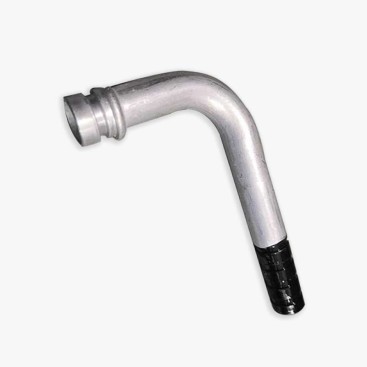
OEM أنابيب العادم الصلب بالألمنيوم
- وصف
وصف
OEM exhaust projects require more than selecting a corrosion-resistant steel. The material, نظام الطلاء, أبعاد, cut ends, welding areas and production consistency all have to work together. For high-temperature exhaust applications, an aluminum-silicon coating is generally the relevant aluminized coating system because its composition is designed for elevated-temperature service, while pure-aluminum Type 2 coating is more commonly associated with lower thermal loads and corrosion or decorative applications.
For an OEM program, the key question is therefore not simply whether the material is aluminized. It is whether the selected coating, substrate and manufacturing specification can remain consistent from prototype through serial production.
The material-selection conclusion
For a high-temperature exhaust application, يكتب 1 Al-Si coating is generally the appropriate aluminized coating system to evaluate. يكتب 1 typically uses an aluminum-silicon alloy coating, بينما اكتب 2 uses essentially pure aluminum. Final selection should still be validated against the actual exhaust temperature profile, بيئة التآكل, forming process, welding process and required service life.
Why Type 1 Is Used for Exhaust Applications
يكتب 1 aluminized coating is an aluminum-silicon alloy coating. The silicon addition is an important part of the coating system used for elevated-temperature steel applications. يكتب 2 is based on essentially pure aluminum and is generally associated with applications where the thermal demand is lower.
| Characteristic | يكتب 1 | يكتب 2 |
|---|---|---|
| Coating composition | Al-Si alloy coating | Essentially pure aluminum coating |
| Typical silicon level | Commonly within an Al-Si coating range, often around 5–11% Si | Very low silicon content compared with Type 1 |
| Thermal application focus | High-temperature applications | Lower thermal-load applications |
| Exhaust suitability | Primary system to evaluate for high-temperature exhaust | Usually not the first choice for high-temperature exhaust service |
| Final selection basis | Must be matched to actual service conditions | Must be matched to actual service conditions |
The important distinction is not that Type 1 is universally better than Type 2. Rather, the coating system has to match the thermal duty of the application. Exhaust components experience repeated heating and cooling, oxidation and potentially corrosive condensate. This makes high-temperature coating performance a central material-selection issue.
How the Al-Si Coating Protects Exhaust Steel
At elevated temperature, the aluminum-containing coating develops a protective oxide layer. This surface layer helps slow further oxidation and provides protection to the underlying steel against high-temperature environmental attack.
This is a mechanism-based explanation, not a guaranteed service-life value. Exhaust durability depends on the actual temperature cycle, gas composition, التكثيف, سمك الجدار, forming history, لحام, thermal cycling and installation environment.
Important: coating selection should not be based on a single maximum-temperature number. An OEM should evaluate the complete thermal cycle, including heating rate, cooling rate, dwell time, peak exposure, condensation and repeated cycling.
OEM Exhaust Is a Consistency Problem as Much as a Material Problem
A prototype can fit perfectly and still fail as an OEM supply program if the dimensional or coating variation between production batches is not controlled. The buyer therefore needs a specification that converts the prototype into measurable production requirements.
For serial production, batch-to-batch consistency can be more important than optimizing the nominal material cost. A small dimensional change can affect fixture fit, welding alignment, assembly force and downstream forming. A coating variation can affect surface appearance, corrosion performance and processing behavior.
The OEM Specification Must Define More Than OD
| مواصفة | What the OEM Should Define | Why It Matters |
|---|---|---|
| Outside diameter | Nominal OD and tolerance | Controls fit, forming and connection dimensions |
| Wall thickness | Nominal thickness and permitted variation | Affects mass, تشكيل, welding and durability |
| طول | Finished length and tolerance | Controls assembly and downstream processing |
| طلاء | يكتب, coating mass and applicable standard | Controls high-temperature protection and batch consistency |
| End condition | Cut, deburred, شكلت, chamfered or other required condition | Affects assembly and welding |
| Welding requirements | Joint type, preparation and coating-removal requirements | Controls weld quality and local corrosion protection |
| Supply form | Coil, straight tube or cut-to-length section | Determines downstream processing requirements |
Batch Consistency: The OEM Requirement That Is Easy to Underestimate
OEM production normally involves repeat orders rather than a single shipment. This changes how a supplier should be evaluated.
A supplier may produce a technically acceptable first batch but still create problems if subsequent batches have different OD, سمك الجدار, coating mass, surface condition or cut-end quality. The result can be assembly variation, tooling adjustment or increased rejection at the customer’s plant.
What OEM buyers should monitor
- Dimensional consistency between production lots
- Coating mass and coating appearance consistency
- Cut-end geometry and burr condition
- Weld quality and tube roundness where applicable
- Traceability from finished tubes to material and coating batches
- Inspection records that can be compared across production lots
Cut Ends and Welding Areas Need Their Own Specification
Cutting exposes the underlying material at the tube end. The coating that protects the surrounding surface is interrupted at the cut. For exhaust components, that exposed area should therefore be considered separately from the intact coated surface.
OEM drawings should state whether the cut end requires deburring, edge treatment, protective coating, end caps or another form of protection. The requirement becomes even more important if components will be stored for an extended period before welding or assembly.
Welding also requires attention to the coating in and around the weld zone. The coating may need to be removed or otherwise managed according to the welding procedure, followed by appropriate treatment of the affected area where corrosion protection is required.
Choosing the Supply Form for an OEM Program
The correct supply form depends on the customer’s manufacturing route. Coil can be suitable when the OEM has its own tube-forming and cutting process. Straight tube can reduce downstream processing when the tube dimensions are already established. Cut-to-length sections can simplify assembly when the required lengths are repetitive.
| Supply Form | Suitable When | OEM Should Confirm |
|---|---|---|
| Coil | Customer performs tube forming and cutting | Coil dimensions, طلاء, forming behavior and surface condition |
| Straight tube | Tube is required before downstream fabrication | ل, سمك الجدار, straightness, length and end condition |
| Cut-to-length tube | Repeated finished lengths simplify assembly | Length tolerance, cutting method, burr control and exposed cut-end treatment |
Aluminized Steel vs Ferritic Stainless Exhaust Materials
Aluminized steel and ferritic stainless steels such as 409 و 439 represent different material approaches to exhaust-system design. The choice involves more than corrosion resistance alone and can include temperature exposure, تشكيل, لحام, سماكة, ركوب الدراجات الحرارية, fabrication requirements and expected service conditions.
Rather than treating one material as universally superior, an OEM should compare the candidate materials against the actual component requirements. The material decision should then be validated through the intended manufacturing process and service environment.
Keep the comparison application-specific
The relevant question is not simply “coated steel or stainless steel?” It is which substrate and surface system provides the required combination of thermal resistance, الحماية من التآكل, القابلية للتشكيل, weldability, dimensional stability and production consistency for this component?
OEM Sampling: Prove the Specification Before Mass Production
An OEM exhaust project should not move directly from a general material enquiry to a large production order. The sample stage should verify both the material and the manufacturing specification.
The first sample should ideally confirm dimensional compliance, متطلبات الطلاء, cut-end condition and the customer’s forming or welding process. If the customer has a formal first-article approval procedure, that requirement should be identified before serial production begins.
| Sampling Stage | Recommended Verification |
|---|---|
| Material review | Base steel grade, coating type and relevant material documentation |
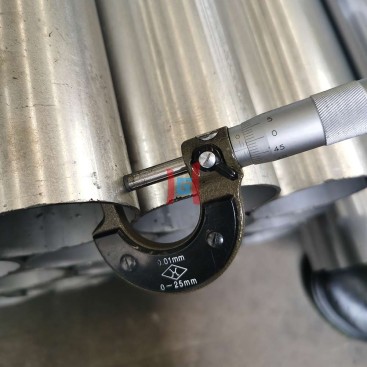
| فحص الأبعاد | ل, سمك الجدار, طول, straightness and other drawing requirements |
| Coating verification | كتلة الطلاء, surface condition and applicable quality records |
| Fabrication trial | تشكيل, قطع, welding and assembly compatibility |
| First-article approval | Customer approval before serial production where required |
OEM Exhaust Material and Specification Checklist
□ Application: identify the exhaust component and actual service environment.
□ Coating: specify Type 1 Al-Si coating where the application requires a high-temperature aluminized system.
□ Base material: define the required steel grade or chemical composition.
□ OD and wall thickness: specify nominal dimensions and tolerances.
□ Length: define straight-tube or cut-to-length dimensions and tolerances.
□ Coating mass: state the required coating quality level and applicable measurement basis.
□ End condition: define cutting, deburring, chamfering and end protection requirements.
□ Welding: define the welding process and requirements for managing the coating in the weld area.
□ Batch consistency: establish dimensional, coating and inspection controls for repeat production.
□ Traceability: require appropriate material and production-batch identification.
□ Sampling: confirm whether samples and first-article approval are required.
□ Supply form: choose coil, straight tube or cut-to-length sections according to the OEM’s manufacturing route.
How Teda Ganghua Supports OEM Exhaust Projects
Teda Ganghua can support OEM procurement with specification-based supply of coated steel tubing, focusing on the dimensions, متطلبات الطلاء, processing condition and documentation needed for repeat production. For an OEM enquiry, providing the drawing or complete specification is more useful than providing only a material name.
For projects requiring أنابيب الصلب بالألمنيوم, Teda Ganghua can work from the customer’s OD, سمك الجدار, طول, متطلبات الطلاء, end condition and application requirements to establish a clearer supply specification. Sample verification can then be used to confirm fit, processing and coating requirements before moving into serial production.
The objective of OEM sourcing is not simply to receive the first batch successfully. It is to establish a repeatable specification that can be manufactured, inspected and delivered consistently across subsequent batches.
The Bottom Line
For high-temperature exhaust applications, يكتب 1 Al-Si coating is the aluminized coating system that should generally be evaluated first. Its purpose is not merely decorative; the aluminum-containing coating can develop a protective oxide layer at elevated temperature and help protect the steel substrate against oxidation and high-temperature corrosion.
For OEM production, لكن, material selection is only the starting point. The drawing should define ل, سمك الجدار, طول, جودة الطلاء, end condition and welding requirements. Production controls should then focus on batch-to-batch dimensional and coating consistency.
The most reliable OEM workflow is specification → sample → inspection → first-article approval → serial production. Establishing this process before mass production helps prevent the common OEM problem of one batch fitting correctly while the next batch requires adjustment.
الأسئلة المتداولة
لماذا النوع 1 coating generally selected for exhaust applications?
يكتب 1 uses an aluminum-silicon alloy coating designed for elevated-temperature applications. Exhaust components experience repeated heating and cooling and can face oxidation and corrosive environments, making this coating system more relevant than a lower-thermal-load Type 2 system.
Does Type 1 guarantee a specific exhaust service life?
لا. Coating performance depends on the actual temperature cycle, atmosphere, التكثيف, component design, fabrication and other service conditions. A service-life claim should be supported by application-specific testing rather than coating type alone.
What should an OEM drawing specify for coated exhaust tube?
The drawing should define the outside diameter, سمك الجدار, طول, التحمل الأبعاد, coating type and quality level, end condition, welding requirements and any special processing requirements. These details turn a general material request into a repeatable production specification.
Should an OEM buyer request samples before placing a production order?
نعم. A sample can verify dimensions, جودة الطلاء, قطع, تشكيل, welding and assembly compatibility. If the customer’s quality system requires first-article approval, this should be completed before serial production.
Is aluminized steel always preferable to ferritic stainless steel for exhaust systems?
Not universally. الصلب بالألمنيوم ودرجات الفولاذ المقاوم للصدأ مثل 409 و 439 لها خصائص مادية مختلفة ويجب مقارنتها بالتعرض الحراري للمكون, بيئة التآكل, تشكيل, اللحام وأداء الخدمة المطلوبة.