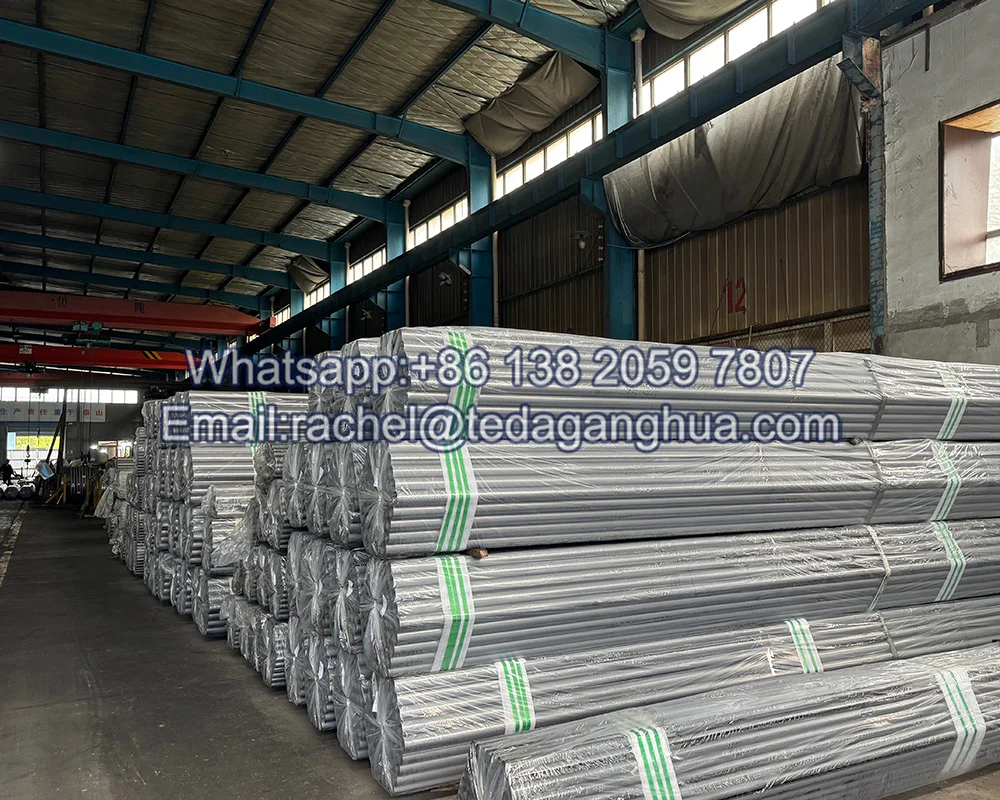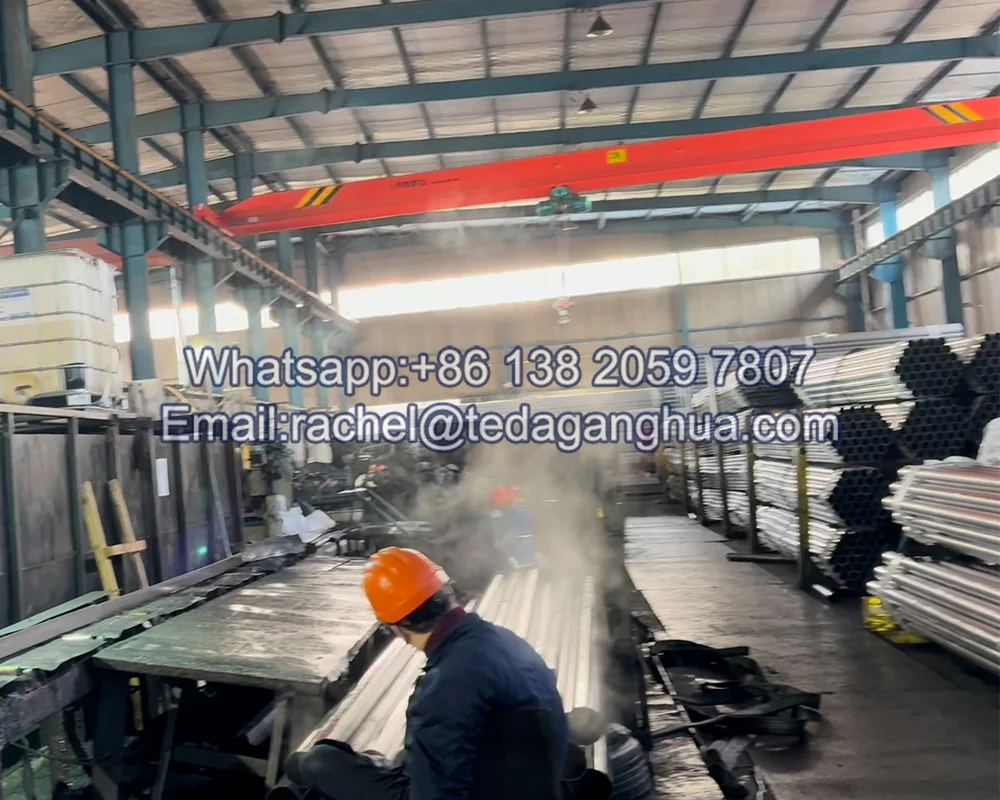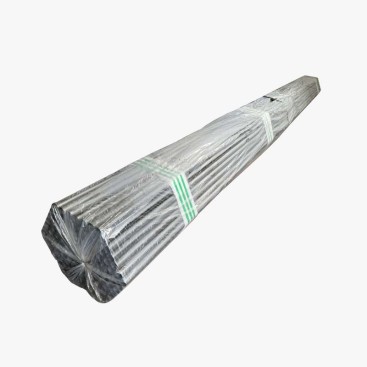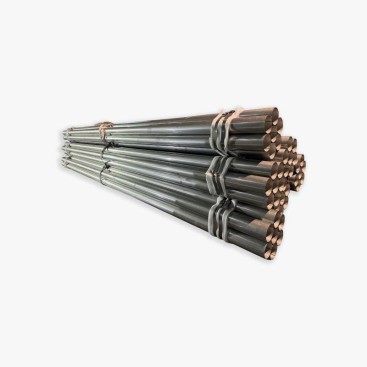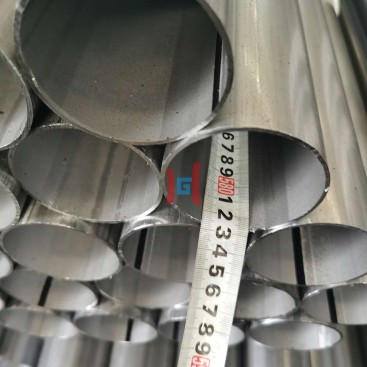
Feueraluminiertes Stahlrohr
- Beschreibung
Beschreibung
Hot-dip aluminized steel is not simply carbon steel dipped into molten aluminum. It is an engineered coated steel product in which a carbon steel substrate is covered with an aluminum-based alloy coating. In the aluminum-silicon coating process, silicon plays an important role in controlling the reaction between molten aluminum and iron, influencing the intermetallic layer, Beschichtungsstruktur, and high-temperature performance. Understanding what happens inside the molten bath helps buyers distinguish genuine hot-dip aluminized materials from other aluminum-coated steel products.
1. What Is Hot-Dip Aluminizing?
Hot-dip aluminizing is a surface coating process in which prepared steel is brought into contact with molten aluminum or an aluminum-based alloy. During immersion, a metallurgical reaction takes place between the iron in the steel substrate and the aluminum in the bath. This reaction creates an intermediate iron-aluminum alloy layer, while the remaining aluminum-rich material forms the outer coating.
For aluminum-silicon coated steel, the product consists of two main components:
Carbon Steel Substrate
The base material provides structural strength, mechanical properties, and the required load-bearing performance.
Aluminum-Silicon Alloy Coating
The surface coating provides corrosion and oxidation protection, while the metallurgical interface helps establish a durable connection with the steel substrate.
daher, aluminized steel should not be described simply as aluminum-covered steel without considering the alloy composition and interfacial reaction. The coating is an integrated metallurgical system rather than a separate layer attached only by mechanical contact.
2. Why Is Silicon Added to the Aluminum Bath?
Silicon is not an accidental impurity in aluminum-silicon coating production. It is an intentional alloying element that influences the interaction between molten aluminum and the steel surface. Its most important metallurgical function is to control the growth and morphology of the iron-aluminum intermetallic layer.
When steel contacts pure molten aluminum, iron and aluminum react to form intermetallic compounds. Excessive growth of these compounds can produce a relatively thick and brittle interface, which may negatively affect coating formability and resistance to mechanical deformation. Adding silicon helps regulate this reaction.
| Function of Silicon | Metallurgical Effect | Practical Significance |
|---|---|---|
| Controls intermetallic growth | Regulates the formation and thickness of Fe-Al reaction layers | Helps improve coating integrity and formability |
| Modifies interface structure | Influences the morphology and composition of the metallurgical interface | Supports a more controlled coating-substrate connection |
| Contributes to oxidation resistance | Influences the coating’s high-temperature oxidation behavior | Supports protective oxide formation during elevated-temperature service |
| Influences bath chemistry | Changes the reaction behavior of the molten aluminum alloy | Helps control coating formation during production |
One important distinction is that silicon does not simply make the molten aluminum flow more easily under every production condition. Its primary metallurgical significance in this coating system is controlling iron-aluminum intermetallic formation. Coating uniformity and final surface quality also depend on bath temperature, immersion conditions, steel surface preparation, withdrawal speed, and coating control equipment.
This is why the aluminum-silicon bath must be treated as a carefully controlled alloy system rather than ordinary molten aluminum.
3. What Happens Inside the Hot-Dip Bath?
The production process involves several coordinated stages. Each stage affects the final coating structure, Haftung, and surface condition.
Schritt 1. Steel Surface Preparation
The steel surface is cleaned to remove oil, Rost, Skala, and other contaminants that may interfere with wetting and metallurgical bonding.
Schritt 2. Entry into the Molten Bath
The prepared steel enters a controlled molten aluminum or aluminum-silicon alloy bath. The liquid metal contacts the steel surface and initiates an interfacial reaction.
Schritt 3. Formation of the Intermetallic Layer
Iron from the steel reacts with aluminum to form iron-aluminum-based intermetallic compounds. Silicon modifies the growth behavior and microstructure of this reaction layer.
Schritt 4. Withdrawal and Coating Control
The steel is withdrawn from the bath. Excess molten alloy is controlled through production equipment and process parameters to achieve the specified coating characteristics.
Schritt 5. Cooling and Inspection
The coated material is cooled and inspected for surface condition, coating consistency, Haftung, and compliance with the agreed technical requirements.
In continuous production, steel strip passes through the coating line and molten bath using controlled transport equipment. Tubular products may be manufactured through different production routes, including forming and welding coated strip or applying a coating to an already manufactured tube. These routes are not interchangeable, so the manufacturing method should be confirmed when specifying the product.
4. Hot-Dip Aluminizing vs. Other Aluminum Coating Methods
Not every steel product described as aluminum-coated is manufactured using the same technology. The coating method determines how the aluminum is deposited, how the interface develops, and what performance characteristics can be expected.
| Coating Method | Prozessprinzip | Main Characteristics |
|---|---|---|
| Hot-Dip Coating | Steel contacts a molten aluminum-based bath | Forms a metallurgical interface and an aluminum-rich surface coating |
| Electroplating | Metal is deposited through an electrochemical process | Conventional aqueous aluminum electroplating is difficult because of water reduction; specialized non-aqueous processes are possible |
| Thermal Spraying | Molten or semi-molten aluminum particles are deposited onto steel | Creates a sprayed coating without the same bath-driven diffusion mechanism |
| Diffusion Aluminizing | Aluminum diffuses into the steel surface during a controlled thermal treatment | Produces an aluminide diffusion layer with a different structure from conventional hot-dip coatings |
Hot-dip processing is an established industrial method for producing aluminum-coated steel. Jedoch, it should not be assumed that every aluminized tube is produced through a continuous strip coating line. Individual components and finished tubular products can involve different coating arrangements.
The term hot-dip therefore provides important information about the manufacturing process. It should be retained in technical descriptions whenever the actual coating route is relevant.
5. Aluminum Coating Types and Relevant Standards
The terms aluminum-coated steel and aluminum-silicon coated steel are related but should not automatically be treated as identical. Different standards distinguish coating compositions and product forms.
ASTM A463/A463M covers steel sheet coated with aluminum by the hot-dip process. It distinguishes two aluminum coating types, including an aluminum-silicon alloy coating and a commercially pure aluminum coating.
IN 10346 addresses continuously hot-dip coated steel flat products. Its AS designation identifies an aluminum-silicon alloy coating, while A identifies an aluminum coating. These designations are useful when specifying the coating chemistry and delivery requirements for flat steel products.
| Standard | Product Coverage | Relevant Coating Classification |
|---|---|---|
| ASTM A463/A463M | Hot-dip aluminum-coated steel sheet | Typ 1: Aluminium-Silizium-Legierung; Typ 2: commercially pure aluminum |
| IN 10346 | Continuously hot-dip coated steel strip and sheet | ALS: Aluminium-Silizium-Legierung; A: Aluminiumbeschichtung |
An important purchasing consideration is that these standards primarily address steel sheet or flat products, rather than establishing a universal specification for every finished steel tube. For tubular products, buyers should confirm the applicable product standard, Grundstahlsorte, coating composition, manufacturing route, and inspection requirements separately.
Beschichtungsmasse, coating thickness, and adhesion requirements should follow the applicable standard and the agreed purchase order. There is no single coating specification that applies to every aluminized steel tube.
6. What Determines the Quality of Aluminized Steel Tubes?
The quality of an aluminum-coated tube depends on more than the aluminum content of the bath. Buyers should evaluate the complete relationship between the steel substrate, coating chemistry, production conditions, and final inspection.
Grundmaterial
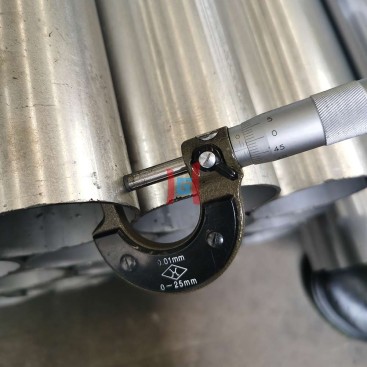
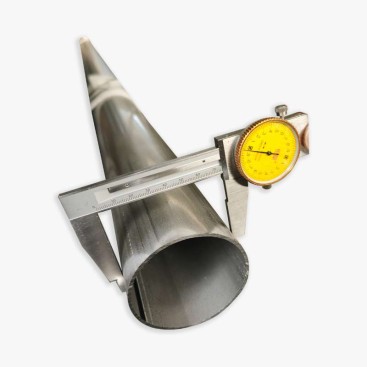
Check the carbon steel grade, mechanical properties, chemical composition, and dimensional tolerances.
Beschichtungszusammensetzung
Confirm whether the required coating is aluminum-silicon alloy or commercially pure aluminum. Do not rely on the general term aluminum-coated alone.
Beschichtungshaftung
The interface must withstand the forming, Biegen, handling, and service conditions specified for the application.
Surface Uniformity
Inspect for bare areas, excessive buildup, surface defects, and other inconsistencies that may affect service performance.
Manufacturing Route
Determine whether the tube was formed from coated strip or coated after tube fabrication. This affects the condition of the weld seam, cut ends, and finished surface.
7. Applications of Aluminum-Silicon Coated Steel
Aluminum-based coatings are selected when steel components require a combination of structural strength, surface protection, and resistance to elevated-temperature oxidation. Aluminum-silicon coated steel is particularly relevant to applications involving thermal exposure and demanding operating environments.
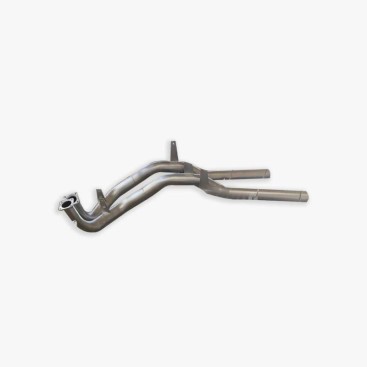
- Abgassysteme für Kraftfahrzeuge: Tubular components and related parts exposed to elevated temperatures and oxidation.
- Industrial heating equipment: Components used in furnaces, heating assemblies, and thermal processing equipment.
- Heat-resistant enclosures: Steel structures and protective components operating under elevated-temperature conditions.
- Industrial ducting: Selected air-handling and exhaust components where coating performance meets the operating environment.
- Thermal equipment fabrication: Fabricated steel parts requiring controlled surface protection and mechanical strength.
Material selection must consider actual operating temperature, Temperaturwechsel, atmosphere, Feuchtigkeit, chemical exposure, and mechanical loading. Aluminum-based coatings are not universally resistant to every corrosive medium or temperature condition. Application-specific evaluation remains essential.
8. Sourcing Hot-Dip Aluminized Steel Tubes from Teda Ganghua
Selecting the correct coated steel product requires more than matching a product name. Buyers should communicate the base material, Rohrabmessungen, coating type, production method, and required inspection documents before confirming an order.
Teda Ganghua Metal is a steel stockist based in Tianjin TEDA, mit 20 years of steel stockist experience and export experience. The company supports international buyers with material sourcing, dimensional requirements, processing coordination, and quality documentation.
For buyers sourcing hot-dip aluminized steel tubes, Teda Ganghua can help coordinate product specifications and purchasing requirements, einschließlich:
- Confirmation of carbon steel substrate grade and tube dimensions.
- Clarification of aluminum-silicon or other specified coating requirements.
- Coordination of cutting, Schweißen, Biegen, and other fabrication requirements where applicable.
- Material Test Certificates (MTC) and relevant quality inspection documentation.
- Third-party inspection arrangements and shipment verification.
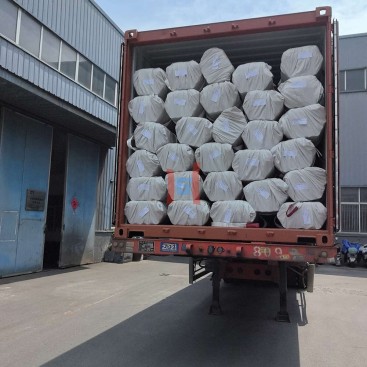
- Export packing and delivery coordination for international projects.
Teda Ganghua emphasizes material traceability, specification confirmation, and shipment quality control. Buyers are welcome to arrange inspections before shipment to verify material grades, Abmessungen, quantities, and agreed quality requirements.
When requesting a quotation or technical confirmation, providing the intended application, tube size, Stahlsorte, coating designation, manufacturing route, and applicable standard will help establish a more accurate product specification.
Häufig gestellte Fragen
1. Is aluminized steel made entirely of aluminum?
NEIN. It consists of a carbon steel substrate with an aluminum-based surface coating. In aluminum-silicon coated products, the coating contains aluminum and silicon, together with an interfacial reaction layer formed during the coating process.
2. Why is silicon added during hot-dip aluminizing?
Silicon helps control the formation and growth of iron-aluminum intermetallic compounds at the steel-coating interface. This influences coating structure, adhesion behavior, und Formbarkeit. It also contributes to the oxidation behavior of the coating system.
3. What is the difference between aluminum-coated and aluminum-silicon coated steel?
Aluminum-coated steel is a broad description. Aluminum-silicon coated steel specifically uses an aluminum-silicon alloy coating. Standards such as ASTM A463/A463M distinguish different aluminum coating types, while EN 10346 identifies aluminum-silicon coating with the AS designation.
4. Is hot-dip aluminizing the same as aluminum spraying?
NEIN. Hot-dip aluminizing involves contact between steel and a molten aluminum-based bath, creating a metallurgical reaction layer. Thermal spraying deposits aluminum particles onto a prepared surface through a different process and produces a different coating structure.
5. What information is required when purchasing aluminized steel tubes?
Käufer sollten die Stahlsorte angeben, Außendurchmesser, Wandstärke, Rohrlänge, coating type, manufacturing route, geltenden Norm, Maßtoleranzen, und Inspektionsanforderungen. Die erforderliche Beschichtungsmasse und -dicke sollte gemäß der geltenden Spezifikation und Bestellung vereinbart werden.