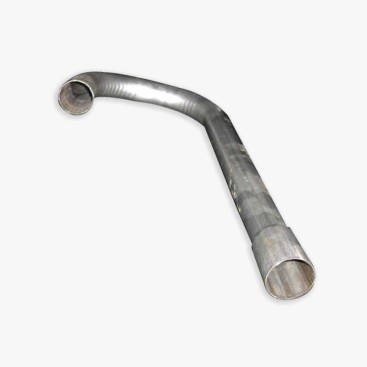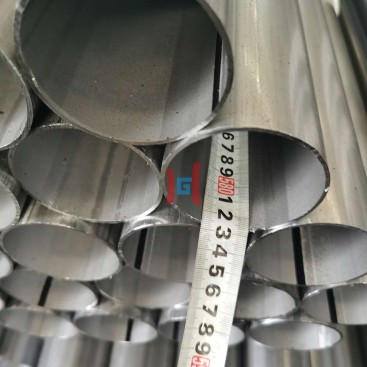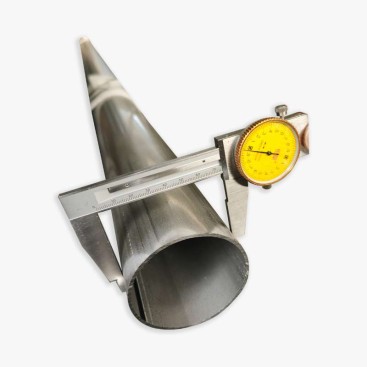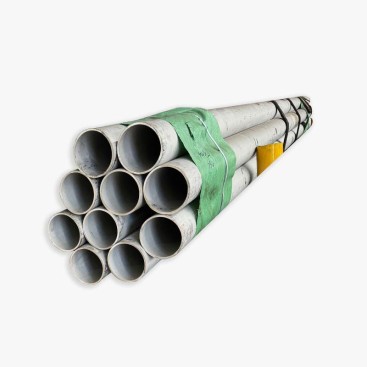
Tuyau en acier aluminisé Sa1d As120
- Description
Description
When specifying SA1D AS120 aluminized steel pipe, two separate material characteristics need to be evaluated: the formability of the steel substrate and the protective capacity of the aluminum-based coating. SA1D identifies a deep-drawing substrate designation associated with JIS G3314 terminology, while AS120 describes a coating mass designation used in the EN coating system. Understanding these two components helps procurement managers and engineers select tubular materials for demanding forming operations, elevated-temperature service, et protection contre la corrosion à long terme.
1. Understanding SA1D and AS120 as Separate Specifications
The designation combines a substrate grade with a coating specification. Although this shorthand is used in commercial discussions, the two parts belong to different standards frameworks. Confirming the applicable product standard, substrate condition, exigences en matière de revêtement, and tubular dimensions is essential before placing an order.
| Designation | Meaning | Procurement consideration |
|---|---|---|
| SA1D | A deep-drawing substrate designation associated with JIS G3314 terminology. | Verify the governing standard, mechanical properties, and forming requirements. |
| AS120 | An aluminum-silicon coating designation associated with the EN coating system. | Confirm the applicable coating standard and whether the specified mass is a two-sided total. |
| Combined designation | A description combining substrate formability and coating protection. | State the complete standard references and tubular manufacturing requirements. |
JIS G3314 covers hot-dip aluminum-coated steel sheets and strips, whereas EN 10346 establishes requirements for continuously hot-dip coated flat steel products. Combining their terminology can communicate the intended material characteristics, but it does not automatically establish that a finished pipe complies with both standards. The tube manufacturing route, méthode de soudage, dimensions, and final inspection requirements should also be specified.
2. What Does AS120 Mean in Coating Mass?
In the relevant EN coating designation context, AS identifies an aluminum-silicon coating system, et 120 refers to a nominal coating mass of 120 g/m² for both coated sides combined. Assuming an approximately equal coating distribution, this corresponds to about 60 g/m² par face. The actual distribution may vary, so the required coating condition should be confirmed against the applicable product specification.
Coating mass comparison
AS120: environ 120 g/m² combined, ou 60 g/m² per side when evenly distributed.
AS80: environ 80 g/m² combined, ou 40 g/m² per side when evenly distributed.
The nominal combined coating mass of AS120 is 50% greater than that of AS80. This does not mean that service life or oxidation resistance will increase by the same percentage.
| Parameter | AS80 | AS120 |
|---|---|---|
| Nominal combined coating mass | 80 g/m² | 120 g/m² |
| Approximate mass per side, assuming equal distribution | 40 g/m² | 60 g/m² |
| Relative combined coating mass | Reference level | 50% higher |
| Primary selection consideration | Coating requirements with lower nominal mass | Greater coating mass for applications requiring additional protection |
A higher coating mass can provide a larger protective material reserve under suitable service conditions. Cependant, actual corrosion performance depends on temperature, atmosphere, humidité, chemical exposure, continuité du revêtement, and damage introduced during fabrication. Coating mass alone cannot determine the expected service life.
3. Why Combine Deep-Drawing Steel with a Heavier Coating?
The combination addresses two different engineering requirements. A deep-drawing substrate is intended for demanding forming operations, while a heavier aluminum-silicon coating can provide additional protection against oxidation and environmental attack when the service conditions are compatible with the coating system.
Formability of the SA1D Substrate
Deep-drawing applications require the steel substrate to deform without unacceptable tearing, rides, or dimensional distortion. The suitability of the material depends on verified mechanical properties, thickness consistency, forming geometry, lubrication, tooling clearance, and process control. A grade designation alone does not guarantee that every component geometry can be formed successfully.
Protective Reserve of the AS120 Coating
A greater coating mass can offer additional protective reserve compared with a lighter coating of the same system. Aluminum-silicon coatings are used where oxidation resistance and protection of the underlying steel are important. Nevertheless, the coating should be qualified for the actual operating temperature and atmosphere rather than selected solely because its nominal mass is higher.
When both requirements are critical, the material selection combines enhanced forming potential with a relatively high coating mass. The final result still depends on whether the substrate specification, système de revêtement, and finished tubular product are compatible with the intended manufacturing route.
4. Applications and Operating Conditions
This material concept may be considered for components that require both complex forming and protective performance. Suitability must be verified for each application, particularly where elevated temperatures, cyclic heating, welded joints, or prolonged outdoor exposure are involved.
Automotive Exhaust Components
Potentially suitable for selected exhaust-system components where forming capability and oxidation resistance are required. Confirm peak metal temperature, cyclage thermique, exposition aux condensats, and weld integrity.
Industrial Furnaces and Heating Equipment
May be evaluated for formed ducts, housings, and other components exposed to heat. Suitability depends on continuous and peak temperatures, atmosphere chemistry, and the required oxidation life.
Outdoor Tubular Components
Can be considered for exposed components where the coating remains compatible with the environment. Assess rainwater retention, salt exposure, cut edges, fasteners, and local coating damage.
Unpainted Fabricated Parts
A coated surface may reduce the need for an additional paint layer in qualified applications. Confirm appearance, état de surface, forming damage, and corrosion requirements before omitting further finishing.
For high-temperature service, the design should distinguish oxidation resistance from general corrosion resistance. A coating that performs well in a controlled heated atmosphere may behave differently under condensation, chloride contamination, aggressive combustion gases, or repeated heating and cooling.
5. Formation, Flexion, and Welding Recommendations
Deep Drawing and Bending
Although the substrate is intended for demanding forming operations, the coating introduces an additional surface-integrity consideration. Excessive deformation, sharp corners, unsuitable tooling, or poor lubrication can cause coating cracking, flaking, or local separation. These defects may expose the steel substrate and reduce the intended protective performance.
- Use suitable die radii and avoid unnecessarily sharp transitions in heavily deformed areas.
- Evaluate forming limits through trials using the actual material thickness, outillage, and lubrication conditions.
- Inspect highly strained regions for coating cracks, flaking, and exposed substrate.
- Where tight-radius forming is required, confirm coating flexibility and adhesion before production.
Welding and Joint Protection
Welding locally heats or removes the coating and may generate fumes from the coating constituents. Welding procedures should be selected according to the substrate, joint design, épaisseur de paroi, and applicable safety requirements. Appropriate ventilation, exposure controls, and protective equipment are essential when working with coated steel.
- Use a qualified welding procedure and control heat input to limit unnecessary thermal damage.
- Prepare the joint as required by the approved procedure, including coating removal where necessary.
- Inspect the weld and heat-affected area for defects and coating damage.
- Apply a compatible post-weld protective treatment where the service environment requires it.
For welded pipe, the original flat-strip coating specification does not by itself guarantee equivalent protection at the weld seam, cut ends, or heat-affected areas. These locations should be addressed separately in the product specification and quality inspection plan.
6. Ordering Checklist for Aluminized Steel Pipe
Because the combined designation spans different standards terminology, procurement managers should provide a complete technical specification rather than relying on a short material label.
- Substrat: Specify the required grade, governing standard, mechanical properties, and forming requirements.
- Revêtement: Identify the coating system, nominal coating mass, base de mesure, and acceptable distribution between surfaces.
- Pipe dimensions: State outside diameter, épaisseur de paroi, longueur, tolérances dimensionnelles, and permitted ovality.
- Manufacturing method: Specify the forming and tube-making route, weld type where applicable, and seam-protection requirements.
- Service conditions: Define continuous and peak temperatures, operating atmosphere, humidité, chemical exposure, and expected service life.
- Quality documents: Request material test certificates, coating inspection results, dimensional reports, and traceability information as applicable.
- Fabrication requirements: Identify drawing geometry, bending radii, welding procedures, surface acceptance criteria, and post-fabrication protection.
Buyers should also clarify whether the supplier is offering coated strip subsequently formed into pipe or a finished tubular product manufactured and inspected to a specific tube standard. This distinction affects dimensional tolerances, qualité de soudure, continuité du revêtement, and acceptance criteria.
7. Sourcing Support from Teda Ganghua
Teda Ganghua supports industrial buyers with material selection and sourcing discussions for coated steel products and tubular applications. When evaluating a deep-drawing substrate with a heavier aluminum-silicon coating, procurement teams should confirm the exact substrate standard, coating designation, dimensions des tubes, fabrication route, and service environment before requesting a quotation.
For project-specific requirements, buyers can explore tubes en acier aluminisé and provide the required outside diameter, épaisseur de paroi, longueur, spécification du revêtement, température de fonctionnement, et l'application prévue. This information helps the supply team assess specification compatibility, documentation needs, and whether additional processing or inspection is necessary.
A well-defined inquiry should distinguish the desired material properties from the finished product acceptance criteria. This approach reduces ambiguity between substrate designation, coating mass, and tubular product standards while supporting more reliable purchasing decisions.
Foire aux questions
1. What do SA1D and AS120 mean?
SA1D identifies a deep-drawing substrate designation associated with JIS G3314 terminology, while AS120 describes an aluminum-silicon coating designation associated with the EN system. They describe different material characteristics and should be verified against the applicable standards.
2. Does AS120 mean 120 g/m² on each side?
Non. In the relevant EN designation context, 120 g/m² refers to the nominal combined coating mass on both sides. An even distribution would correspond to approximately 60 g/m² par face, although the actual distribution must be checked against the specification.
3. Is AS120 always better than AS80?
Pas dans toutes les applications. The higher nominal coating mass provides additional protective reserve under suitable conditions, mais cela peut augmenter la consommation de matière et compliquer le formage ou le soudage. La qualité appropriée dépend des conditions de fonctionnement, exigences de fabrication, et durée de vie requise.
4. Ce matériau peut-il être utilisé pour les tuyaux d'échappement à haute température?
Il peut convenir à certains composants, mais l'adéquation ne peut pas être déterminée à partir de la seule désignation. Température maximale du métal, cyclage thermique, atmosphere, intégrité de la soudure, et la dégradation du revêtement doit être évaluée par rapport aux conditions réelles de fonctionnement du système d'échappement..
5. Quelles informations les acheteurs doivent-ils fournir lors d'une demande de devis?
Fournir les spécifications complètes du substrat et du revêtement, normes régissant, diamètre du tuyau, épaisseur de paroi, longueur, méthode de fabrication, conditions de service, exigences d'inspection, et les certificats requis. Des informations détaillées aident les fournisseurs à évaluer la faisabilité et à clarifier toute différence entre les normes de revêtement des aciers plats et les exigences relatives aux tubes finis..