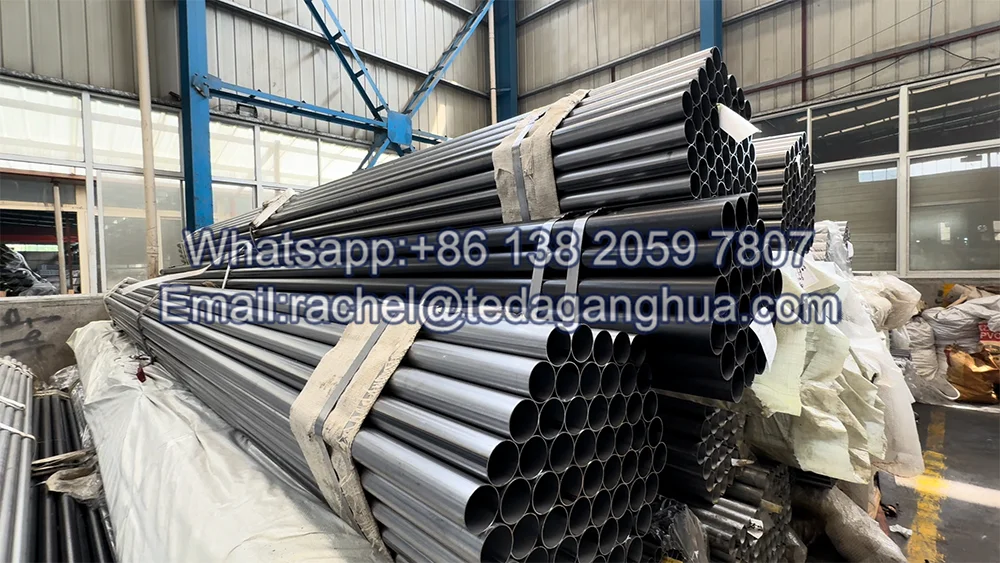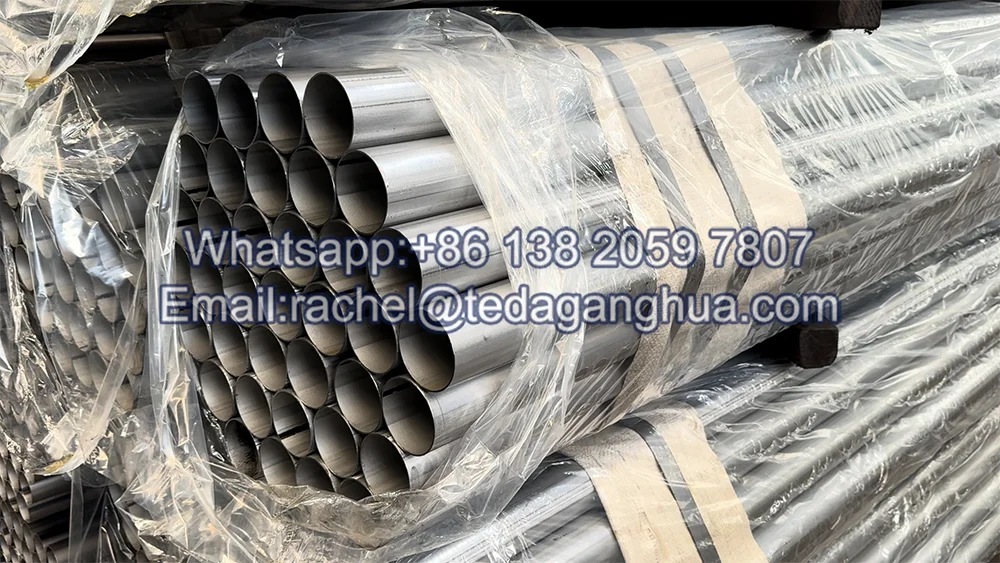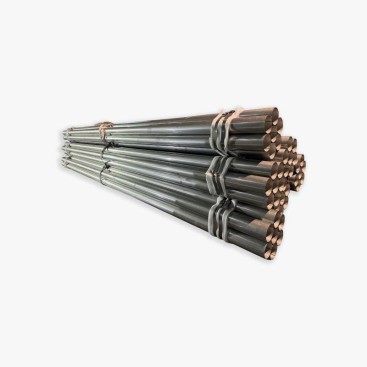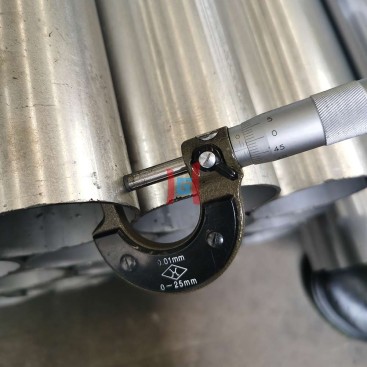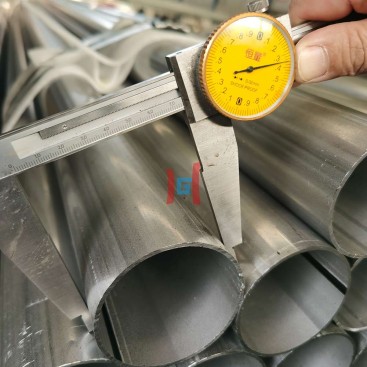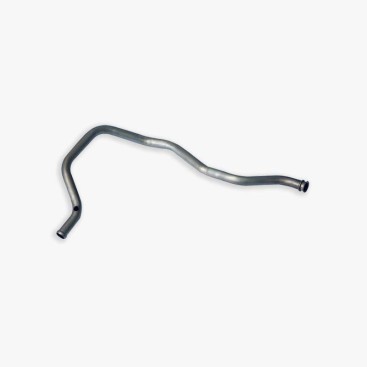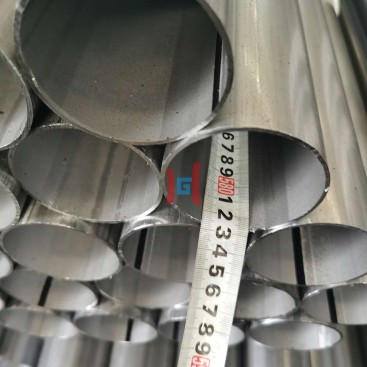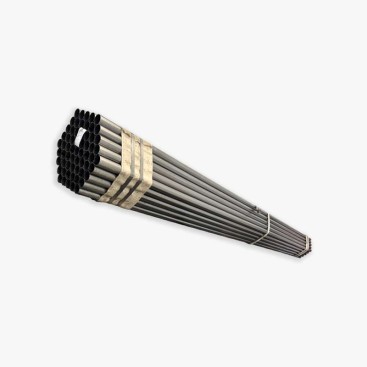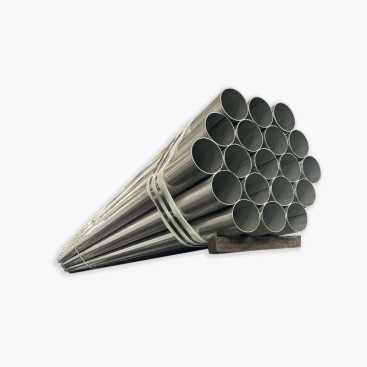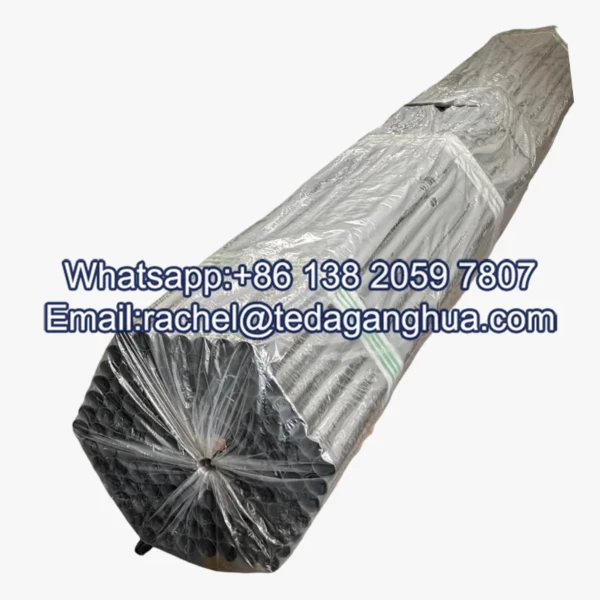
Tubo in acciaio alluminato Sa1d As80
- Descrizione
Descrizione
SA1D AS80 aluminized steel tube is a practical material combination for applications that require good forming capability without specifying a heavier coating than necessary. The designation brings together two distinct characteristics: SA1D identifies a deep-drawing substrate designation associated with JIS G3314 terminology, while AS80 refers to an aluminum-silicon coating designation associated with the EN coating system. For many formed exhaust components and heat-resistant fabricated parts, this combination can provide a useful balance between substrate formability, coating protection, e requisiti di produzione.
1. What SA1D AS80 Means
The designation should be interpreted in two parts rather than as a single grade. The substrate designation describes the intended forming characteristics, while the coating designation identifies the nominal coating mass under the applicable coating specification.
| Specification element | Meaning | What buyers should verify |
|---|---|---|
| SA1D | Deep-drawing substrate designation associated with JIS G3314 terminology. | Applicable standard, mechanical properties, spessore, and forming performance. |
| AS80 | Aluminum-silicon coating designation associated with the EN coating system. | Coating mass basis, continuità del rivestimento, and applicable inspection requirements. |
| Finished tube | A tubular product manufactured from coated steel or produced through another specified coating route. | Dimensioni del tubo, metodo di produzione, weld-zone protection, and final acceptance criteria. |
JIS G3314 addresses hot-dip aluminum-coated steel sheets and strips, while EN 10346 riguarda i prodotti piatti di acciaio rivestiti a caldo in continuo. Because the designation combines terminology from different standards systems, buyers should state the complete material requirements when ordering finished tubes. The shorthand communicates the intended material combination but does not, by itself, establish compliance of the finished tube with both standards.
2. Why AS80 Is a Common Practical Choice
The main advantage of AS80 is its balance of coating protection, forming behavior, and material utilization. A coating mass of approximately 80 g/m² across both sides is equivalent to about 40 g/m² per side when distributed evenly. This provides a defined coating level without automatically moving to the higher coating mass associated with AS120.
AS80 coating specification at a glance
Nominal combined coating mass: 80 g/m².
Approximate coating mass per side: 40 g/m², assuming equal distribution.
Primary selection objective: balance protective performance and fabrication requirements.
Actual service life depends on temperature, atmosphere, coating integrity, danno di fabbricazione, and operating conditions. It should be established through application-specific evaluation rather than a fixed lifetime assumption.
A Balanced Coating Level
For applications where the required protective performance can be achieved without a heavier coating, AS80 can be a rational starting point. Increasing coating mass may provide additional protective reserve, but the improvement in service performance is not necessarily proportional to the increase in coating mass. The economic benefit of a heavier coating therefore depends on the actual exposure conditions and required service life.
Forming-Friendly Fabrication
Compared with a heavier coating of the same system, a lighter coating may reduce the amount of coating material subjected to severe deformation and can be advantageous in some forming operations. Tuttavia, coating cracking is also affected by adhesion, coating microstructure, substrate condition, die geometry, lubrication, and deformation severity. AS80 should not be assumed to eliminate cracking during deep drawing or tight-radius bending.
A Sensible Starting Point for Material Selection
AS80 is often worth evaluating when the application needs reliable heat and oxidation protection but does not require the additional coating mass of a higher specification. It is not a universal default for every exhaust or industrial heating component. Qualification should reflect the actual temperature profile, corrosive exposure, component geometry, and expected operating conditions.
3. SA1D AS80 vs. SA1C AS80: Which Substrate Should You Choose?
The distinction between SA1D and SA1C is primarily related to the required forming capability, not a simple ranking of overall material quality. When the coating specification remains the same, the substrate should be selected according to the geometry and deformation demands of the component.
| Comparison factor | SA1D + AS80 | SA1C + AS80 |
|---|---|---|
| Substrate designation | Deep-drawing grade | Commercial-grade designation |
| Forming priority | More demanding drawing and complex forming, subject to verified properties | Less demanding forming operations within the material’s qualified limits |
| Potential applications | Deep-drawn shells, complex profiles, and formed components | Simple bending, roll forming, and suitable tube-making operations |
| Coating designation | AS80 | AS80 |
| Selection principle | Choose when the forming requirements justify a deep-drawing substrate. | Choose when the specified commercial-grade properties satisfy the component design. |
Both combinations use the same nominal coating designation, so the principal decision concerns the substrate’s verified forming properties. SA1D is the more appropriate starting point for demanding drawing operations, whereas SA1C may be sufficient for simpler fabrication. Neither designation should be treated as a blanket guarantee of finished-component quality; the actual standard, material test results, and forming trials remain important.
4. Typical Applications of Deep-Drawing Aluminized Steel
A deep-drawing substrate combined with a moderate aluminum-silicon coating mass may be considered for components requiring both complex shaping and protection against heat or environmental exposure.
Exhaust Manifolds and Front Pipes
Evaluate for suitable formed exhaust components where temperature resistance, coating integrity, and complex geometry are important. Confirm peak metal temperature and thermal cycling before selection.
Muffler Internal Components
Potentially suitable for selected internal parts exposed to heat and exhaust gases. Assess condensate, corrosive deposits, local temperature, and the durability of welded joints.
Heat-Resistant Appliance Parts
Consider for appropriately qualified housings, condotti, and formed parts in heating appliances. The coating and substrate must meet the actual temperature and atmosphere requirements.
These are potential application categories, not universal approvals. For exhaust systems in particular, temperature can vary considerably between locations. The material suitable for a downstream pipe or muffler component may not be appropriate for a manifold or another area exposed to more severe thermal cycling.
5. Tube Manufacturing, Piegatura, and Welding Considerations
Control the Bending Radius
A bending radius that is too small can create excessive local strain and increase the risk of coating cracks, flaking, or exposure of the underlying steel. The minimum practical radius depends on wall thickness, diametro del tubo, utensileria, forming direction, and material condition.
- Avoid unnecessarily tight bends and abrupt transitions in highly strained areas.
- Confirm the minimum bend radius through engineering assessment or forming trials.
- Inspect the outside of the bend for cracking and the inside for wrinkling or distortion.
- Check coating continuity after forming, especially where the component will operate in a corrosive environment.
Manage Coating Damage at the Weld Seam
During tube manufacturing, welding can locally damage or remove the coating because of concentrated heat. The original coating designation does not guarantee that the weld seam will retain the same protective condition as the surrounding surface.
- Select a welding process and heat input appropriate for the substrate, spessore della parete, and joint design.
- Establish suitable seam preparation and coating-removal procedures where required.
- Inspect the weld for defects and examine the adjacent coating for thermal damage.
- Determine whether the seam requires a compatible protective treatment based on the final operating environment.
- Use appropriate ventilation and exposure controls to manage fumes generated when welding coated steel.
These precautions are particularly important for exhaust tubing and other components that combine repeated thermal cycles with vibration. The tube specification should address weld quality, precisione dimensionale, continuità del rivestimento, and final inspection rather than relying exclusively on the incoming strip designation.
6. How to Specify SA1D AS80 for Procurement
Procurement managers can reduce specification ambiguity by documenting the material and finished-product requirements separately. This is especially important when the substrate and coating descriptions refer to different standards systems.
Recommended inquiry checklist
- Substrate grade and complete governing standard.
- Coating system, nominal mass, base di misurazione, and coating distribution requirements.
- Tube outside diameter, spessore della parete, lunghezza, and dimensional tolerances.
- Tube-making method, requisiti di saldatura, and seam-protection expectations.
- Required forming operations, including deep drawing, flessione, or roll forming.
- Continuous and peak operating temperatures, atmosphere, umidità, and chemical exposure.
- Material test certificates, rapporti di ispezione, tracciabilità, and acceptance criteria.
- Requirements for post-weld treatment, ispezione superficiale, confezione, and delivery.
Buyers should also clarify whether the supplier manufactures finished tubes from coated strip or supplies a different tube product with a separately controlled coating process. This information helps establish which standards apply to the substrate, rivestimento, weld seam, and finished dimensions.
7. Sourcing Aluminized Steel Tubes from Teda Ganghua
Teda Ganghua supports industrial sourcing inquiries for coated steel products and tubular applications. For projects considering a deep-drawing substrate with an AS80 coating, buyers should provide the intended component geometry, dimensioni del tubo, requisiti di formazione, temperatura operativa, and applicable material standards so that specification compatibility can be assessed.
Explore tubi in acciaio alluminato and submit your project requirements for review. A detailed inquiry helps clarify the coating mass basis, substrate properties, tube manufacturing route, weld protection, and documentation needed for the intended application.
The objective is to select a material specification that meets the component’s actual performance requirements without adding coating mass or forming capability that the design does not need. The final selection should be supported by applicable standards, supplier documentation, and application-specific validation.
Domande frequenti
1. What does AS80 mean for aluminized steel tube?
In the relevant EN coating designation context, AS80 refers to a nominal combined aluminum-silicon coating mass of 80 g/m² across both sides. If evenly distributed, this corresponds to approximately 40 g/m² per lato. The applicable specification should be checked to confirm the coating requirements.
2. Why choose SA1D AS80 instead of SA1D AS120?
AS80 may be preferable when its coating protection is sufficient for the operating environment. It offers a lower nominal coating mass than AS120 and may be advantageous in some forming operations. The correct choice depends on required durability, temperatura, coating integrity, fabrication conditions, and lifecycle requirements.
3. What is the difference between SA1D AS80 and SA1C AS80?
The primary distinction is the substrate designation and its intended forming characteristics. SA1D is associated with deep-drawing applications, while SA1C is a commercial-grade designation. The choice should be based on verified mechanical properties and the component’s forming requirements, not on a general assumption that one material is always better.
4. Can this material be used for exhaust pipes?
It can be evaluated for suitable exhaust components, compresi tubi formati selezionati e parti della marmitta. La decisione richiede il controllo della temperatura di picco del metallo, ciclo termico, condensa di scarico, vibrazione, integrità della saldatura, e la durabilità del rivestimento nelle condizioni di servizio effettive.
5. Come si possono ridurre i danni al rivestimento durante la produzione dei tubi??
Utilizzare procedure di formatura e saldatura qualificate, evitare raggi di curvatura inutilmente stretti, controllare l'apporto termico di saldatura, e ispezionare il tubo finito per individuare eventuali crepe nel rivestimento e danni alla zona di saldatura. Dove necessario, specificare un trattamento protettivo post-saldatura compatibile per l'ambiente di servizio previsto.