- 説明
説明
アルミめっき溶接鋼管: Sourcing Tips for After-Market Exhaust System Manufacturers
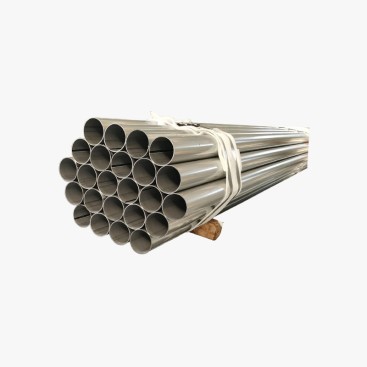
Aluminized welded steel pipe is widely used in the automotive aftermarket exhaust industry due to its balance of 費用対効果, 形成性, and high-temperature corrosion resistance. For exhaust system manufacturers, especially those producing mandrel-bent tubing systems, correct sourcing is critical to ensure bending quality and coating integrity.
This guide focuses on procurement requirements for aftermarket exhaust system production, including dimensional control, coating durability, and bending compatibility.
1. Why Aluminized Welded Pipe Dominates Aftermarket Exhaust Systems
| アドバンテージ | Impact on Exhaust Manufacturing |
|---|---|
| High cost-performance ratio | Lower cost than stainless steel while maintaining heat resistance |
| Good oxidation resistance | Al-Si coating protects against exhaust gas corrosion |
| 優れた成形性 | Suitable for mandrel bending and CNC tube forming |
| 軽量構造 | Reduces vehicle exhaust system weight |
2. Critical Sourcing Parameter: OD Tolerance & Wall Accuracy
| Parameter | Recommended Standard | Why It Matters |
|---|---|---|
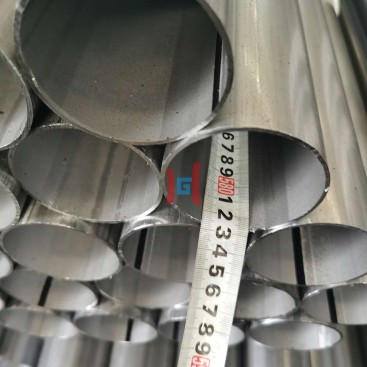
| 外径 (の) | ±0.10 mm to ±0.25 mm | Ensures compatibility with bending dies and connectors |
| 壁の厚さ | ±5–10% | Affects bending strength and exhaust durability |
| Ovality | ≤1.5% | Prevents distortion during mandrel bending |
Poor OD control can lead to bending deformation, cracking, or assembly mismatch in exhaust systems.
3. Mandrel Bending Compatibility Requirements
| Factor | Requirement |
|---|---|
| Material ductility | Low-carbon steel base for smooth deformation |
| Coating adhesion | Al-Si layer must remain intact after bending |
| Bend radius (R/D ratio) | Typically 1.5D–2.5D for exhaust tubing systems |
| 表面状態 | No micro-cracks or coating peeling allowed |
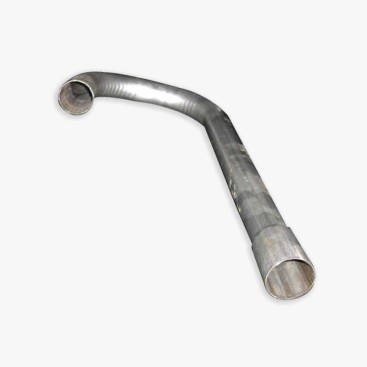
High-quality aluminized pipe should maintain coating integrity after cold forming and mandrel bending.
4. Coating Integrity After Bending
| Potential Issue | Cause | Solution |
|---|---|---|
| Micro-cracking of coating | Excessive bending stress | Use optimized Al-Si coating (9–10% Si) |
| Coating flaking | Poor adhesion or surface contamination | Improve pre-treatment and cleaning |
| Seam area weakness | ERW weld zone stress concentration | Post-weld normalization and controlled cooling |
5. Typical Exhaust System Applications
| 成分 | 関数 |
|---|---|
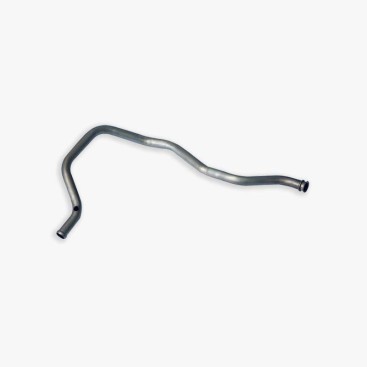
| 排気管 | Main gas flow channel |
| ミッドパイプ | Connect engine to muffler system |
| Muffler tubing | Noise reduction system structure |
| テールパイプ | Final exhaust outlet section |
6. Procurement Checklist for Buyers
| アイテム | What to Verify |
|---|---|
| Material certification | Ensure ASTM A463 / で 10346 compliance |
| Coating specification | Verify Al-Si coating weight (AS80 / AS120 / AS150) |
| 寸法検査 | Check OD, 壁の厚さ, and ovality reports |
| Bending test | Mandrel bend test without cracking or peeling |
| Surface quality | No pinholes, blisters, or coating discontinuity |
7. バイヤーが泰達江華を選ぶ理由
で 泰達江華, 当社は排気システムメーカー向けに特に最適化されたアルミめっき溶接鋼管を供給しています。, 安定した外径公差を確保, 均一なAl-Siコーティング, 信頼性の高いマンドレル曲げ性能.
OEMカットも承ります, 曲げ準備, 世界中の自動車アフターマーケット顧客向けの輸出対応パッケージ.
当社のアルミメッキ鋼管製品はこちらからご覧ください:
アルミめっき鋼管製品
結論
アフターマーケット排気メーカー向け, コストと性能の最適なバランスを実現するアルミめっき溶接鋼管. しかし, 調達は外径精度に重点を置く必要があります, コーティングの密着性, 実際の排気システムでの長期耐久性を確保するための曲げ互換性.