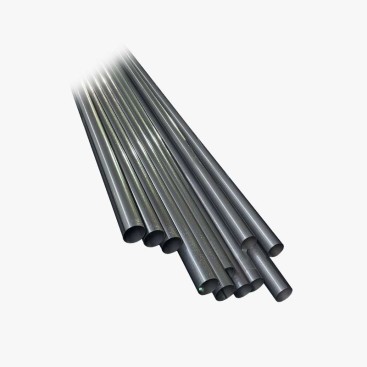
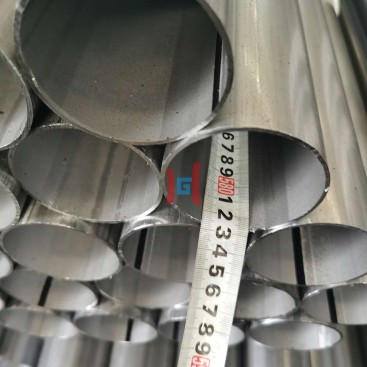
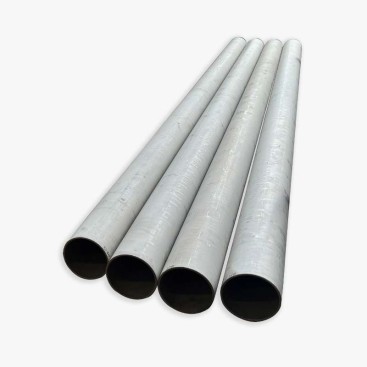
Aluminium Silicon Alloy Coated Steel Pipe


- Description
Description
Al-Si Alloy Coated Pipe: The Full Metallurgical Story — From Liquid Bath to Solid Protection
Aluminium silicon alloy coated steel pipe is not just a surface-treated product—it is a metallurgically bonded multi-layer system formed through controlled reactions between steel substrate and an Al-Si liquid bath. Its performance depends on the evolution of intermetallic compounds such as FeAl₃ and Fe₂Al₅, and how silicon modifies their growth.
This article explains the full metallurgical pathway: from molten coating bath → diffusion layer formation → intermetallic control → final protective structure.
1. Al–Si–Fe Phase System: The Foundation of Coating Behavior
| Element System | Metallurgical Role |
|---|---|
| Aluminium (Al) | Main corrosion-resistant coating element, forms protective oxide layer |
| Silicon (Si) | Controls diffusion rate and suppresses brittle phase growth |
| Iron (Fe) | Substrate element diffusing into coating during immersion |
In the Al–Si–Fe system, the key challenge is controlling iron diffusion into aluminum, which otherwise leads to brittle intermetallic layers.
2. Formation of Intermetallic Layers (Critical Engineering Zone)
| Layer Type | Behavior | Engineering Risk |
|---|---|---|
| Fe₂Al₅ (inner layer) | Fast-growing, hard, brittle intermetallic compound | Cracking under thermal or mechanical stress |
| FeAl₃ (outer intermetallic) | Less stable, forms under prolonged diffusion | Reduces ductility of coating system |
| Al-Si coating layer | Main protective layer above intermetallic zone | Performance depends on thickness control |
These layers form naturally during hot-dip aluminizing, but their thickness must be carefully controlled.
3. Why Silicon Changes Everything
| Silicon Function | Metallurgical Effect |
|---|---|
| Diffusion control | Slows Fe → Al interdiffusion rate |
| Phase stabilization | Limits excessive Fe₂Al₅ growth |
| Interface refinement | Produces thinner, more uniform intermetallic layer |
| Coating adhesion improvement | Reduces delamination risk under thermal cycling |
This is why industrial coatings typically use ~9–10% Si in aluminizing baths.
4. Simplified Metallurgical Evolution Path
| Stage | Process Description |
|---|---|
| Immersion in Al-Si bath | Steel enters molten alloy (~680°C) |
| Initial reaction | Iron begins diffusing into aluminum layer |
| Intermetallic formation | Fe₂Al₅ and FeAl₃ layers develop at interface |
| Solidification | Stable Al-Si coating forms outer protective layer |
The final structure is a multi-layer composite system with graded composition.
5. Performance Impact of Intermetallic Control
| Factor | Controlled Intermetallic Layer | Uncontrolled Growth |
|---|---|---|
| Flexibility | High | Low (brittle cracking) |
| Thermal cycling resistance | Stable | Coating spalling |
| Adhesion strength | Strong | Weak interface separation |
6. Key Industrial Applications
| Industry | Application |
|---|---|
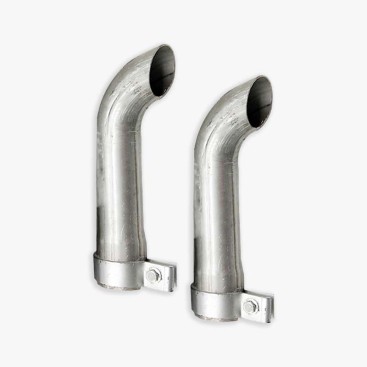
| Automotive | Exhaust systems, catalytic converter housings |
| Energy Systems | Flue gas ducts, thermal recovery pipelines |
| Industrial Heating | Furnace tubes, burner components |
| HVAC | High-temperature ventilation systems |
7. Why Buyers Choose Teda Ganghua
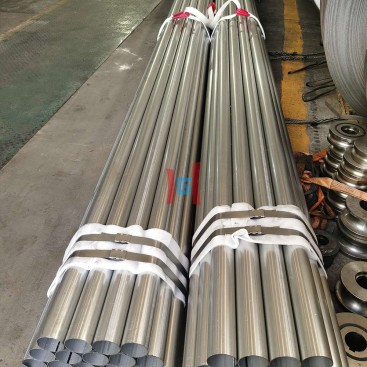
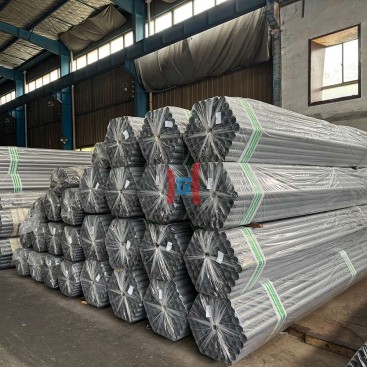
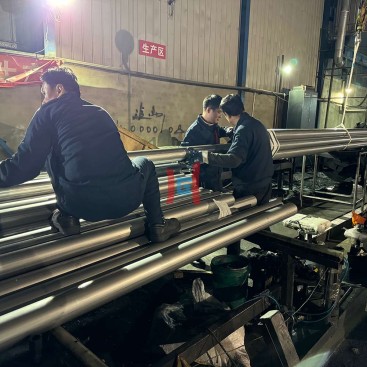
At Teda Ganghua, we supply aluminium silicon alloy coated steel pipes with controlled Al–Si composition, optimized intermetallic layer thickness, and stable metallurgical bonding for demanding industrial environments.
We support OEM cutting, bending, and export packaging solutions for global automotive and energy customers.
Explore our aluminized steel tube products here:
Aluminized Steel Tube Products
Conclusion
The performance of Al-Si coated steel pipe is governed by deep metallurgical reactions within the Al–Si–Fe system. By controlling intermetallic phases such as Fe₂Al₅ and FeAl₃, silicon ensures a stable, durable, and high-temperature resistant coating system suitable for modern industrial applications.