- Description
Description
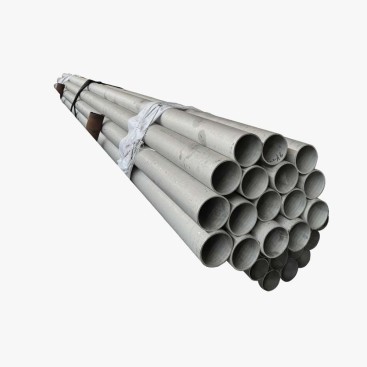
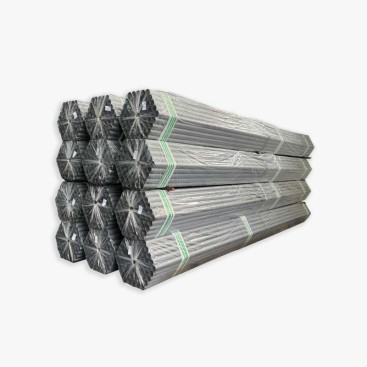
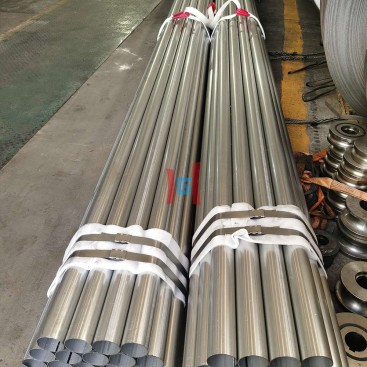
Aluminum-silicon coated steel tube uses a hot-dip Al-Si coating to combine the structural strength of a steel substrate with strong resistance to heat and atmospheric corrosion. The coating is mainly aluminum with a controlled silicon addition, commonly around 5–10%, and is widely used for automotive exhaust components, heat exchangers, oven parts, and other applications where both elevated temperature and corrosion resistance are required.
What Is an Al-Si Coated Steel Tube?
An Al-Si coated steel tube is produced by applying an aluminum-silicon alloy coating to a steel tube, normally through a hot-dip process. The aluminum provides the main barrier and heat-resistant function, while silicon helps control the reaction between the coating and the steel substrate.
The coating is therefore more than a simple aluminum layer. During hot dipping and subsequent processing, intermetallic phases develop between the coating and steel. This metallurgical structure is important because it determines coating adhesion, forming behavior, and resistance to thermal cycling.
Basic coating system
Outer layer: predominantly Al-Si coating
Intermediate layer: Fe-Al-Si intermetallic reaction layer
Substrate: steel tube providing mechanical strength
Three-Layer Al-Si Coating Structure
The performance of an Al-Si coated tube comes from the interaction between its coating and steel substrate. The structure can be simplified into three functional regions.
| Layer | Main characteristics | Primary function |
|---|---|---|
| Al-Si outer layer | Al-rich coating with controlled Si addition | Barrier protection and oxidation resistance |
| Fe-Al-Si reaction layer | Intermetallic phases formed during hot dipping | Metallurgical bonding and coating stability |
| Steel substrate | Carbon or low-alloy steel tube | Load-bearing structure and tube geometry |
The exact phase composition and thickness of the reaction layer depend on coating chemistry, bath temperature, dipping time, steel chemistry, and manufacturing conditions. It should therefore be regarded as a controlled metallurgical interface rather than a simple physical boundary.
Why Is Silicon Added to the Aluminum Coating?
Silicon plays an important role in controlling the reaction between molten aluminum and iron. Without suitable control of this reaction, an excessively thick intermetallic layer can develop during coating formation. Such a layer may become relatively brittle and can affect forming and coating durability.
A controlled silicon addition helps moderate the growth of iron-aluminum intermetallic compounds. This supports a better balance between coating adhesion, thermal stability, and fabrication performance.
Silicon helps limit excessive reaction-layer development during hot dipping.
The controlled interface promotes metallurgical bonding between coating and substrate.
The coating system is designed to remain stable through repeated heating and cooling.
Al-Si Coating vs Pure Aluminum Coating
Al-Si coating is often selected instead of a pure aluminum coating when the component will experience significant heat or thermal cycling. The silicon addition changes the coating/substrate reaction and helps control the intermetallic interface.
| Factor | Al-Si coating | Pure aluminum coating |
|---|---|---|
| Main coating chemistry | Aluminum with controlled silicon addition | Predominantly aluminum |
| Reaction-layer control | Silicon helps moderate intermetallic growth | More direct Fe-Al reaction must be controlled by process conditions |
| Thermal cycling | Well suited to repeated heating and cooling | Application dependent |
| Forming behavior | Designed for practical tube forming and fabrication | Depends strongly on coating structure and substrate |
| Typical use | Exhaust and heat-related components | Selected general corrosion-protection applications |
Coating Thickness and Coverage
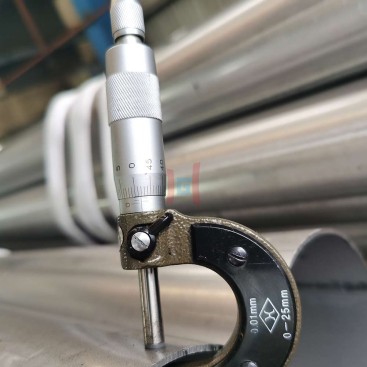
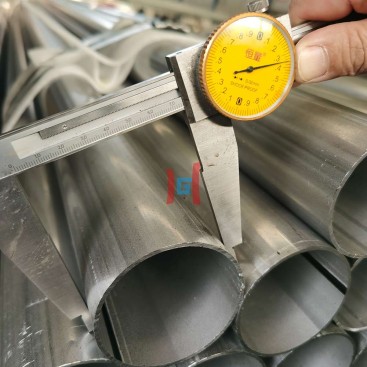
For industrial tubes, an Al-Si coating thickness of roughly 20–40 μm per side is a useful typical range, although actual values vary according to the product specification and manufacturing process. Coating mass may also be used instead of, or together with, thickness to define the amount of metallic coating.
A coating requirement should not be specified only by a generic thickness range when the tube is intended for a critical application. The buyer should identify the required coating mass or thickness, measurement location, minimum value, and inspection method.
Typical reference
Al-Si coating thickness: approximately 20–40 μm per side
Actual acceptance values should always follow the applicable product specification.
Heat and Corrosion Resistance
The main advantage of this coating system is its ability to protect the steel substrate under elevated-temperature conditions. Aluminum forms a stable oxide layer when exposed to oxygen, helping slow further oxidation of the coating.
For suitable Al-Si coated steel systems, continuous service temperatures around 677°C are commonly referenced in high-temperature applications. The actual allowable temperature depends on the substrate, coating system, atmosphere, thermal cycling, mechanical load, and exposure duration.
The coating also provides useful resistance against atmospheric corrosion and many condensate environments. However, high-temperature corrosion can involve sulfur, chlorides, water vapor, and other aggressive species, so application-specific testing may still be necessary.
Why It Works Well for Exhaust Systems
Automotive exhaust components experience repeated temperature changes, condensation, road contaminants, vibration, and external atmospheric exposure. Bare carbon steel can oxidize rapidly under these conditions.
The Al-Si coating provides a protective aluminum-rich surface while the steel substrate maintains the structural strength and formability needed for tube manufacturing. The controlled reaction layer helps the coating remain attached during fabrication and thermal cycling.
Typical Applications
Exhaust tubing and components exposed to heat, oxidation, and road environments.
Tubular components requiring a combination of thermal and corrosion resistance.
Tubular and fabricated parts exposed to elevated operating temperatures.
Selected industrial components requiring durable metallic surface protection.
How Is the Coating Inspected?
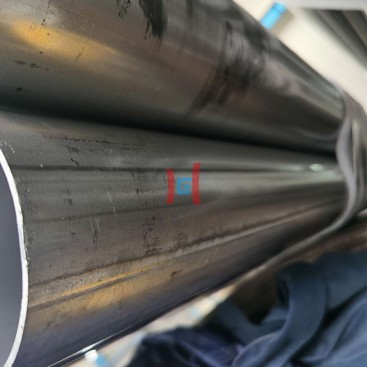
Coating quality should be evaluated by more than visual appearance. Two common quantitative controls are coating mass and coating thickness. Visual inspection can then be used to identify bare spots, cracking, excessive roughness, peeling, or other surface defects.
| Inspection item | What it evaluates | Why it matters |
|---|---|---|
| Coating mass | Amount of coating, commonly expressed in g/m² | Confirms coating coverage against the specified requirement |
| Coating thickness | Local or average metallic coating thickness | Helps verify barrier thickness and process consistency |
| Surface inspection | Visible defects and coating uniformity | Identifies local coating damage or production defects |
| Adhesion / bend assessment | Coating behavior after deformation | Important for formed and fabricated tubes |
Coating mass and thickness are related but should not be treated as identical measurements. The conversion depends on coating density, alloy composition, and whether the reported value represents one surface or both surfaces.
Ordering an Al-Si Coated Steel Tube
A complete inquiry should identify the tube dimensions and coating requirement together. Simply requesting an “aluminized tube” may leave important details undefined.
Recommended purchasing information
• Outside diameter or nominal tube size
• Wall thickness
• Tube length or coil form
• Steel grade and applicable standard
• Al-Si coating composition or applicable coating standard
• Minimum coating mass or thickness
• Surface and appearance requirements
• Forming, welding, flaring, or bending requirements
• Inspection and certification requirements
Source Aluminum-Silicon Coated Steel Tubes
Teda Ganghua provides sourcing support for aluminized steel products used in industrial and thermal applications. Buyers can review the aluminized steel tubes range and submit the required tube dimensions, steel grade, Al-Si coating specification, coating thickness or mass, quantity, and certification requirements.
For exhaust and heat-related projects, it is especially useful to provide the operating temperature, thermal cycling conditions, tube forming requirements, and exposure environment. These details help determine whether the selected coating and substrate are suitable for the actual service conditions.
FAQ
What is an aluminum-silicon coated steel tube?
It is a steel tube protected by a hot-dip aluminum-silicon alloy coating. The Al-Si layer provides oxidation and corrosion protection while the steel substrate supplies structural strength.
Why is silicon added to an aluminum coating?
Silicon helps control the reaction between aluminum and iron during coating formation. This limits excessive growth of brittle intermetallic phases and supports coating adhesion and fabrication performance.
How thick is an Al-Si coating?
A commonly referenced industrial range is approximately 20–40 μm per side, but the required value depends on the applicable product specification and intended service environment.
Can Al-Si coated tubes be used for automotive exhausts?
Yes. They are widely used for exhaust-related components because the coating provides useful resistance to oxidation, atmospheric corrosion, and repeated thermal exposure. The exact grade and coating system should be selected according to the exhaust design and operating conditions.
How should Al-Si coating quality be checked?
Common controls include coating mass in g/m², coating thickness, visual surface inspection, and adhesion or deformation testing where required. The acceptance criteria should be defined by the applicable specification.