- Description
Description
ERW Aluminized Steel Pipe: How Electric Resistance Welding + Aluminizing Creates the Industry Standard
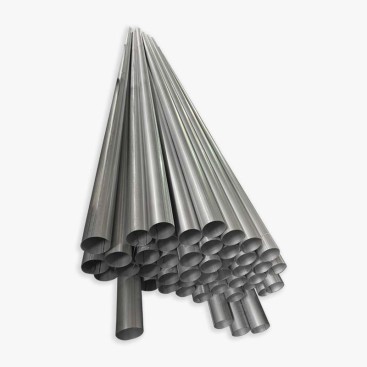
ERW aluminized steel pipe combines two core industrial processes: Electric Resistance Welding (ERW) and hot-dip aluminizing coating. This integrated production route has become a global standard for high-volume, cost-efficient, and performance-balanced tubular products used in automotive exhaust, HVAC, and heat-exchange systems.
The key value lies in combining precise welded tube forming with high-temperature corrosion protection provided by the aluminized layer.
1. What Is ERW Aluminized Steel Pipe?
| Process Stage | Description |
|---|---|
| ERW Tube Forming | Steel strip is formed into a tube and welded longitudinally using high-frequency current |
| Weld Seam Refinement | Flash removal and seam normalization to ensure uniform geometry |
| Hot-Dip Aluminizing | Tube is coated with Al-Si layer for corrosion and heat resistance |
| Cooling & Finishing | Controlled cooling stabilizes coating and mechanical properties |
This combination enables high production efficiency + enhanced surface protection.
2. Continuous Production Chain Advantage
| Stage | Industrial Benefit |
|---|---|
| ERW Forming Line | High-speed continuous tube production with tight dimensional control |
| Inline Surface Preparation | Ensures coating adhesion by removing oxidation and contaminants |
| Aluminizing Line | Uniform coating distribution across large-volume output |
| Post-Treatment | Improves coating stability and surface consistency |
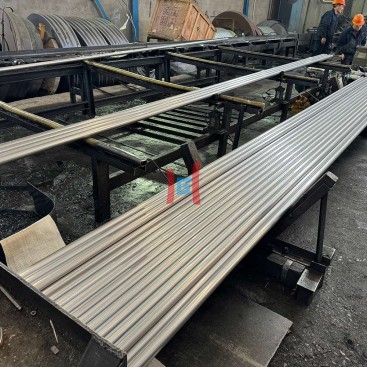
Modern ERW aluminized pipe production is designed for continuous, high-efficiency industrial manufacturing.
3. Weld Seam Coating Challenge & Solution
| Issue | Engineering Solution |
|---|---|
| Weld seam oxidation sensitivity | Pre-cleaning and controlled atmosphere treatment |
| Coating thickness variation at seam | Optimized immersion angle and bath flow control |
| Adhesion inconsistency | Surface activation and flux control before aluminizing |
Ensuring uniform coating over the weld seam is critical for corrosion resistance and long-term durability.
4. Why ERW + Aluminizing Is Widely Used
| Requirement | Benefit |
|---|---|
| High-volume production | ERW enables continuous, cost-efficient manufacturing |
| Thermal resistance | Aluminized coating withstands 600–800°C environments |
| Dimensional accuracy | ERW ensures consistent OD and wall thickness |
| Cost efficiency | Lower cost than seamless stainless steel alternatives |
This makes ERW aluminized pipe a preferred industrial solution for mass-market applications.
5. Key Application Areas
| Industry | Application |
|---|---|
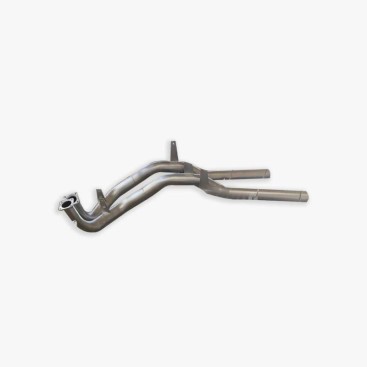
| Automotive | Exhaust pipes, muffler systems, emission control tubing |
| HVAC Systems | Ventilation ducts and heat-resistant air channels |
| Industrial Equipment | Gas transfer pipelines and furnace systems |
| Energy Systems | Flue gas and heat recovery piping |
6. Why Buyers Choose Teda Ganghua
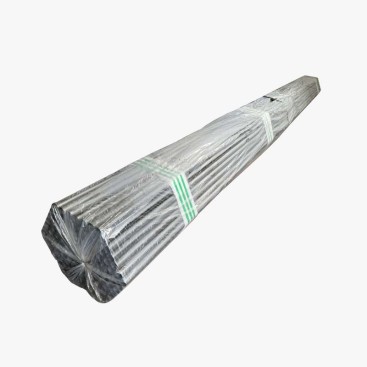
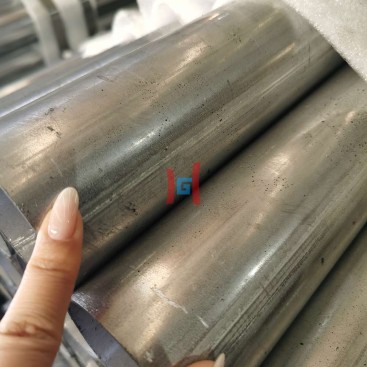
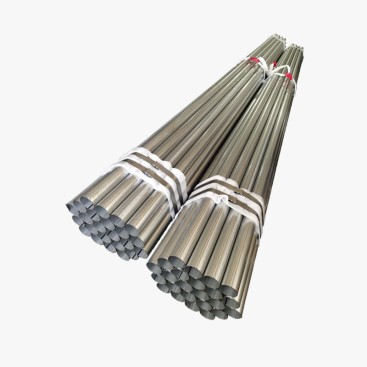
At Teda Ganghua, we supply ERW aluminized steel pipes with stable weld seam quality, uniform Al-Si coating distribution, and consistent mechanical performance for industrial-grade applications.
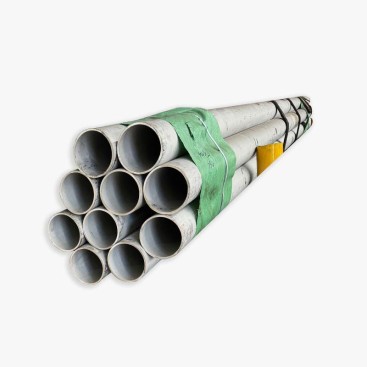
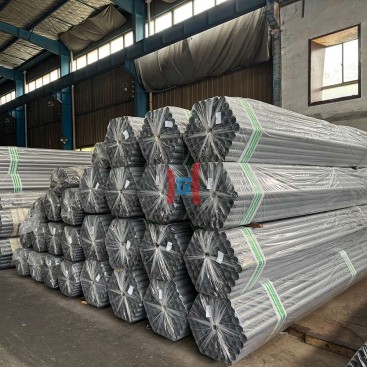
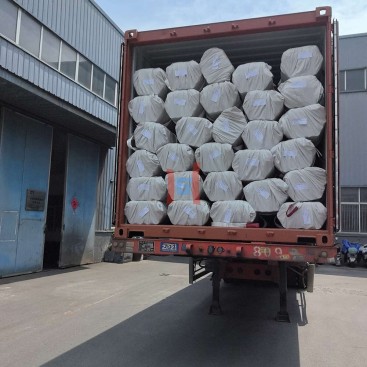
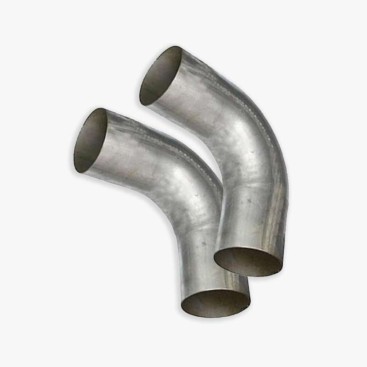
We support OEM cutting, bending, and full export packaging solutions for global automotive and industrial customers.
Explore our aluminized steel tube products here:
Aluminized Steel Tube Products
Conclusion
ERW aluminized steel pipe represents an optimized industrial balance between manufacturing efficiency and high-temperature corrosion protection. The combination of ERW forming and aluminizing coating makes it a global standard for cost-effective, large-scale tubular applications.