- Description
Description
Hot-Dip Aluminizing Process Demystified: How Steel Pipe Gets Its Aluminum Armor
Hot-dip aluminized steel pipe is produced through a controlled metallurgical process that bonds aluminum (or aluminum-silicon alloy) to a steel substrate. This creates a durable protective “armor layer” that significantly improves heat resistance, oxidation resistance, and service life in demanding industrial environments such as automotive exhaust systems, heat exchangers, and furnace piping.
Unlike painting or coating sprays, hot-dip aluminizing is a metallurgical diffusion process, meaning the coating becomes partially integrated with the steel surface at the atomic level.
1. Full Hot-Dip Aluminizing Process Flow
| Step | Process Description |
|---|---|
| 1. Surface Cleaning (Degreasing) | Removes oil, dust, and surface contaminants from steel pipe |
| 2. Acid Pickling | Removes oxide scale and activates the steel surface for coating |
| 3. Fluxing (助镀处理) | Prevents re-oxidation and improves coating adhesion |
| 4. Hot-Dip Immersion (~680°C) | Steel pipe is immersed into molten aluminum or Al-Si alloy bath |
| 5. Metallurgical Reaction | Iron reacts with aluminum forming Fe-Al intermetallic layers |
| 6. Withdrawal & Cooling | Controlled extraction and air cooling to stabilize coating structure |
2. What Happens at 680°C? (Core Science)
| Phenomenon | Result |
|---|---|
| Iron-Aluminum Diffusion | Forms intermetallic compound layers (Fe-Al phases) |
| Surface Alloying | Creates strong metallurgical bonding instead of simple adhesion |
| Silicon Addition (Al-Si bath) | Improves coating fluidity and reduces brittle layer formation |
This diffusion reaction is what makes hot-dip aluminized coatings far more durable than conventional paint or electroplating.
3. Coating Structure (Cross-Section Model)
| Layer | Function |
|---|---|
| Outer Al-Si Layer | Primary oxidation and corrosion protection barrier |
| Intermetallic Layer | Hard transition zone ensuring bonding strength |
| Steel Substrate | Mechanical strength and structural support |
The graded structure prevents peeling and ensures long-term stability under thermal cycling.
4. Why This Process Is Used for Steel Pipe
| Requirement | Benefit of Hot-Dip Aluminizing |
|---|---|
| High Temperature Exposure | Stable performance up to ~800°C |
| Oxidation Resistance | Prevents scaling in exhaust and furnace environments |
| Cost Optimization | Cheaper than stainless steel alternatives |
| Mechanical Strength | Retains carbon steel’s load-bearing capacity |
5. Industrial Applications
| Industry | Application |
|---|---|
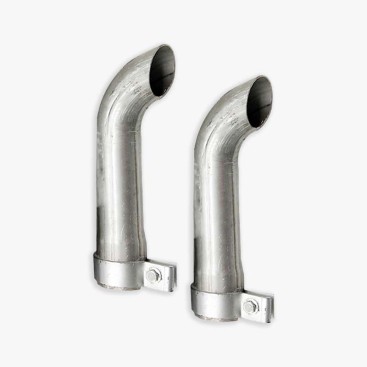
| Automotive | Exhaust pipes, mufflers, catalytic converter tubing |
| Heat Exchange Systems | Thermal transfer piping and ducts |
| Industrial Furnaces | High-temperature gas pipelines |
| Energy & HVAC | Flue gas and ventilation systems |
6. Why Buyers Choose Teda Ganghua
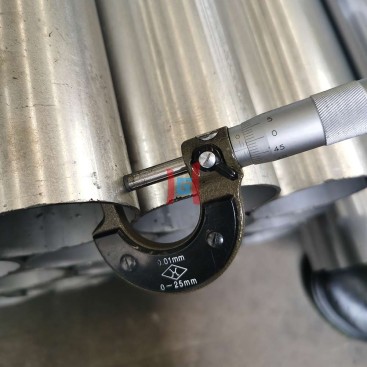
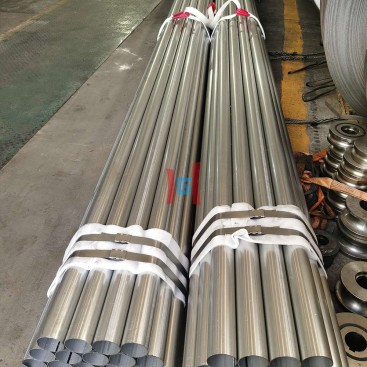
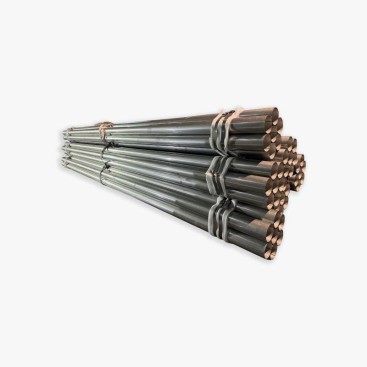
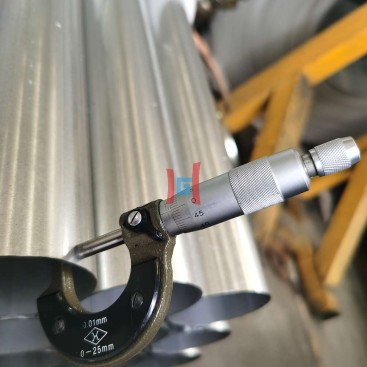
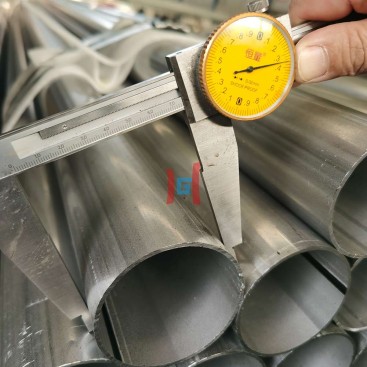
At Teda Ganghua, we supply hot-dip aluminized steel pipes with stable coating thickness, controlled Al-Si composition, and reliable metallurgical bonding for industrial-grade performance.
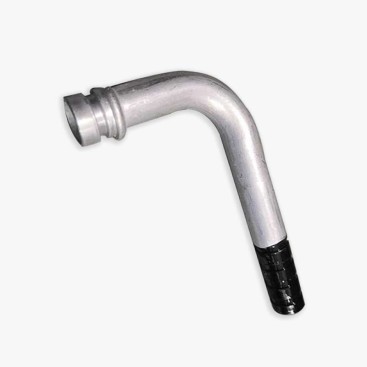
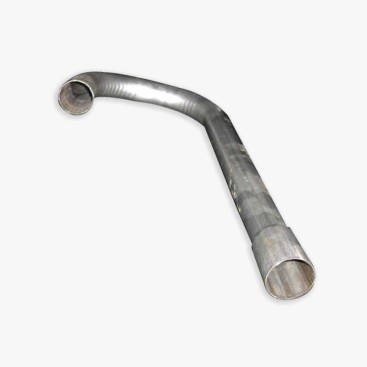
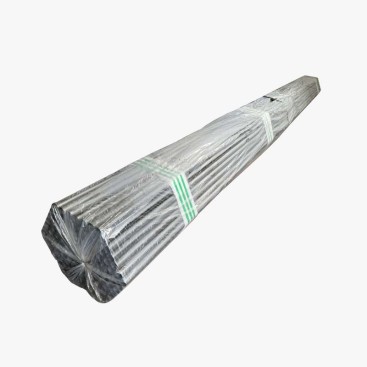
We support OEM cutting, bending, and full export packaging solutions for global automotive and industrial customers.
Explore our aluminized steel tube products here:
Aluminized Steel Tube Products
Conclusion
The hot-dip aluminizing process transforms ordinary steel pipe into a high-performance material with aluminum “armor.” Through acid cleaning, fluxing, immersion at ~680°C, and controlled cooling, a durable metallurgical coating is formed that enables long service life in extreme environments.