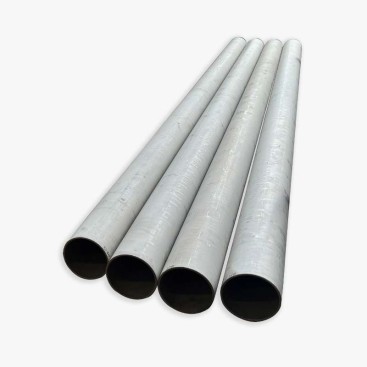
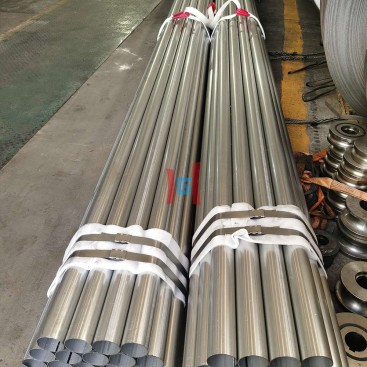
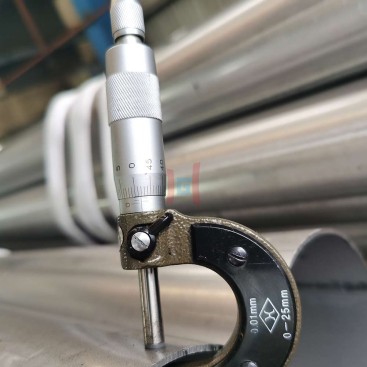
Hot Dipped Aluminum Coated Steel Pipe


- Description
Description
Hot dipped aluminum coated pipe should be evaluated by more than appearance alone. Coating weight, coating thickness, adhesion, surface uniformity, and service environment all affect the expected performance of the finished pipe. For buyers, these parameters provide a more practical way to compare coating grades and define acceptance requirements.
Coating Weight: AS90, AS120 and AS150
Coating weight is commonly used to describe the total mass of aluminum-based coating applied to a defined surface area. Designations such as AS90, AS120, and AS150 can be used as coating-grade references, with the numerical value generally indicating a nominal coating mass in g/m² under the applicable specification.
A higher coating weight normally provides more coating material for long-term environmental protection. However, the highest grade is not automatically required for every application. Temperature, condensate, chloride exposure, abrasion, forming, and expected service life should be considered together.
| Coating grade | Reference coating weight | Typical selection logic |
|---|---|---|
| AS90 | 90 g/m² | Moderate environmental exposure |
| AS120 | 120 g/m² | Higher protection requirement |
| AS150 | 150 g/m² | More demanding exposure or extended protection target |
AS coating designations should always be checked against the specific product standard or purchase specification. Coating weight may be defined differently depending on whether the requirement refers to total, single-side, or another measurement basis.
Coating Weight vs Coating Thickness
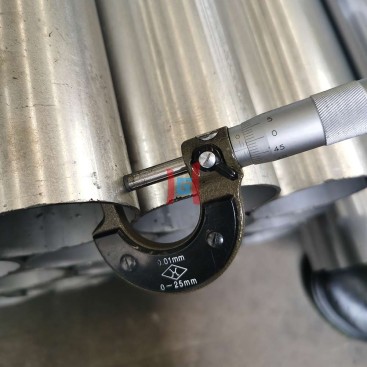
Coating weight and coating thickness describe related but different properties. A simple theoretical conversion can be made by using aluminum’s density of approximately 2.7 g/cm³. Under an idealized pure-aluminum assumption, about 1 μm of coating corresponds to roughly 2.7 g/m², not 6–7 g/m².
For hot-dip aluminum-coated steel, the actual coating is not pure aluminum. The coating can contain an aluminum-rich outer layer and an iron-aluminum-silicon intermetallic region. Its effective density and structure therefore differ from pure aluminum. A direct conversion from g/m² to μm should not be used as an exact acceptance method unless the applicable specification defines the relationship.
Important purchasing point
Use coating mass when the standard defines a mass-based grade, and use coating thickness when the drawing or inspection specification requires a dimensional measurement. Do not substitute one for the other without an agreed conversion method.
Why Adhesion Matters
A thick coating is not useful if it separates from the steel substrate during forming, impact, thermal cycling, or service. Hot-dip aluminizing creates a metallurgically bonded interface, but adhesion still needs to be evaluated according to the applicable product requirements.
Possible evaluation methods include bending tests, impact tests, and other coating-adhesion procedures. A cross-cut or scribe-type test may also be appropriate for certain coating systems, but the selected method should match the governing standard rather than being applied universally.
Salt Spray Testing: What It Can and Cannot Tell You
ASTM B117 is widely used as a laboratory practice for producing a controlled salt-fog environment. It can help compare corrosion behavior under defined test conditions, but a salt-spray result should not be converted directly into a guaranteed outdoor service life.
Real service environments contain variables that laboratory salt fog does not reproduce completely. Temperature cycling, wet-dry periods, pollutants, chloride concentration, mechanical damage, condensate, and exposure time can all influence actual performance.
| Inspection item | Purpose | Buyer consideration |
|---|---|---|
| Coating weight | Verify specified coating grade | Confirm measurement basis and sampling plan |
| Coating thickness | Check local coating depth | Compare with the agreed specification |
| Adhesion | Evaluate coating/substrate bonding | Use the applicable test method |
| Surface condition | Identify bare areas and visible defects | Define acceptable defect limits before shipment |
| Internal coating | Verify protection inside hollow pipe | Specify separately when required |
Coating Uniformity: Outside vs Inside
For hollow products, coating distribution may not be identical on the outside and inside surfaces. The external surface usually has easier access to the molten coating and may achieve more consistent coverage, while internal surfaces can be more difficult to coat, particularly in small-diameter or long tubes.
An “outer thicker, inner thinner” result is therefore possible in some production configurations. It should not automatically be classified as a defect. The correct question is whether both surfaces meet the minimum requirements established for the product.
For internal-service applications, specify:
- Whether internal coating is mandatory
- Minimum internal coating requirement
- Inspection location and method
- Acceptable local variation
- End-area treatment after cutting
Expected Service Life: Why One Number Is Not Enough
Service life depends on the exposure environment rather than coating grade alone. As a broad engineering reference, coated steel components used indoors under relatively mild conditions may remain serviceable for 10 years or more. Exhaust applications can be considerably more demanding, and a representative mid-temperature exhaust section may have a service-life range of roughly 3–7 years.
These figures should not be treated as guaranteed lifetimes. Exhaust temperature, thermal cycling, condensation, road salt, coating damage, tube geometry, and operating hours can move actual performance substantially above or below a general reference range.
How to Select the Coating Grade
| Service condition | Potential starting point | What should be checked |
|---|---|---|
| Indoor, mild atmosphere | AS90 | Humidity and expected service period |
| General outdoor exposure | AS120 | Moisture, salts, pollutants, and mechanical damage |
| More aggressive exposure | AS150 | Temperature, corrosion mechanism, and required service life |
| Exhaust / thermal service | Select from temperature and corrosion data | Continuous temperature, peaks, condensate, and cycling |
The grades above are selection examples, not universal classifications for every standard. The applicable specification should control the final coating designation and minimum coating requirements.
Four Checks for Incoming Inspection
A practical receiving inspection should focus on the parameters that directly affect coating performance:
- Coating weight: verify the measured value against the ordered grade and measurement basis.
- Adhesion: perform the agreed bending, impact, or other coating-adhesion test.
- Surface defects: inspect for bare areas, excessive buildup, cracks, damaged zones, and abnormal surface conditions.
- Coverage uniformity: check representative external and internal locations where internal coating is specified.
Source Hot-Dip Aluminum Coated Steel Pipe
Teda Ganghua can support coated steel tube and pipe sourcing for exhaust systems, thermal equipment, mechanical applications, and general corrosion-protection requirements. Buyers can review the Aluminized Steel Tubes range and specify the required pipe dimensions, substrate, coating grade, coating weight, internal coverage, and inspection requirements.
For projects with defined service-life targets, it is useful to provide the operating temperature, exposure environment, condensate conditions, forming requirements, and expected operating period. This allows the coating grade to be selected according to actual service conditions rather than coating weight alone.
FAQ
What does AS90 mean for aluminum-coated steel pipe?
AS90 is commonly used as a coating-grade reference corresponding to a nominal coating mass of 90 g/m² under the relevant specification. The exact measurement basis should always be confirmed in the applicable standard.
Is a higher coating weight always better?
Not necessarily. A higher coating weight can provide more protective material, but the best grade depends on temperature, corrosion exposure, forming, coating adhesion, and the required service life.
Can coating weight be converted directly into thickness?
Only as an approximation when the coating composition and density are known. Hot-dip coatings contain intermetallic regions, so a simple pure-aluminum conversion should not be used as an exact acceptance criterion.
Does ASTM B117 predict the actual service life of the pipe?
No. Salt-spray testing provides controlled laboratory exposure for comparative evaluation, but actual service life depends on the real environment, temperature, wet-dry cycles, contaminants, mechanical damage, and other factors.
Should internal coating be included in the purchase specification?
Yes, if internal corrosion protection is important. Internal coating coverage, minimum requirements, and inspection methods should be stated explicitly because internal surfaces can be more difficult to coat uniformly.