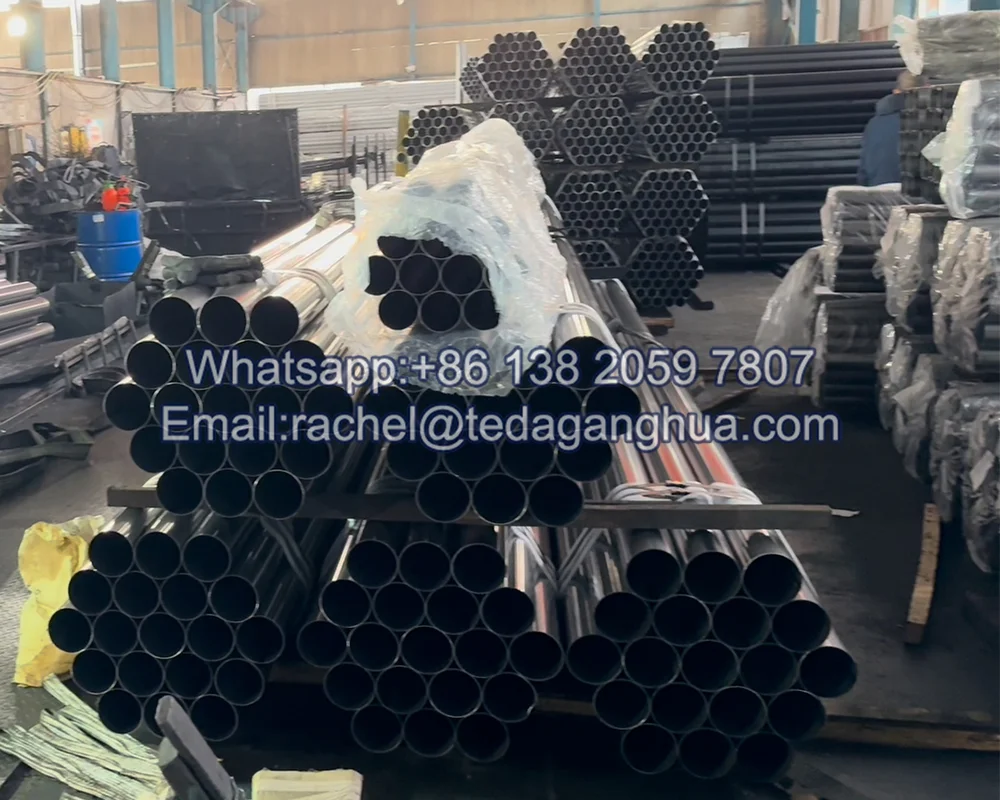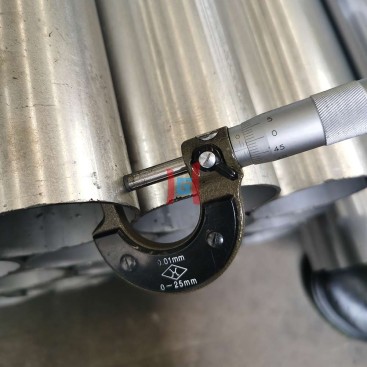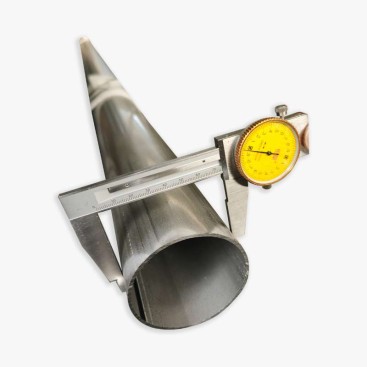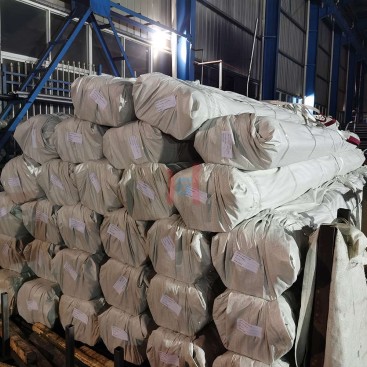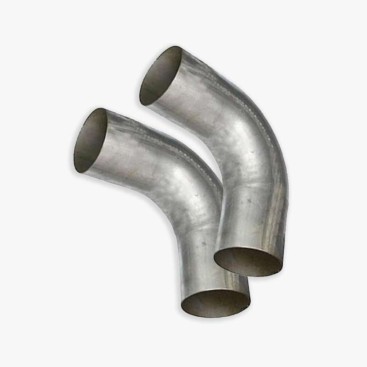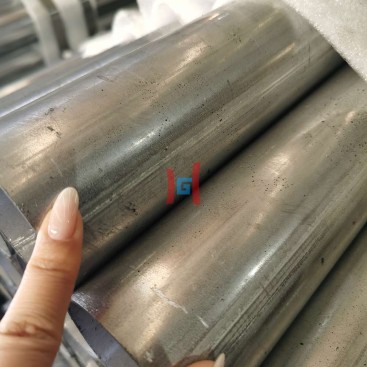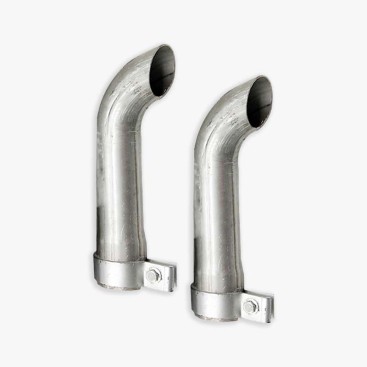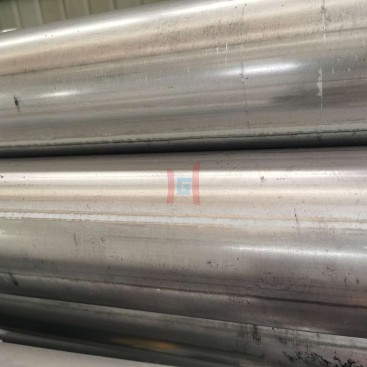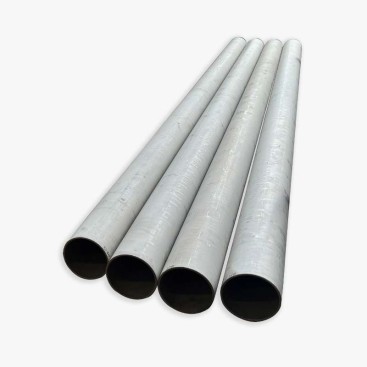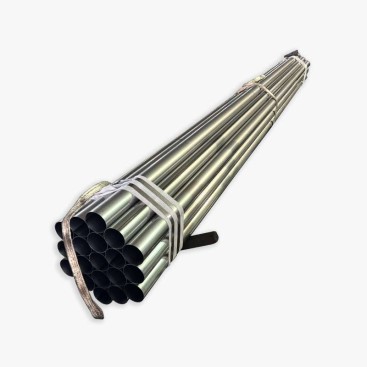
Холоднокатаная алюминизированная стальная труба
- Описание
Описание
Choosing between cold-rolled and hot-rolled steel substrate is an important decision when sourcing aluminized steel tubes. Both materials can be used to manufacture coated tubular products, but they differ in typical thickness availability, состояние поверхности, dimensional consistency, and cost. These differences influence not only the finished tube dimensions but also coating appearance and suitability for different applications. Cold-rolled substrate is generally preferred for thinner walls and appearance-sensitive components, while hot-rolled substrate is often considered for thicker, cost-sensitive structural applications. The right choice depends on the required tube performance rather than simply selecting one rolling process as universally better.
1. Cold-Rolled Base vs Hot-Rolled Base: The Main Differences
The substrate is the steel strip or sheet used to manufacture the tube. Cold rolling and hot rolling are different production routes that create different starting material characteristics. When these substrates are subsequently coated and formed into tubes, their original properties can influence the final product.
| Сравнение | Cold-Rolled Base | Hot-Rolled Base |
|---|---|---|
| Thickness range | Generally available in thinner gauges | Commonly used for thicker gauges |
| Состояние поверхности | Usually smoother and more uniform | Generally rougher, depending on descaling and finishing |
| Thickness tolerance | Often tighter | Often wider |
| Расходы | Generally higher due to additional processing | Generally lower for comparable material specifications |
| Типичные применения | Компоненты выхлопной системы, техника, precision parts, appearance-sensitive products | Structural tubes, скобки, supports, and non-appearance-critical parts |
These are general production tendencies rather than fixed rules. Actual thickness ranges and tolerances depend on the steel grade, strip width, rolling line, coating route, and tube-forming equipment. A hot-rolled substrate can also be descaled and surface-treated, while the final appearance of a cold-rolled-based tube still depends on coating and fabrication quality.
2. Thickness Availability: Why the Starting Material Matters
Cold-rolled steel is commonly selected when a project requires relatively thin material and closer thickness control. The cold reduction process allows producers to manufacture thinner gauges and achieve a more consistent thickness profile than many conventional hot-rolled products.
Hot-rolled steel is commonly selected for thicker sections where a very thin wall is not necessary. It can be a practical option for structural tube applications, скобки, equipment supports, and other components where strength and cost are more important than a refined surface appearance.
Однако, buyers should not assume that every cold-rolled product is thinner than every hot-rolled product. The available ranges can overlap. The correct comparison should be made using the actual substrate thickness, терпимость, and finished tube dimensions offered by the supplier.
Purchasing point
Ask suppliers to confirm whether the quoted thickness refers to the steel substrate before coating or the finished coated tube wall. The measurement basis should be consistent when comparing quotations and inspecting deliveries.
3. Surface Condition and Coating Appearance
Surface condition is one of the most visible differences between cold-rolled and hot-rolled substrate. Cold-rolled steel generally has a smoother and more uniform starting surface. This can provide a more consistent foundation for subsequent coating and is often preferred when the finished tube will remain visible.
Hot-rolled substrate typically has a rougher surface before descaling or other surface preparation. Surface scale, residual roughness, and local variations may influence coating preparation and the final appearance. The actual result depends heavily on how the material is cleaned and conditioned before coating.
A smoother substrate can make it easier to achieve a visually uniform coating, but it does not automatically guarantee uniform coating thickness. Coating bath conditions, line speed, wiping or air-knife control, дренаж, температура, and material geometry are also important factors.
4. Why Surface Roughness Can Affect Coating Uniformity
An often-overlooked issue is the relationship between substrate surface condition and coating thickness distribution. During hot-dip coating, the steel surface is exposed to molten coating metal. Surface topography, cleanliness, wetting behavior, and process control can all influence how the coating forms and drains.
A rougher or less consistent surface may create local variations in coating appearance and thickness. Peaks, valleys, residual oxides, and surface contamination can affect wetting and the way excess molten metal is removed. Как результат, achieving a consistent coating appearance may require more careful surface preparation and process control.
Factors influencing coating consistency
- Substrate roughness: Surface peaks and valleys influence local coating geometry and appearance.
- Surface cleanliness: Масло, oxides, and contaminants can interfere with coating wetting.
- Bath and line conditions: Температура, immersion conditions, and line speed influence coating formation.
- Coating removal control: Wiping or air-knife settings influence the amount and distribution of excess coating metal.
- Tube forming: Bending and welding may change the coating condition after the original strip has been coated.
For appearance-sensitive components, cold-rolled substrate is generally the preferred starting point because its smoother surface can support a more consistent finished appearance. This is a manufacturing consideration, not a judgment about the overall quality grade of hot-rolled steel. A properly prepared hot-rolled substrate can still meet demanding requirements when the application and acceptance criteria are appropriate.
For critical applications, buyers should specify measurable coating requirements, such as coating mass or thickness where applicable, coverage, surface defects, and inspection methods. Visual descriptions alone are not sufficient when coating uniformity is a key acceptance condition.
5. Thickness Tolerance and Finished Tube Accuracy
Cold-rolled substrate often provides tighter thickness control, which can help manufacturers maintain more consistent input material during tube forming. This is particularly useful for thin-wall tubes, precision components, and products that require consistent dimensions across production batches.
Hot-rolled substrate generally has wider thickness variation, depending on its specification and production route. For structural applications, this may be acceptable if the finished tube meets the required wall thickness, сила, and dimensional tolerances.
The final tube tolerance is not determined by substrate rolling alone. Forming accuracy, weld seam control, калибровка, straightening, резка, and inspection all contribute to the finished dimensions. Buyers should therefore define both the starting material requirements and the final tube acceptance tolerances.
| Объект проверки | Substrate Check | Finished Tube Check |
|---|---|---|
| Толщина | Incoming strip thickness and tolerance | Finished wall thickness and tolerance |
| Поверхность | Roughness, cleanliness, and surface defects | Coating appearance, преемственность, and visible defects |
| Dimensions | Strip width and flatness where relevant | Outside diameter, ovality, длина, and straightness |
| Изготовление | Formability and material condition | Weld seam, forming condition, and dimensional stability |
6. Which Substrate Is Better for Your Application?
The most suitable substrate depends on the balance between wall thickness, appearance, dimensional requirements, service conditions, and budget. The following guide helps buyers identify a practical starting point.
| Substrate Type | Typical Thickness Position | Suitable Application Direction |
|---|---|---|
| Cold-rolled base | Thinner gauges, subject to production-line capability | Компоненты выхлопной системы, техника, precision tubes, visible parts |
| Hot-rolled base | Thicker gauges, subject to product specification | Structural tubes, скобки, supports, industrial components |
For exhaust components and appliance parts, surface appearance, thinner wall requirements, and dimensional consistency may make cold-rolled substrate the better starting choice. For brackets, supports, and structural components, hot-rolled substrate may provide a more economical solution when its surface and tolerance characteristics satisfy the design.
The application environment must also be considered. A tube exposed to high temperatures may require an aluminum-silicon alloy coating, while other applications may call for a different aluminum coating system. Substrate selection and coating selection are separate decisions and should be specified independently.
7. How to Compare Supplier Offers
When comparing quotations, do not evaluate suppliers only by the words cold rolled or hot rolled. Ask each supplier to provide the same technical information so that the offers can be compared on an equivalent basis.
Supplier comparison checklist
- Substrate type and steel grade.
- Nominal substrate thickness and tolerance.
- Available thickness range for the required tube size.
- Substrate surface condition and finished coating appearance.
- Coating composition and applicable specification.
- Finished tube outside diameter, толщина стены, and length.
- Weld seam condition and coating coverage requirements.
- Material certificates and agreed inspection records.
A supplier should also confirm whether the product is made from pre-coated strip or coated after tube forming. This difference can affect the weld seam, internal coating, cut ends, and the inspection method. It is especially important for products used in corrosive or high-temperature environments.
8. Теда Ганхуа: Matching Substrate to Tube Requirements
Teda Ganghua Metal is a steel stockist based in Tianjin TEDA, с 20 years of steel stockist and export experience. The company supports international industrial buyers with steel sourcing, specification coordination, услуги по обработке, документация по качеству, and export shipment arrangements.
For customers sourcing aluminized steel tubes, Teda Ganghua can help clarify the required substrate type, thickness range, допуски на размеры, спецификация покрытия, и требования к приложению. This helps buyers distinguish between a cold-rolled base selected for thinner walls and better surface consistency and a hot-rolled base selected for thicker or more cost-sensitive products.
Depending on product availability and confirmed manufacturing capabilities, purchasing support may include:
- Cold-rolled and hot-rolled substrate specification coordination.
- Марка стали, толщина, and tolerance confirmation.
- Aluminum or aluminum-silicon coating requirement review.
- Резка, сварка, изгиб, and other processing services where applicable.
- Material Test Certificates and material traceability documentation.
- Third-party inspection arrangements and shipment verification.
Teda Ganghua maintains substantial steel inventory and works with established steel mill partners to support different industrial purchasing requirements. The company emphasizes specification-based sourcing, accurate shipment quantity verification, and material quality documentation.
Buyers are welcome to arrange inspections before shipment to verify the agreed material grade, размеры, количество, and quality requirements. For projects with strict appearance or wall-thickness requirements, confirming the substrate and finished tube inspection criteria before production is particularly important.
Часто задаваемые вопросы
1. What is the main difference between cold-rolled and hot-rolled aluminized steel tubes?
Cold-rolled substrate is generally thinner, smoother, and more dimensionally consistent, while hot-rolled substrate is commonly used for thicker and more cost-sensitive applications. The final tube quality also depends on coating and tube-forming processes.
2. Does cold-rolled substrate always produce a more uniform coating?
Не автоматически. Its smoother surface can support a more consistent appearance, но однородность покрытия зависит еще и от чистоты поверхности, банные условия, line speed, контроль удаления покрытия, и осмотр.
3. Какая подложка лучше для вытяжных труб?
Холоднокатаная основа часто является подходящей отправной точкой для выхлопных труб, требующих более тонких стенок., хорошая консистенция поверхности, и контроль размеров. Тип покрытия также необходимо выбирать в зависимости от рабочей температуры и условий окисления..
4. Когда горячекатаная подложка является практичным выбором?
Горячекатаная подложка часто подходит для более толстых конструкционных труб., скобки, supports, и компоненты, для которых улучшенная обработка поверхности не является существенной и может быть достигнут указанный допуск по толщине..
5. Какую информацию следует включать в запрос?
Укажите тип подложки, марка стали, номинальная толщина и допуск, тип покрытия, внешний диаметр, толщина стены, длина, требования к поверхности, и критерии проверки. Также подтвердите, наносится ли покрытие до или после формования труб..