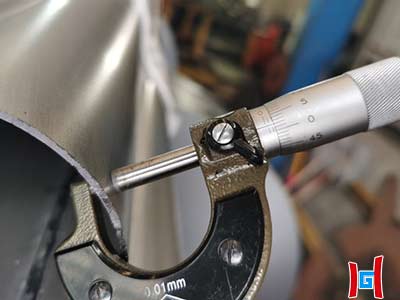
DX54D+AS Tiub Keluli Beralum: Gred, Salutan & Panduan RFQ
DX54D+AS sering digambarkan dalam pasaran sebagai “tiub aluminized,” tetapi penerangan ini secara teknikalnya tidak lengkap. Menurut EN 10346, DX54D+AS refers to a continuously hot-dip-coated flat steel product: DX54D defines the formability of the steel substrate, while +AS denotes an aluminum-silicon coating system. Finished aluminized tubes are typically manufactured by forming and welding this coated flat steel. Oleh itu, tube specifications must separately define the substrate grade, coating mass, proses pembuatan, and dimensional requirements for the finished tube.
1. First Correction: DX54D+AS Is Not a Tube Grade
This distinction is critical when preparing a request for quotation (RFQ) or technical data sheet. DALAM 10346 covers continuously hot-dip-coated flat steel products for cold forming, but it does not establish “DX54D+AS tubing” as an independent tube or pipe grade. [Gred Tiub DX54D+AS atau Keluli Rata Bersalut? Panduan Spesifikasi]
| Specification Level | What It Defines | Procurement Question |
|---|---|---|
| DX54D | Cold-forming steel substrate and mechanical properties | Is the substrate actually DX54D? |
| +AS | Hot-dip aluminum-silicon coating | What coating mass is required? |
| Tube Standard | Dimensi tiub, toleransi, keperluan membentuk dan kimpalan | Which tube standard and manufacturing process apply? |
Procurement Rule: Never specify only “DX54D+AS tube.” A complete technical purchase order should identify the substrate grade, coating designation and mass, tube manufacturing standard, dimensi, toleransi, keperluan kimpalan, and inspection documentation.
Material Numbers: 1.0306 dan 1.0952
As European standards evolve, older drawings and supplier documents may contain different material numbers associated with the DX54D material designation. Historical documents may reference 1.0306, whereas current documentation may identify DX54D using material numbers such as 1.0952 under updated EN 10346-related documentation. [1.0306 atau 1.0952? DX54D Peralihan Nombor Bahan Diterangkan]
When the material number on an older drawing differs from that on a current mill certificate, procurement teams should not automatically treat the materials as different grades. Sebaliknya, verify the applicable edition of the standard and, where necessary, request a formal equivalence statement or material identification declaration.


2. Decoding DX54D+AS
| Symbol | Meaning | Technical Significance |
|---|---|---|
| DX | Cold-forming steel designation | Identifies a steel family designed for forming and continuous hot-dip coating |
| 54 | Deep-drawing grade designation | Indicates enhanced formability within the DX steel family compared with general forming grades |
| D | Designation for flat steel products intended for hot-dip coating | Distinguishes this material designation from other steel product and coating systems |
| + | Coating designator separator | Separates the substrate grade from the coating designation |
| AS | Salutan aluminium-silikon | Identifies an aluminum-based coating system designed to provide resistance to high-temperature oxidation |
The same DX54D substrate can be combined with several different coating systems, including zinc, zinc-iron, zinc-aluminum, zinc-magnesium, aluminum-zinc, and aluminum-silicon coatings. Oleh itu, replacing +AS with another coating designation is not simply a cosmetic substitution. It changes the coating system and may affect the finished material’s corrosion resistance, rintangan haba, and processing characteristics. [+Salutan AS lwn +Z: Panduan Aluminium-Silikon vs Zink Steel]
3. DX54D Mechanical Properties: Why It Is a Deep-Drawing Steel
For procurement purposes, the deep-forming performance of DX54D should be evaluated using multiple mechanical indicators rather than elongation alone. Typical requirements include tensile strength, pemanjangan, plastic strain ratio, and work-hardening behavior, with applicable thickness corrections determined in accordance with the relevant standard. [r90 vs n90 dalam Pembentukan Lembaran Logam Lukisan Dalam]
| Harta benda | Typical DX54D+AS Requirements | Procurement Significance |
|---|---|---|
| Kekuatan Hasil, Re | Approximately 120–220 MPa* | Indicates a low-strength substrate with high formability |
| Kekuatan Tegangan, Rm | Approximately 260–350 MPa | Defines the tensile strength range of the forming-grade steel |
| Pemanjangan, A80 | ≥34%* | Represents overall deformation capacity |
| r90 | ≥1.4* | Indicates resistance to excessive sheet thinning during forming |
| n90 | ≥0.18* | Indicates work-hardening behavior and strain distribution |
*Applicable requirements and permitted values must always be verified against the exact edition of the standard, product thickness, surface quality requirements, and contractual specifications. [a80 r90 n90: Mengapa Keperluan Lukisan Dalam Tolok Nipis Dilonggarkan]
[Jaminan Keluli Enam Bulan: Can Lembaran Berusia Masih Dicop?]
Thickness Corrections Must Be Specified in the Contract
Formability requirements for thin-gauge material may need to be adjusted. This is particularly important when purchasing material thinner than approximately 0.70 mm. If a specification states only “r90 ≥ 1.4” without identifying the applicable thickness correction, the supplier and buyer may apply different acceptance criteria to the same coil.
| Thickness Range | A80 Adjustment | r90 Adjustment | n90 Adjustment |
|---|---|---|---|
| 0.50 ≤ t < 0.70 mm | −2 percentage points | −0.2 | −0.01 |
| 0.35 ≤ t < 0.50 mm | −4 percentage points | −0.4 | −0.03 |
| t < 0.35 mm | −7 percentage points | −0.6 | −0.04 |
| 1.50 < t ≤ 2.00 mm | - | −0.2 | - |
| t > 2.00 mm | - | −0.4 | - |
The practical lesson is straightforward: never copy thin-gauge formability requirements directly from a general DX54D datasheet without checking the provisions applicable to the specific thickness.
4. Komposisi Kimia: Distinguishing the Steel Substrate from the Coating
Untuk DX54D, chemical composition requirements apply to the steel substrate, not the aluminum-silicon coating. Typical maximum values for the substrate include the following:
| C | Dan | Mn | P | S | Al |
|---|---|---|---|---|---|
| ≤0.12% | ≤0.50% | ≤0.60% | ≤0.10% | ≤0.045% | ≤0.30% |
A common specification error is to see a silicon limit for the substrate and assume that it describes the coating composition. It does not. Silicon in the substrate’s chemical composition and silicon used in the aluminum-silicon coating belong to different metallurgical systems and must be evaluated separately.
5. What Does +AS Mean?
The +AS coating is an aluminum-silicon alloy coating, not a pure aluminum coating. Industrial aluminum-silicon coatings typically contain several percent silicon, with compositions containing approximately 10% silicon widely used. This coating system is designed to provide resistance to high-temperature oxidation while maintaining good adhesion and processability.
Jenis Salutan
Uses an aluminum-silicon alloy rather than pure aluminum.
Typical Silicon Content
Approximately 5–11% silicon in common industrial formulations, depending on the specification.
Common Coating Designations
AS060, AS080, AS100, AS120, and AS150 are commonly used designations.
Aplikasi Biasa
High-temperature components, exhaust-related products, peralatan pemanas, and other heat-exposed parts.
AS120 and ASTM A463 Type 1: Compare Coating Mass, Not Just Standards
EN and ASTM coating standards use different designation systems and units. Under the applicable EN coating system, AS120 denotes a nominal total coating mass of 120 g/m² across both surfaces. Jenis ASTM A463 1 uses designations expressed in ounces per square foot, such as T1-13, T1-25, T1-40, and T1-60. [EN ASTM JIS Perbandingan Piawaian Keluli Bersalut ISO Al-Si]
| EN Coating Designation | Nominal Total Coating Mass | Approximate ASTM Type 1 Perbandingan |
|---|---|---|
| AS060 | 60 g/m² | Below T1-25 |
| AS080 | 80 g/m² | Close to the T1-25 range |
| AS120 | 120 g/m² | Close to T1-40, approximately 122 g/m² |
| AS150 | 150 g/m² | Between T1-40 and T1-60 |
Important: These are comparison values, not automatic declarations of material equivalence. The coating chemistry, test method, minimum values, designation rules, and application requirements must still be verified against the applicable standard. [AS060 lwn AS080 lwn AS100 lwn AS120 lwn AS150 Panduan Salutan]
AS120 Coating Thickness: A Useful Engineering Estimate
If a total coating mass of 120 g/m² is distributed equally across two surfaces, each side accounts for approximately 60 g/m². Using an approximate density of 2.7 g/cm³ for an aluminum-based coating gives a theoretical single-side thickness of roughly 22 μm. This calculation is intended as an engineering estimate only. Actual coating thickness and distribution should be established using the applicable coating-mass test method and supplier documentation.
6. Deep Drawing: Why DX54D Is Suitable for Complex Forming
DX54D is intended for demanding cold-forming applications. Its forming behavior depends on the combined effects of elongation, plastic anisotropy, and work-hardening characteristics.
| Indicator | What It Controls | Why It Matters in Tube Production |
|---|---|---|
| A80 | Overall elongation capacity | Supports forming without premature tensile fracture |
| r90 | Resistance to localized thinning | Important during deep drawing and severe cross-sectional deformation |
| n90 | Work-hardening behavior | Influences how deformation is distributed throughout the forming zone |
Another procurement consideration is resistance to stretcher strains. Surface strain marks can become a quality issue for components where appearance is important. For deep-drawing applications, material age should therefore be managed alongside mechanical properties and surface-quality requirements.
Where a supplier provides a defined aging or surface-quality guarantee period, the contract should state that requirement explicitly. Older stock should not automatically be considered equivalent to freshly produced material simply because the nominal grade remains unchanged.
7. The Critical Issue in Tube Manufacturing: Coating vs. Kimpalan
Converting coated flat steel into tubing introduces a processing challenge that does not arise in exactly the same way when the product remains flat sheet: the aluminum-silicon coating interacts with the welding process.
| Manufacturing Stage | Potential Issue | Procurement Requirement |
|---|---|---|
| Welding Zone | The coating may affect weld-pool behavior and weld quality | Define the welding procedure and treatment of the weld zone |
| Kaedah Kimpalan | Process parameters must account for the coated steel substrate | Specify a qualified welding procedure and applicable consumables |
| Post-Weld Protection | Coating removed or affected by heat may leave areas with reduced protection | Define local protection or coating-repair requirements |
| Tube Forming | Severe bending or expansion may place stress on the coating | Verify coating adhesion after forming |
| Cut Edges | Exposed steel edges have less coating protection | Specify edge condition and any required sealing or protection |
Engineering Focus: For welded aluminized tubing, substrate selection is only one part of the corrosion-performance equation. The weld zone, cut edges, forming radius, and post-processing protection can determine the actual service performance of the finished tube.
8. Cross-Standard Comparison: Do Not Match Designations by Name Alone
| System | Standard | Typical Designation | Procurement Note |
|---|---|---|---|
| European | DALAM 10346 | DX54D+AS | Coated flat steel product; the tube standard must be specified separately |
| Historical European | Earlier EN specifications | DX54D+AS with historical material references | Older drawings should be checked against the current edition of the applicable standard |
| American | ASTM A463/A463M | taip 1 Al-Si; T1 coating designations | taip 1 dan Jenis 2 are different coating systems |
| Japanese | JIS G 3314 | SA1C / SA1D / SA1E | Verify the grade, coating mass, dan aplikasi yang dimaksudkan |
| International | ISO 5000 | Al-Si-coated cold-rolled carbon steel flat products | Check the exact mechanical and coating requirements |
The correct sequence for cross-standard comparison is substrate grade → coating chemistry → coating mass → mechanical requirements → dimensions → test method. A Type 1 Al-Si coating should not be considered interchangeable with a Type 2 pure-aluminum coating simply because both are described as aluminized steel.
9. Typical Applications and Selection Limitations
Automotive Exhaust Components
Suitable for applications requiring formability combined with resistance to high-temperature oxidation and atmospheric corrosion.
Aluminized Tubes and Fittings
Useful where coated steel tubing is required for exhaust systems, peralatan pemanas, or other temperature-exposed applications.
Heating Equipment
Applicable to selected oven, relau, heat-shield, and heat-exchanger components.
HVAC and Industrial Enclosures
Can combine cold-forming capability with atmospheric corrosion resistance in selected applications.
When Should DX54D+AS Be Reconsidered?
- Extremely high service temperatures: Verify the actual continuous and cyclic operating temperatures rather than relying on generic statements about coating temperature resistance.
- Severe chloride or chemical exposure: Evaluate the complete corrosion environment and compare alternative material systems.
- Primary load-bearing structures: The low-strength deep-drawing substrate is not automatically suitable for structural applications requiring high yield strength.
- Highly visible surfaces: Establish surface-quality, membentuk, and weld-zone requirements before production.
- Severe post-forming operations: Confirm coating adhesion and the permissible forming radius before selecting the coating mass.
10. DX54D+AS Tube Specification: Complete RFQ Checklist
A professional aluminized tube specification should distinguish material requirements from finished-tube requirements. The following checklist can be incorporated into an RFQ:
| item | Required Information |
|---|---|
| 1. Substrat | DX54D and the applicable EN 10346 jawatan |
| 2. Salutan | +AS and the exact coating mass designation, such as AS060, AS080, AS100, AS120, or AS150 |
| 3. Coating-Mass Convention | Clearly specify the total mass across both surfaces or the applicable alternative measurement convention |
| 4. Sifat Mekanikal | Re, Rm, A80, r90, and n90, including applicable thickness corrections |
| 5. Komposisi Kimia | Heat analysis and material certificate requirements |
| 6. Tube Dimensions | Outside diameter, ketebalan dinding, panjang, bujur, and dimensional tolerances |
| 7. Kaedah Pembuatan | Membentuk, mengimpal, and any subsequent tube-forming operations |
| 8. Weld Requirements | Welding procedure, weld inspection, and treatment of the coated zone |
| 9. Edge Protection | Protection requirements for cut edges and weld areas |
| 10. Kualiti Permukaan | Surface class, permissible defects, and coating adhesion requirements |
| 11. Material Age | Applicable forming-quality or aging-guarantee requirements |
| 12. Inspection Documentation | Mechanical, kimia, coating-mass, lekatan, dan rekod pemeriksaan dimensi |
11. Three Contract Clauses That Prevent Common Disputes
Dispute 1 — Thin-Gauge Material Fails a Formability Test.
Cause: The contract copied a nominal r90 or n90 requirement without incorporating the applicable thickness adjustment.
Dispute 2 — Coating Mass Does Not Match Between Supplier and Buyer.
Cause: One party interprets the value as the total coating mass across both surfaces, while the other uses a different unit or measurement convention.
Dispute 3 — Older Stock Develops Forming or Surface-Quality Problems.
Cause: Material age was not controlled, even though the application requires reliable deep drawing and freedom from surface strain marks.
The simplest way to prevent these disputes is to attach the applicable standard requirements and exact acceptance methods to the purchase order rather than relying on a short material designation.
12. Teda Ganghua Support for Aluminized Steel Coil and Tube Projects
Teda Ganghua can support procurement teams sourcing coated steel for exhaust, heating, HVAC, perkakas, and tube-manufacturing applications. For a DX54D+AS project, procurement can be organized around the substrate grade, coating designation, coating mass, ketebalan, lebar, membentuk keperluan, dimensi tiub, proses kimpalan, and inspection documentation.
For projects in which coated steel is purchased in coil form and subsequently converted into welded tubing, it is particularly important to evaluate the flat-product specification together with the downstream tube-manufacturing process. Teda Ganghua can coordinate material requirements for gegelung keluli beraluminium applications and help procurement teams define the required coating grade, dimensi, membentuk keperluan, and documentation before order confirmation.
This approach reduces the risk of receiving material that matches the stated material designation but does not meet the actual requirements of tube production. For engineering and procurement teams, the objective should always be to establish a complete material-to-tube specification rather than simply copying a single grade designation into the purchase order.
13. Final Engineering Takeaways
DX54D+AS combines a low-carbon steel substrate with a hot-dip aluminum-silicon coating and is intended for deep-forming applications. Its value lies in the combination of formability and high-temperature coating performance, but the designation itself does not define the finished tube. [Penukaran Jisim Salutan: Satu Sebelah vs Dua Sebelah Diterangkan]
To ensure reliable procurement, divide the specification into four levels: DX54D substrate → +AS coating → coating mass → finished-tube manufacturing standard. Then add thickness-dependent mechanical requirements, kawalan kimpalan, perlindungan tepi, surface acceptance criteria, material-aging requirements, and inspection documentation. [Kimpalan Tiub Keluli Alumin: Penyingkiran dan Pembaikan Salutan]
[Pencegahan Karat Tiub Keluli Alumin di Kimpalan dan Tepi Potong]
The most important procurement rule is simple: match the complete technical specification, not just the material code.
[Keluli Beralumni lwn Keluli Tahan Karat Feritik untuk Sistem Ekzos]
Soalan yang sering ditanya
Is DX54D+AS a tube grade?
Tidak. It refers to a continuously hot-dip aluminum-silicon-coated flat steel product under the relevant EN standard. Finished aluminized tubes are manufactured from coated flat steel, so the tube standard and manufacturing requirements must be specified separately.
What does +AS mean?
+AS denotes an aluminum-silicon coating, not a pure aluminum coating. The coating chemistry and coating mass must be specified separately from the DX54D substrate grade.
What is AS120?
AS120 is a coating designation indicating a nominal coating mass of 120 g/m² under the applicable EN coating system, generally referring to the combined mass on both surfaces. Its coating mass is approximately comparable to ASTM A463 Type 1 T1-40, but the two designations should not be considered fully equivalent.
Why are thickness corrections important for DX54D?
Deep-forming properties, including elongation, r90, and n90, may be subject to thickness-dependent adjustments. The applicable corrections should be included in the procurement specification so that the supplier and buyer apply the same acceptance criteria.
What is the main issue when converting DX54D+AS into tubing?
The welding and subsequent forming operations must be compatible with the aluminum-silicon coating. The weld zone, cut edges, and heavily formed areas may require specific processing measures and localized protection to maintain the intended service performance.
Can DX54D+AS be used for automotive exhaust systems?
It may be suitable for selected exhaust and high-temperature components when its formability and aluminum-silicon coating performance meet the actual temperature, kakisan, mengimpal, and service-life requirements. The complete operating environment should be evaluated before the material is approved.