- Description
Description
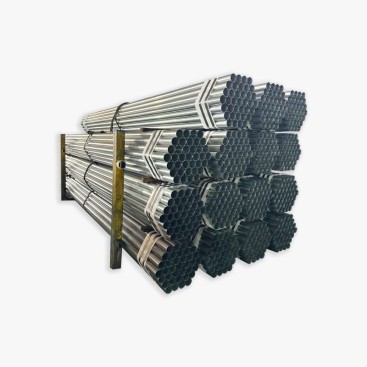
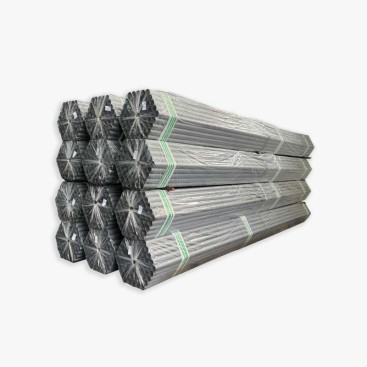
Aluminized Steel Heat Exchanger Tubes: Corrosion and Scale Resistance at 600-900°F for Long-Term Thermal Equipment Performance
Heat exchanger tubes used in boilers, power plants, and industrial heating systems operate under severe conditions, including high temperature oxidation, flue gas corrosion, condensation, and mineral scale formation. Selecting the right tube material directly affects heat transfer efficiency, maintenance frequency, and equipment service life.
Aluminized steel heat exchanger tubes provide a cost-effective solution between traditional carbon steel and higher-cost stainless steel options. Through an aluminum-based protective coating and diffusion layer, these tubes offer improved resistance against oxidation, sulfur-related corrosion, and surface degradation in high-temperature environments.
The Role of Aluminized Steel Tubes in Heat Exchanger Applications
In thermal equipment, tube materials must withstand repeated temperature changes, hot gas exposure, and corrosive combustion products. Aluminized steel tubes are designed to improve the performance of steel substrates by adding an aluminum protective layer.
The aluminum coating reacts with oxygen at elevated temperatures to form a stable aluminum oxide film. This protective layer reduces oxidation damage and helps extend tube service life in applications such as boiler air preheaters and economizer tube bundles.
| Application Area | Operating Challenge | Material Requirement |
|---|---|---|
| Boiler air preheater | Hot flue gas oxidation | High-temperature oxidation resistance |
| Economizer tube bundle | Condensation corrosion | Resistance to acidic moisture |
| Waste heat boiler | Thermal cycling and deposits | Stable surface protection |
Three Protection Mechanisms of Aluminized Coating in Heat Exchangers
1. Protection Against High-Temperature Oxidation
At elevated temperatures, ordinary carbon steel forms iron oxide layers that can continuously grow, crack, and peel away. This repeated oxidation process gradually reduces tube wall thickness.
The aluminum coating creates a protective aluminum oxide layer that slows oxygen diffusion and reduces oxidation-related material loss. This makes aluminized tubes suitable for environments approaching 600-900°F operating conditions.
2. Resistance Against Sulfuric Acid Dew Point Corrosion
Flue gases containing sulfur compounds may generate acidic condensation when temperatures fall below the dew point. This type of corrosion is a common problem in boiler systems.
The aluminized surface provides additional protection between corrosive condensate and the steel substrate, helping reduce corrosion risks in heat recovery equipment.
3. Reduced Scale Formation on Tube Surfaces
The relatively smooth aluminum-based surface can reduce the adhesion of deposits compared with rough oxidized steel surfaces. Lower scale accumulation helps maintain heat transfer efficiency and reduces cleaning requirements.
Aluminized Steel vs Carbon Steel vs Stainless Steel Heat Exchanger Tubes
| Material | Corrosion Resistance | Heat Transfer | Cost Efficiency |
|---|---|---|---|
| Carbon steel tube | Limited protection | Good thermal conductivity | Lowest initial cost |
| Aluminized steel tube | Improved oxidation and corrosion resistance | Maintains steel heat transfer characteristics | Balanced performance and cost |
| 304 stainless steel tube | High corrosion resistance | Moderate thermal conductivity | Higher material investment |
| 316 stainless steel tube | Excellent chloride resistance | Moderate thermal conductivity | Higher lifecycle cost |
Common Failure Modes of Aluminized Heat Exchanger Tubes
Although aluminized tubes provide strong protection, correct design, installation, and operating control remain important. Most failures are related to coating damage rather than normal surface oxidation.
| Failure Type | Cause | Result |
|---|---|---|
| Local coating damage | Mechanical impact or improper handling | Steel substrate exposure |
| Accelerated oxidation | Loss of aluminum protection | Rapid tube wall reduction |
| Thermal cycling stress | Repeated heating and cooling | Potential coating cracking |
Aluminizing Processes for Heat Exchanger Tubes
Two main approaches are commonly used for applying aluminum protection to steel tubes.
Hot-Dip Aluminizing
Hot-dip aluminizing immerses steel tubes into molten aluminum alloy. This process creates a relatively thick coating and diffusion layer, making it suitable for mass production applications.
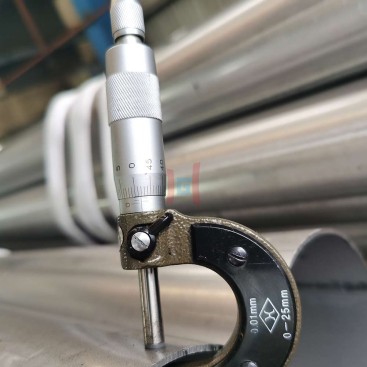
- Typical coating thickness: approximately 25-50μm.
- Suitable for continuous industrial production.
- Provides stable high-temperature protection.
Spraying and Diffusion Treatment
Spraying followed by diffusion treatment is often used for repair applications or customized protection. It allows localized restoration of damaged surfaces.
Typical Purchasing Specifications
| Specification Item | Common Range |
|---|---|
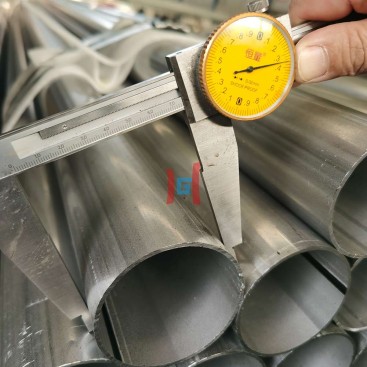
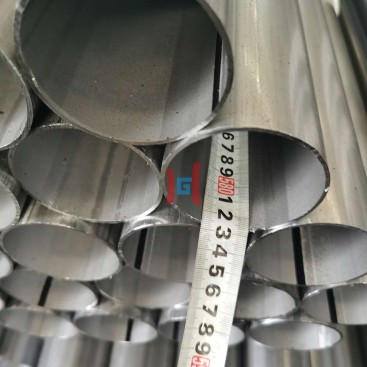
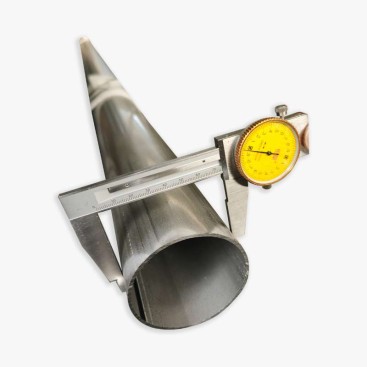
| Outer Diameter | 25-76 mm |
| Wall Thickness | 2-4 mm |
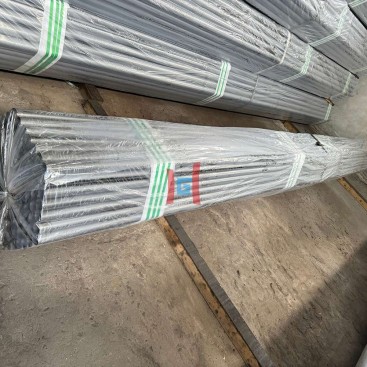
| Tube Length | 6-12 m |
Industrial Applications
- Power plant air preheater systems.
- Waste heat boiler economizer tubes.
- Industrial furnace heat recovery equipment.
- Thermal processing systems exposed to corrosive gases.
Teda Ganghua Aluminized Steel Tube Solutions
Teda Ganghua provides aluminized steel tube solutions for customers requiring improved corrosion resistance, high-temperature performance, and reliable heat exchanger operation. With professional metal processing capabilities, Teda Ganghua supports power generation, industrial heating, and heat recovery equipment manufacturers with customized tube solutions.
For applications requiring durable protection against oxidation and flue gas corrosion, Teda Ganghua offers aluminized steel tubes designed for demanding thermal environments.
FAQ
1. Why are aluminized steel tubes used in heat exchangers?
They provide improved oxidation resistance and corrosion protection compared with ordinary steel while maintaining good cost efficiency.
2. Can aluminized steel tubes operate at 600-900°F temperatures?
Yes. They are commonly selected for high-temperature environments where oxidation resistance is required.
3. Are aluminized tubes better than stainless steel tubes?
Not always. Stainless steel provides higher corrosion resistance, while aluminized steel offers a better balance between performance and investment for many applications.
4. What causes aluminized tube failure?
Most failures occur after coating damage exposes the steel substrate to aggressive oxidation or corrosion conditions.
5. Which industries use aluminized heat exchanger tubes?
Power plants, waste heat recovery systems, boilers, and industrial heating equipment commonly use these tubes.