- Description
Description
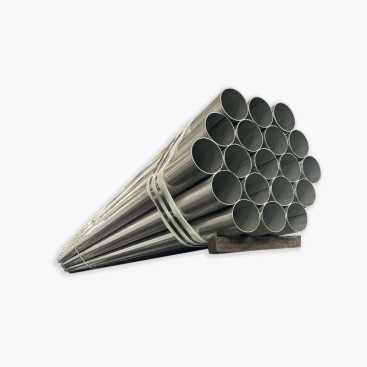
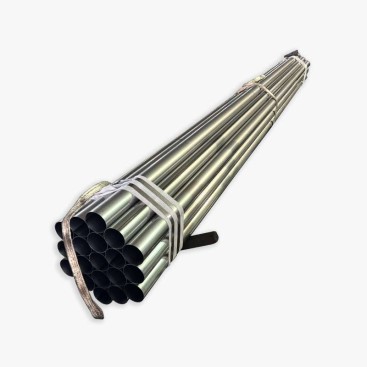
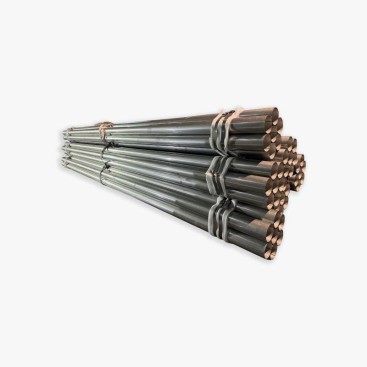
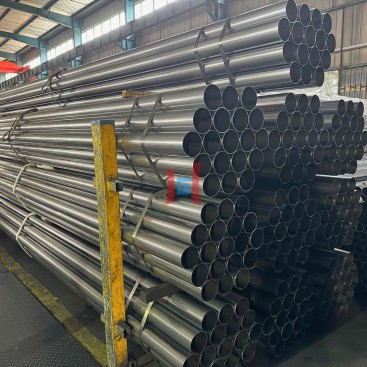
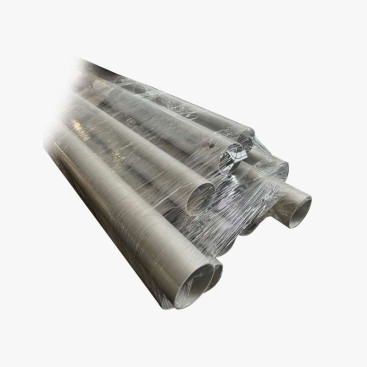
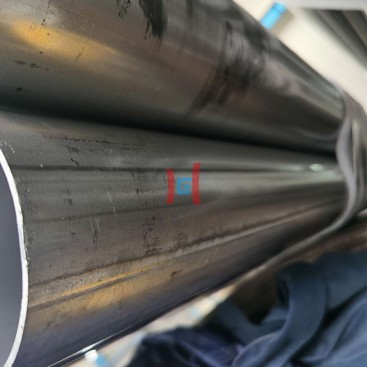
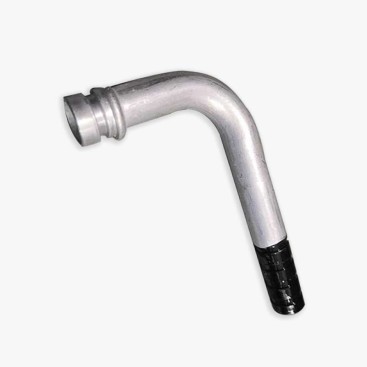
Aluminized Boiler Tubes: Hot Corrosion and Fireside Attack Protection for Long-Life Boiler Systems
Boiler tubes are exposed to some of the most aggressive operating environments in thermal power and industrial heating systems. High-temperature furnace gases, sulfur compounds, molten ash deposits, steam oxidation, and acidic condensation can gradually reduce tube wall thickness and cause unexpected failures.
Traditional carbon steel boiler tubes provide good mechanical strength and cost advantages, but they have limited resistance against severe fireside corrosion. Aluminized boiler tubes provide an upgraded protection solution by combining a steel tube substrate with an aluminum diffusion layer and protective aluminum oxide film.
For many boiler applications, aluminized tubes can extend service life while maintaining a more economical structure compared with higher-alloy materials.
The Three Major Threats to Boiler Tubes
Different sections of a boiler experience different corrosion mechanisms. Understanding the failure environment is essential for selecting the correct tube material.
| Failure Mechanism | Typical Location | Main Cause |
|---|---|---|
| Fireside high-temperature corrosion | Water wall and furnace side | Molten salts, sulfur compounds, ash deposits |
| Steam oxidation | Superheater and reheater tubes | High-temperature steam exposure |
| Flue gas dew point corrosion | Economizer tubes | Acidic condensation from sulfur gases |
How Aluminized Layers Protect Boiler Tubes
The protection mechanism of aluminized boiler tubes comes from two important structures: an aluminum diffusion layer and a stable aluminum oxide surface film.
1. Aluminum Diffusion Layer
During the aluminizing process, aluminum diffuses into the steel surface and forms an iron-aluminum intermetallic layer. This transition zone improves bonding strength and provides additional oxidation resistance.
2. Aluminum Oxide Protective Film
When exposed to high temperatures, aluminum reacts with oxygen to form Al₂O₃. This dense oxide film acts as a barrier against oxygen penetration, sulfur attack, and molten ash corrosion.
Compared with ordinary steel oxidation products, aluminum oxide has better stability under high-temperature conditions and helps slow down metal loss.
Aluminized Boiler Tubes vs Carbon Steel and Alloy Tubes
| Material Type | Advantages | Limitations |
|---|---|---|
| Carbon steel boiler tube (SA-192 / SA-210) | Low cost, good strength, easy fabrication | Limited resistance to hot corrosion |
| Aluminized boiler tube | Improved oxidation and sulfur corrosion resistance | Requires coating quality control |
| Low alloy tube (T11 / T22) | Better high-temperature strength | Higher material cost |
Where Aluminized Boiler Tubes Are Used
Aluminized protection can be applied to different boiler sections depending on the dominant corrosion problem.
| Boiler Section | Operating Condition | Protection Benefit |
|---|---|---|
| Water wall tubes | Direct flame and ash exposure | Reduces fireside corrosion |
| Superheater tubes | High-temperature steam oxidation | Improves oxidation resistance |
| Economizer tubes | Low-temperature acidic gas area | Helps resist dew point corrosion |
Aluminizing vs Weld Overlay vs Thermal Spray Protection
Boiler tube protection can be improved through different surface engineering methods. Each technology has different advantages depending on repair requirements, production scale, and operating conditions.
| Protection Method | Main Feature | Typical Application |
|---|---|---|
| Aluminizing | Metallurgical diffusion protection | New tube manufacturing and upgrades |
| Stainless steel weld overlay | Thick corrosion-resistant layer | Severe furnace wall corrosion repair |
| Thermal spray coating | Flexible surface repair method | Localized maintenance areas |
Economic Advantages of Upgrading Boiler Tubes
Replacing standard carbon steel tubes with aluminized boiler tubes can improve equipment reliability without requiring the same investment level as fully alloyed materials.
- Service life can reach approximately 2-3 times that of standard carbon steel tubes in suitable environments.
- Material upgrade cost is generally lower than switching to high-alloy stainless solutions.
- Reduced shutdown frequency improves boiler availability.
- Longer maintenance intervals reduce replacement labor requirements.
Manufacturing and Specification Considerations
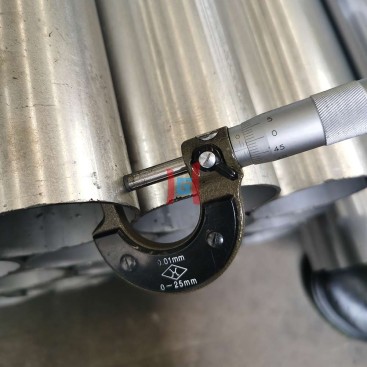
For boiler applications, aluminized tubes are typically produced using qualified boiler tube substrates combined with controlled aluminizing processes. Proper coating thickness, diffusion depth, and welding area protection are important factors affecting performance.
| Specification Item | Typical Requirement |
|---|---|
| Base Tube Standard | ASME boiler tube grades such as SA-210 |
| Coating Method | Controlled aluminizing treatment |
| Weld Area Protection | Post-weld coating repair or aluminizing treatment |
Teda Ganghua Aluminized Boiler Tube Solutions
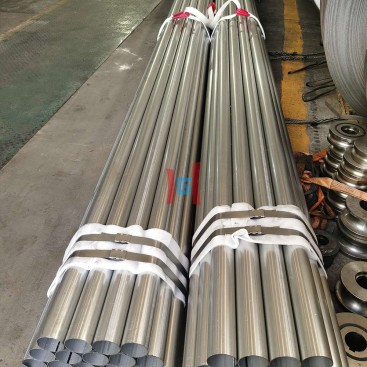
Teda Ganghua provides aluminized steel tube solutions for industrial heating systems, boilers, and thermal equipment manufacturers. Through controlled surface treatment and customized tube processing, Teda Ganghua helps customers improve resistance against oxidation, corrosion, and high-temperature operating challenges.
For boiler systems requiring improved fireside corrosion protection and longer service intervals, Teda Ganghua supplies aluminized steel tubes suitable for demanding thermal applications.
FAQ
1. Why are boiler tubes vulnerable to corrosion?
Boiler tubes face high-temperature gases, sulfur compounds, steam oxidation, and acidic condensation, which can gradually damage the tube surface.
2. How does aluminizing improve boiler tube performance?
The aluminum diffusion layer and Al₂O₃ protective film create a barrier against oxidation, sulfur attack, and high-temperature corrosion.
3. Are aluminized tubes better than alloy boiler tubes?
They are not a replacement for every application, but they provide a cost-effective upgrade where corrosion resistance is needed without extreme temperature requirements.
4. Can existing boiler tubes be repaired with aluminizing?
Yes. Certain repair methods can restore aluminum protection on localized damaged areas depending on site conditions.
5. How long can aluminized boiler tubes last?
Under suitable operating conditions, they can significantly extend service life compared with untreated carbon steel tubes.