- Description
Description
Aluminized Welded Steel Pipe: Sourcing Tips for After-Market Exhaust System Manufacturers
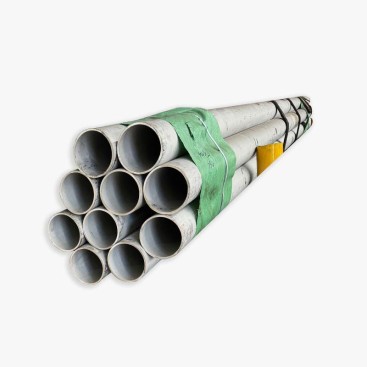
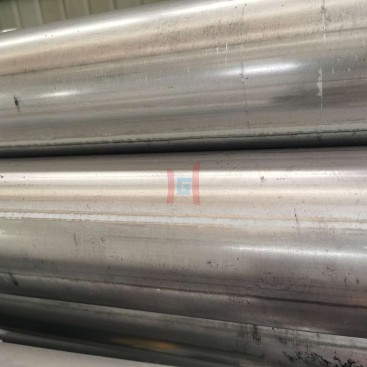
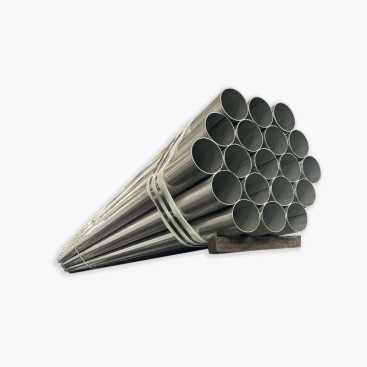
Aluminized welded steel pipe is widely used in the automotive aftermarket exhaust industry due to its balance of cost efficiency, formability, and high-temperature corrosion resistance. For exhaust system manufacturers, especially those producing mandrel-bent tubing systems, correct sourcing is critical to ensure bending quality and coating integrity.
This guide focuses on procurement requirements for aftermarket exhaust system production, including dimensional control, coating durability, and bending compatibility.
1. Why Aluminized Welded Pipe Dominates Aftermarket Exhaust Systems
| Advantage | Impact on Exhaust Manufacturing |
|---|---|
| High cost-performance ratio | Lower cost than stainless steel while maintaining heat resistance |
| Good oxidation resistance | Al-Si coating protects against exhaust gas corrosion |
| Excellent formability | Suitable for mandrel bending and CNC tube forming |
| Lightweight structure | Reduces vehicle exhaust system weight |
2. Critical Sourcing Parameter: OD Tolerance & Wall Accuracy
| Parameter | Recommended Standard | Why It Matters |
|---|---|---|
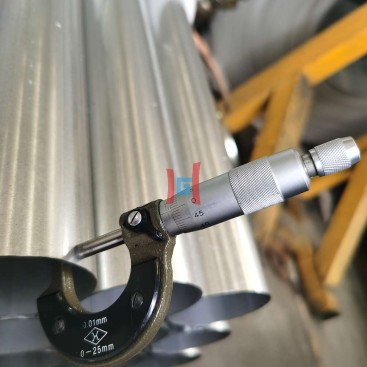
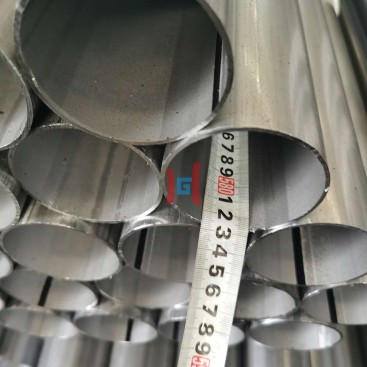
| Outer Diameter (OD) | ±0.10 mm to ±0.25 mm | Ensures compatibility with bending dies and connectors |
| Wall Thickness | ±5–10% | Affects bending strength and exhaust durability |
| Ovality | ≤1.5% | Prevents distortion during mandrel bending |
Poor OD control can lead to bending deformation, cracking, or assembly mismatch in exhaust systems.
3. Mandrel Bending Compatibility Requirements
| Factor | Requirement |
|---|---|
| Material ductility | Low-carbon steel base for smooth deformation |
| Coating adhesion | Al-Si layer must remain intact after bending |
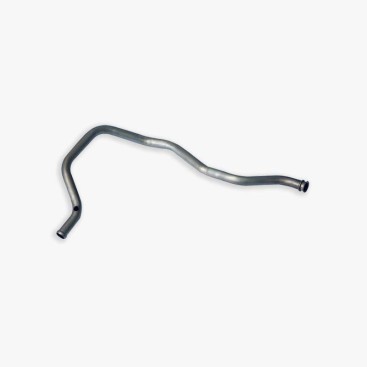
| Bend radius (R/D ratio) | Typically 1.5D–2.5D for exhaust tubing systems |
| Surface condition | No micro-cracks or coating peeling allowed |
High-quality aluminized pipe should maintain coating integrity after cold forming and mandrel bending.
4. Coating Integrity After Bending
| Potential Issue | Cause | Solution |
|---|---|---|
| Micro-cracking of coating | Excessive bending stress | Use optimized Al-Si coating (9–10% Si) |
| Coating flaking | Poor adhesion or surface contamination | Improve pre-treatment and cleaning |
| Seam area weakness | ERW weld zone stress concentration | Post-weld normalization and controlled cooling |
5. Typical Exhaust System Applications
| Component | Function |
|---|---|
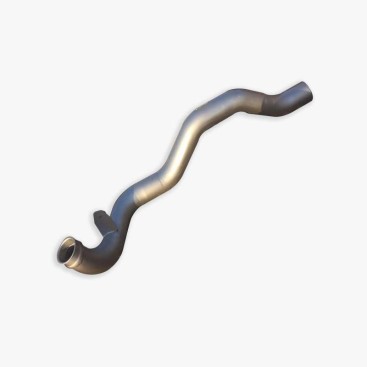
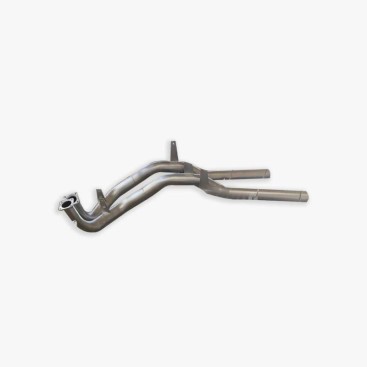
| Exhaust pipes | Main gas flow channel |
| Mid-pipes | Connect engine to muffler system |
| Muffler tubing | Noise reduction system structure |
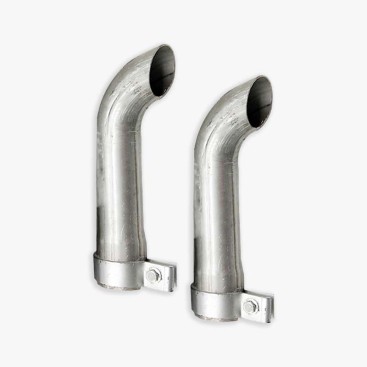
| Tailpipes | Final exhaust outlet section |
6. Procurement Checklist for Buyers
| Item | What to Verify |
|---|---|
| Material certification | Ensure ASTM A463 / EN 10346 compliance |
| Coating specification | Verify Al-Si coating weight (AS80 / AS120 / AS150) |
| Dimensional inspection | Check OD, wall thickness, and ovality reports |
| Bending test | Mandrel bend test without cracking or peeling |
| Surface quality | No pinholes, blisters, or coating discontinuity |
7. Why Buyers Choose Teda Ganghua
At Teda Ganghua, we supply aluminized welded steel pipes specifically optimized for exhaust system manufacturers, ensuring stable OD tolerance, uniform Al-Si coating, and reliable mandrel bending performance.
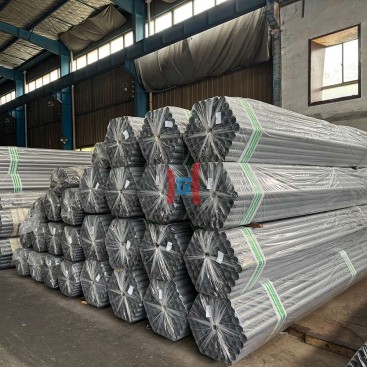
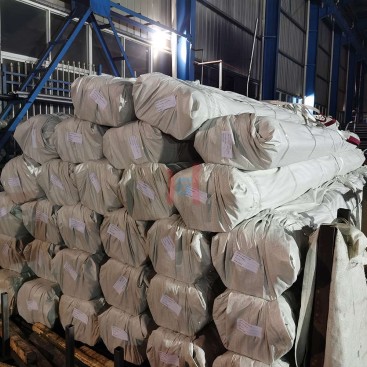
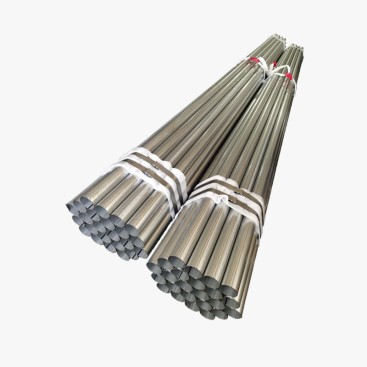
We provide OEM cutting, bending preparation, and export-ready packaging for global automotive aftermarket customers.
Explore our aluminized steel tube products here:
Aluminized Steel Tube Products
Conclusion
For aftermarket exhaust manufacturers, aluminized welded steel pipe offers the best balance between cost and performance. However, sourcing must focus on OD precision, coating adhesion, and bending compatibility to ensure long-term durability in real-world exhaust systems.