- Description
Description
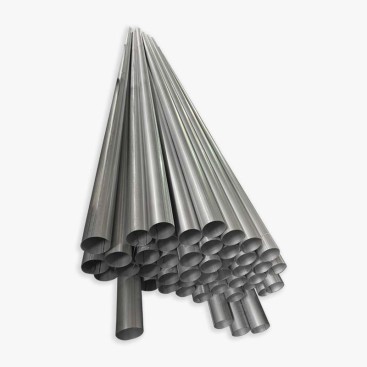
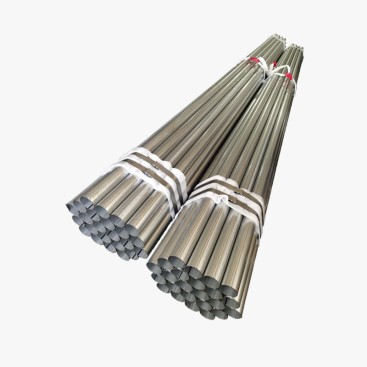
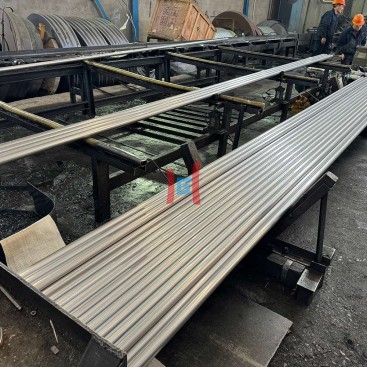
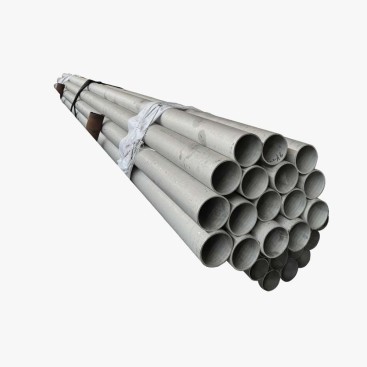
Hot-dip aluminized steel tube is produced by immersing a prepared steel tube in a molten aluminum-silicon bath. The process creates a metallurgically bonded coating that can provide strong resistance to oxidation, corrosion, and elevated-temperature exposure. For tube products, process control is especially important because both the outside surface and, where specified, the internal surface must be properly covered.
How the Hot-Dip Process Works
In a typical process, the steel tube is cleaned and activated before entering a molten aluminum-based bath. Common process stages include degreasing, pickling, fluxing or another suitable surface-conditioning treatment, immersion, withdrawal, cooling, and finishing.
Aluminum-silicon bath compositions are widely used for aluminized steel because silicon helps control the intermetallic reaction between the coating and the steel substrate. The exact bath chemistry and process window depend on the applicable product specification and production route.
Process principle
Surface preparation → molten Al-Si immersion → interfacial reaction → withdrawal → cooling → inspection
Typical Process Stages
| Stage | Main purpose | Quality concern |
|---|---|---|
| Degreasing | Remove oil and organic contamination | Residual contamination can prevent proper wetting |
| Pickling | Remove oxides and scale | Surface activation must be controlled |
| Fluxing / activation | Promote molten-metal wetting | Poor treatment can cause bare spots |
| Immersion | Form the aluminum-based coating | Bath temperature and immersion time are critical |
| Withdrawal | Control coating drainage and thickness | Withdrawal speed affects surface appearance and buildup |
| Cooling | Solidify the coating | Cooling conditions can influence surface condition |
| Finishing and inspection | Meet dimensional and coating requirements | Thickness, uniformity, adhesion, and coverage are checked |
Molten Bath Temperature: Why the Process Window Matters
A molten Al-Si bath is typically maintained at a temperature above the melting point of the coating alloy. Depending on the alloy and process specification, a working range around 660–700°C may be encountered.
The bath should not simply be operated at the highest possible temperature. Excessive thermal exposure can accelerate interfacial reactions, while insufficient temperature can affect wetting and coating formation. A stable process window is therefore more important than a single temperature value.
Immersion Time and Withdrawal Speed
Immersion time affects the interaction between the molten coating and steel substrate. Longer thermal exposure can increase the intermetallic reaction at the interface. If this layer becomes excessively thick, it may become more brittle and influence forming performance.
Withdrawal speed also affects how molten metal drains from the tube surface. Process engineers therefore control immersion and withdrawal as a combined operation rather than treating coating thickness as an isolated variable.
| Parameter | If poorly controlled | Quality objective |
|---|---|---|
| Bath temperature | Poor wetting or excessive reaction | Stable coating formation |
| Immersion time | Non-uniform or excessive intermetallic growth | Controlled interface |
| Withdrawal speed | Uneven drainage and surface buildup | Consistent coating thickness |
| Surface preparation | Bare spots or weak adhesion | Clean, active substrate |
Tube Coating: Inside and Outside Coverage
Steel tubes create an additional challenge that flat products do not have: the internal surface may also require protection. For hollow sections, molten metal must contact the internal wall sufficiently to produce the specified coating coverage.
Internal coating quality can be affected by tube geometry, drainage, trapped gases, surface preparation, and production equipment. A tube that looks satisfactory externally should not automatically be assumed to have complete internal coverage.
For hollow tube products, verify:
- Outside coating continuity
- Inside-wall coating coverage
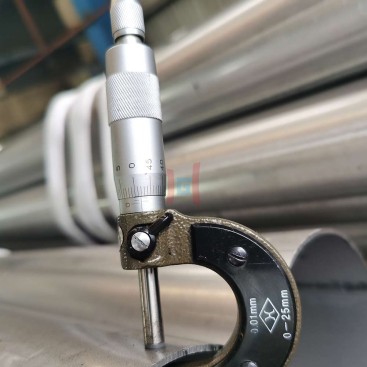
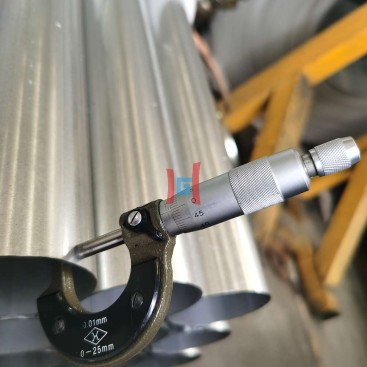
- Coating thickness at representative locations
- Coating adhesion after forming
- End-area condition after cutting
Common Coating Defects
Bare or Uncoated Areas
Local bare spots can result from inadequate cleaning, insufficient surface activation, poor wetting, contamination, or unsuitable process conditions. These areas should be identified during visual and coating inspections.
Flow Marks and Surface Buildup
Uneven drainage during withdrawal can create visible flow marks or local buildup. Tube geometry and withdrawal conditions can make this effect more noticeable.
Poor Adhesion
Poor adhesion can be associated with surface contamination, inadequate preparation, or an unsuitable interfacial structure. Adhesion should be verified using the test method required by the applicable specification.
Excessive Intermetallic Growth
A metallurgical interface is necessary for strong bonding, but excessive intermetallic growth can increase brittleness. Bath temperature, immersion time, alloy chemistry, and steel composition all influence the interface.
Continuous vs Batch Hot-Dip Processing
The production route can be continuous or batch-based. Continuous processing is often suited to standardized tube dimensions and high-volume production, while batch processing can provide greater flexibility for certain product sizes and order requirements.
| Production route | Strength | Main consideration |
|---|---|---|
| Continuous | High production efficiency and process consistency | Best suited to established product ranges |
| Batch | Greater flexibility for selected dimensions | Process uniformity must be controlled between batches |
Hot-Dip vs Electroplated Aluminum
Hot-dip coating and electroplating use fundamentally different mechanisms. In hot-dip processing, the molten coating reacts with the steel surface and can form an intermetallic transition zone. This creates a metallurgical bond rather than relying only on mechanical adhesion.
Electroplating can provide a controlled, relatively thin metallic deposit and is useful for applications where precise surface deposition is required. However, it does not reproduce the same hot-dip interfacial structure or process characteristics.
| Feature | Hot-dip coating | Electroplated coating |
|---|---|---|
| Formation mechanism | Molten-metal immersion and interfacial reaction | Electrochemical deposition |
| Interface | Metallurgically bonded transition zone | Deposited coating interface |
| Coating thickness | Can support relatively substantial protective layers | Typically selected for controlled thinner deposits |
| High-temperature application | Strong candidate for many thermal applications | Depends strongly on coating metal and service conditions |
What Should a Coating Inspection Report Include?
A useful quality report should connect the finished tube to its material specification and coating requirements. The exact inspection plan depends on the purchase standard, but a practical report may include the following information:
The values and test methods in an actual inspection report must be based on the applicable product standard and purchase specification. The sample above is a reporting framework, not a certification document.
Source Hot-Dip Aluminized Steel Tube
Teda Ganghua supports sourcing of aluminized steel tubes for exhaust components, thermal equipment, industrial applications, and fabricated tube assemblies. Buyers can review the Aluminized Steel Tubes range and provide tube dimensions, substrate grade, coating requirements, internal coverage requirements, and service temperature.
For projects involving bending, welding, or internal-fluid service, the inquiry should also state the forming method, post-weld protection requirements, operating environment, and required inspection documentation. This helps ensure that coating quality is evaluated together with the finished tube’s actual application.
FAQ
What temperature is used for hot-dip aluminizing?
An aluminum-based molten bath is typically operated above the melting point of the coating alloy. A process range around 660–700°C may be encountered, but the correct temperature depends on bath chemistry, equipment, substrate, and the governing specification.
Does hot-dip coating cover the inside of a steel tube?
It can, when the production process is designed and specified for internal coating. Internal coverage should be explicitly included in the purchase requirement and verified during inspection.
Why is surface preparation important before immersion?
Oil, scale, oxides, and other contaminants can interfere with molten-metal wetting and coating formation. Proper cleaning and surface activation are therefore essential for consistent coverage and adhesion.
What causes bare spots on aluminized tubes?
Possible causes include inadequate cleaning, poor fluxing or activation, contamination, insufficient wetting, or unstable process conditions. Inspection should determine whether the defect is local or related to a broader process issue.
Is hot-dip coating stronger than electroplated aluminum?
The two processes create different coating structures. Hot-dip aluminizing can produce a metallurgically bonded interfacial layer and a relatively substantial protective coating, while electroplating is based on electrochemical deposition. The better option depends on the required thickness, adhesion, temperature, geometry, and service environment.