- Description
Description
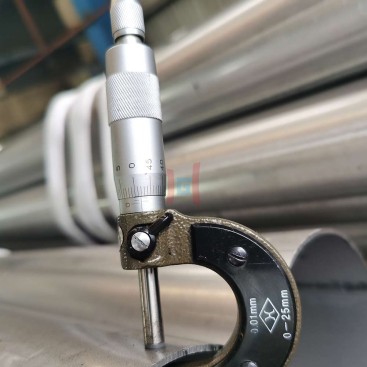
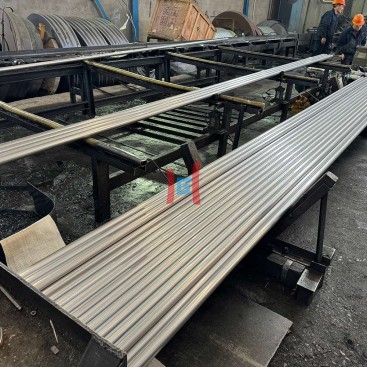
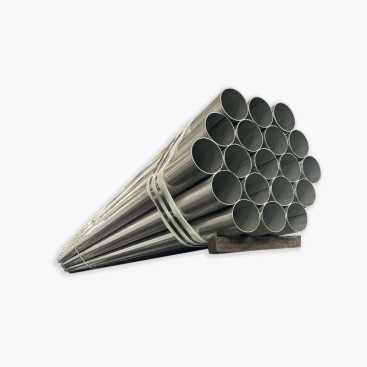
Aluminized low carbon steel tube is designed around one simple advantage: a low-carbon steel substrate provides excellent formability, while an aluminum-based coating improves resistance to oxidation, corrosion, and heat. This combination makes it useful for bent tubes, exhaust components, heat-transfer equipment, and other fabricated parts where forming performance is important.
What Makes Low-Carbon Steel a Good Tube Substrate?
Low-carbon steel contains relatively little carbon, which generally gives it good ductility and weldability. Compared with higher-carbon substrates, it can be easier to bend, flare, expand, and form without excessive cracking.
The aluminum-based coating adds surface protection without requiring the entire tube to be manufactured from a highly alloyed material. The result is a tube system that balances formability, fabrication, heat resistance, and corrosion protection.
The basic design
Low-carbon steel substrate → forming and welding
Aluminum-based coating → oxidation and corrosion protection
Why Formability Matters
Many tubular components are not installed as straight sections. They may need to be bent into complex shapes, expanded at the ends, flared for connections, or formed around fixtures. In these cases, substrate ductility becomes an important selection factor.
A low-carbon substrate can provide a useful balance between strength and ductility. This is particularly valuable for exhaust bends, heat-transfer tubes, and fabricated mechanical components where dimensional accuracy must be maintained after forming.
Typical Applications
Exhaust Bent Tubes
Exhaust systems often require curved sections rather than simple straight tubes. Low-carbon steel supports bending operations, while the aluminum-rich surface helps protect the tube against oxidation and corrosion during service.
The coating specification should be matched to the actual exhaust temperature. Peak temperature, continuous temperature, condensate, road salts, and thermal cycling can all affect service life.
Heat-Transfer Tubes
Selected heat exchangers and thermal equipment can use coated low-carbon tubes when surface oxidation and atmospheric corrosion are concerns. Tube dimensions and coating characteristics should be selected according to the heat-transfer and operating requirements.
Mechanical Tubes
Mechanical components that require bending or formed ends can also benefit from the ductile substrate. The final selection should consider load requirements as well as coating integrity after fabrication.
Bending: Protect the Coating During Forming
The substrate may tolerate a tight bend while the coating experiences a different level of deformation. Excessive tensile strain on the outside radius can lead to coating cracking, while severe compression can affect the inner radius.
For demanding bends, a mandrel bending process can help control tube deformation and maintain a more consistent cross-section. Bend radius, tooling, tube wall thickness, coating characteristics, and forming speed should be evaluated together.
| Forming factor | Potential issue | Recommended control |
|---|---|---|
| Small bend radius | High surface strain | Use suitable tooling and qualify the bend radius |
| Tube flattening | Loss of dimensional accuracy | Consider mandrel or supported bending |
| Coating cracking | Reduced surface protection | Control deformation and inspect the formed area |
| Repeated forming | Cumulative coating damage | Minimize unnecessary forming passes |
Welding and Post-Weld Protection
Low-carbon steel is generally well suited to conventional welding processes. However, welding introduces a separate issue: the heat generated at the joint can burn away, melt, or otherwise alter the protective coating around the weld area.
After welding, the exposed steel should be evaluated and protected according to the applicable coating specification. Depending on the application, this may involve an approved repair coating or another suitable corrosion-protection method.
Welding reminder
Good weldability of the low-carbon substrate does not mean that the original surface protection remains unchanged after welding. The weld zone and heat-affected coating area should be included in the corrosion-protection plan.
Thin-Wall Tube for Lightweight Applications
Thin-wall products in the approximate range of 0.8–2.0 mm can be considered for lightweight structures and formed components. Reducing wall thickness can lower weight and improve material efficiency, but it also reduces structural margin and can make forming more sensitive.
| Wall thickness | General positioning | Main consideration |
|---|---|---|
| 0.8–1.0 mm | Lightweight formed parts | Careful control of bending and handling |
| 1.0–1.5 mm | General fabricated tubing | Balance weight and structural requirements |
| 1.5–2.0 mm | Higher-duty lightweight components | Check load, bend radius, and fabrication method |
These thicknesses are practical reference ranges, not universal limits. The required wall thickness should be calculated from pressure, structural load, temperature, corrosion allowance, and applicable standards.
Low Carbon vs Medium Carbon: Which Substrate Should You Choose?
The decision is mainly a balance between formability and strength. When a tube must undergo significant bending, flaring, or forming, a low-carbon substrate is often attractive. When higher mechanical strength is required, a stronger substrate may be considered, but fabrication and coating adhesion must then be evaluated more carefully.
| Factor | Low-carbon substrate | Medium-carbon substrate |
|---|---|---|
| Formability | Excellent choice for many forming operations | More limited as carbon content increases |
| Bending | Generally favorable | Requires closer process control |
| Weldability | Generally good | May require additional procedure controls |
| Strength potential | Moderate, grade dependent | Higher potential |
| Best priority | Forming and fabrication | Strength and load capacity |
Specification Checklist
A purchase specification should define more than the phrase “low carbon.” The following information helps ensure that the tube and fabrication process are properly matched:
- Steel grade and governing standard
- Outside diameter
- Wall thickness
- Tube length
- Aluminum-based coating system
- Coating mass or thickness
- Bend radius and bending method
- Flaring, expansion, or end-forming requirements
- Welding process and post-weld coating requirements
- Operating temperature
- Corrosion environment
- Inspection and certification requirements
Source Low-Carbon Coated Tube with Forming Support
Teda Ganghua can support sourcing requirements for coated steel tubes used in exhaust systems, thermal equipment, mechanical components, and formed assemblies. Buyers can review the Aluminized Steel Tubes range and provide the required grade, dimensions, coating specification, bend radius, and application conditions.
For projects requiring formed tube components, bending requirements can be included with the inquiry so that the substrate, wall thickness, coating integrity, and fabrication process can be considered together.
FAQ
What is aluminized low carbon steel tube?
It is a low-carbon steel tube protected by an aluminum-based coating. The low-carbon substrate provides good formability and weldability, while the coating improves resistance to oxidation, corrosion, and elevated temperature.
Is low-carbon steel good for tube bending?
Yes. Its relatively high ductility makes it suitable for many bending and forming operations. The bend radius, tooling, wall thickness, and coating behavior must still be evaluated for the specific tube.
Can the coating crack during bending?
It can if deformation exceeds the coating’s forming capability. Mandrel bending, suitable tooling, controlled bend radius, and proper process qualification can help reduce coating damage.
What happens to the coating during welding?
The heat from welding can remove or alter the protective coating around the weld. The affected area should therefore be inspected and protected using a suitable post-weld repair or corrosion-control method.
When should low carbon be chosen over a stronger steel substrate?
Low carbon is generally attractive when bending, flaring, welding, and other forming operations are important. A stronger substrate may be preferable when load capacity is the main requirement, provided that forming and coating adhesion can be maintained.