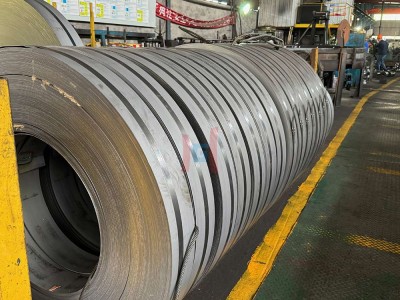
ASTM A463 Спецификация стального листа с алюминиевым покрытием и руководство по покрытию
При покупке стального листа с алюминиевым покрытием или выборе труб с алюминиевым покрытием, понимание применимых требований ASTM имеет важное значение для выбора материала, manufacturing control, and quality inspection. The standard distinguishes between coating composition, coating mass, substrate properties, and product form. One of the most important points for procurement engineers is that a specification for coated flat steel does not automatically establish the dimensional and performance requirements of a finished tube.
For international buyers, производители, and procurement managers, understanding the relationship between coating designations, substrate grades, and tubing specifications helps prevent incorrect material substitutions, coating-weight disputes, and disagreements during final inspection. The following guide explains the standard’s scope, coating classifications, designation system, conversion methods, and practical purchasing requirements. [Руководство по спецификациям алюминизированной стали для листовой рулонной стали и труб]
1. What Does ASTM A463 Cover?
ASTM A463/A463M is officially titled Standard Specification for Steel Sheet, Aluminum-Coated, by the Hot-Dip Process. It covers aluminum-coated steel sheet supplied in coils and cut lengths, with two types of aluminum coating applied through a hot-dip process.
The specification establishes requirements relating to the aluminum coating, base metal, coating mass, and applicable testing procedures. It is primarily intended for flat steel products rather than finished tubular products. [ASTM A463 и ASTM A787 Стандарты стальных труб с алюминиевым покрытием]
Important specification distinction
A463 applies to aluminum-coated steel sheet and strip, not directly to finished steel tubing. For electric-resistance-welded metallic-coated carbon steel mechanical tubing, ASTM A787/A787M provides the relevant product specification. The two standards address different manufacturing and inspection stages.
1.1 Understanding the Three Main Elements
| Элемент | Technical meaning | Procurement significance |
|---|---|---|
| Steel sheet | Flat steel supplied in coils or cut lengths | Defines the product form |
| Aluminum coating | Aluminum or aluminum-silicon coating | Defines coating composition and properties |
| Hot-dip process | Coating applied through immersion in a molten metal bath | Defines the coating manufacturing process |
1.2 What the Standard Does Not Guarantee
Although the specification establishes important material requirements, it should not be interpreted as a complete engineering specification for every finished component.
- Finished tube diameter, ovality, and wall-thickness tolerances.
- Weld seam integrity and mechanical performance after tube manufacturing.
- Guaranteed salt-spray exposure hours for a particular application.
- A universal maximum operating temperature.
- Coating continuity after bending, сварка, expanding, or other fabrication operations.
Например, specifying a particular aluminum coating designation does not automatically guarantee satisfactory performance at 700°C. Actual service life depends on temperature, продолжительность воздействия, термоциклирование, corrosive gases, and mechanical damage.
2. Understanding the Four Parts of an Aluminum Coating Designation
A complete material designation communicates more than the presence of an aluminum coating. Buyers should identify the standard edition, тип покрытия, обозначение покрытия, and substrate grade before confirming an order. [CS против DDS против алюминизированной стали EDDS: Руководство по глубокой вытяжке T1-40]
Consider the following illustrative designation:
Illustrative designation for aluminum-coated steel sheet
| Designation part | Пример | Meaning |
|---|---|---|
| Стандартный | A463 | Applicable product specification |
| Тип покрытия | Т1 | Тип 1 aluminum-silicon coating |
| Coating designation | 40 | 0.40 oz/ft² nominal designation basis, both sides combined |
| Substrate grade | CS | Товарная сталь |
2.1 Why Substrate Identification Matters
The coating protects the steel surface, but the underlying steel determines much of the material’s forming behavior and mechanical performance.
Depending on the applicable edition and ordering requirements, substrate classifications may include commercial steel, forming steel, drawing-quality steel, and structural or high-strength low-alloy steel categories.
These categories should not be treated as interchangeable. A material suitable for simple bending may not provide the drawability required for a deep-drawn component. Similarly, a structural grade selected for strength may not be suitable for complicated forming operations.
Procurement recommendation
Do not purchase material based only on a coating designation. Confirm the substrate grade, толщина, ширина, forming requirements, and mechanical properties in the purchase specification.
3. What Does T1-40 Mean? Understanding Coating Weight
One of the most common misunderstandings when purchasing aluminum-coated steel is the interpretation of the number in a coating designation.
In the conventional inch-pound designation T1-40, the number 40 represents a nominal coating designation of 0.40 oz/ft², with the coating mass calculated for both sides combined. It does not represent a coating thickness of 0.40 mm or a coating mass of 40 г/м².
3.1 Coating Weight Conversion
The basic conversion relationship is:
1 oz/ft² ≈ 305.15 г/м²
Coating mass conversion based on the same measurement area basis
For the commonly referenced Type 1 coating designations, the following table provides approximate conversions. These figures are nominal designation equivalents, not a replacement for the applicable standard’s acceptance limits.
| Coating designation | Масса покрытия (oz/ft²) | Приблизительно. combined mass (г/м²) | Приблизительно. per side (г/м²) |
|---|---|---|---|
| Т1-13 | 0.13 | 40 | 20 |
| Т1-25 | 0.25 | 76 | 38 |
| Т1-40 | 0.40 | 122 | 61 |
| T1-60* | 0.60 | 183 | 91.5 |
| T2-65 | 0.65 | 198 | 99 |
*T1-60 is included as a commonly encountered commercial designation, not as a universal designation required by every edition. Actual coating designations and minimum acceptance values must be checked against the specified edition and product documentation. Тип 2 designations also vary; T2-65 is a recognized designation. [T1-40 Aluminized Steel Coating Weight and ASTM A463 Guide]
3.2 Why Single-Side and Both-Sides Measurements Must Be Distinguished
Coating inspection reports may express results as a combined value for both surfaces or as an individual surface measurement. Confusing these reporting methods can lead to incorrect acceptance decisions.
Например, a nominal combined coating mass of approximately 122 g/m² corresponds to an average of approximately 61 g/m² per side when the coating is evenly distributed.
Однако, the actual coating distribution may not be perfectly symmetrical. Поэтому, the individual-side result should not automatically be assumed to equal exactly half of the combined measurement. [T1-13 vs T1-25 vs T1-40 vs T1-60 Aluminized Steel Coating]
When preparing an order, clearly specify:
- Whether coating mass refers to one surface or both surfaces combined.
- The required coating designation.
- The applicable test method and sampling requirements.
- The minimum acceptance value for the relevant test.
- Whether the inspection report must provide individual-side measurements.
4. Тип 1 против. Тип 2: Aluminum-Silicon Coating or Pure Aluminum Coating?
The two coating types serve different engineering purposes. Their differences relate primarily to coating chemistry, high-temperature behavior, защита от коррозии, and fabrication conditions.
[Тип 1 против типа 2 Aluminized Steel Coating Differences]
| Сравнение | Тип 1 | Тип 2 |
|---|---|---|
| Coating composition | Алюминий-кремниевый сплав | Commercially pure aluminum |
| Типичный состав | Примерно 91% алюминий и 9% кремний | Predominantly aluminum |
| High-temperature behavior | Generally better resistance to coating degradation at elevated temperatures | Generally less suitable for prolonged high-temperature exposure |
| Защита от коррозии | Хорошая устойчивость к атмосферной коррозии | Хорошая устойчивость к атмосферной коррозии |
| Типичные применения | Компоненты выхлопной системы, тепловые экраны, отопительное оборудование | Building components, корпуса приборов, general corrosion-resistant applications |
4.1 Why Silicon Improves High-Temperature Performance
During elevated-temperature exposure, iron and aluminum can diffuse across the interface between the steel substrate and the coating. This reaction produces iron-aluminum intermetallic compounds.
As these compounds develop and grow, they gradually consume the original aluminum-rich coating. Excessive intermetallic growth can reduce coating ductility and compromise its protective function.
Silicon in the Type 1 coating helps control the growth of the iron-aluminum intermetallic layer. This improves the coating’s ability to retain useful protective properties during elevated-temperature service. [Iron-Aluminum Interdiffusion in Aluminized Steel: High-Temperature Coating Degradation]
Typical degradation symptoms may include surface discoloration, increased brittleness, powdering, and localized exposure of the underlying steel.
4.2 Does Type 1 Guarantee a 700°C Operating Temperature?
Нет. A coating designation does not establish a universal service-temperature guarantee. [Значение R и размер зерна в стали для глубокой вытяжки: Руководство по формованию]
Тип 1 aluminum-silicon coated steel is commonly considered for certain applications involving temperatures around the 700°C range. Однако, the actual suitability depends on several operating conditions:
- Continuous operating temperature and exposure duration.
- Frequency and severity of thermal cycling.
- Presence of sulfur, chlorine, and other aggressive substances.
- Mechanical abrasion and vibration during operation.
- Steel substrate chemistry and component thickness.
Engineers should evaluate the complete service environment rather than selecting a coating solely from a nominal temperature figure.
Selection principle
Тип 1 is generally preferred when elevated-temperature coating stability is a major requirement. Тип 2 can be evaluated for applications where aluminum-rich corrosion protection is more important than prolonged high-temperature performance.
5. ASTM A463 vs. ASTM A787: What Is the Difference?
This distinction is particularly important for buyers searching for aluminum-coated steel tubing.
The two specifications address different product forms and manufacturing stages. One concerns the coated flat steel material, while the other covers finished electric-resistance-welded mechanical tubing made from metallic-coated steel sheet or coated after welding, depending on the specified product type.
| Сравнение | A463/A463M | A787/A787M |
|---|---|---|
| Product form | Steel sheet and coils | ERW mechanical tubing |
| Main purpose | Aluminum-coated flat steel requirements | Finished metallic-coated tubing requirements |
| Relevant properties | Покрытие, substrate, coating mass, bend performance | Dimensions, wall tolerances, механические свойства, and applicable coating requirements |
| Manufacturing stage | Flat steel production | Tube production |
| Typical users | Steel processors and tube manufacturers | Tube manufacturers and industrial buyers |
5.1 The Manufacturing Relationship
For tubing manufactured from pre-coated flat steel, the production sequence generally follows this route:
Aluminum-Coated Steel Coil
Flat steel material inspected against the applicable sheet specification
Slitting and Strip Preparation
Coil processing and dimensional preparation
Roll Forming and ERW Welding
Formation of the tubular section and longitudinal welding
Finished Metallic-Coated Mechanical Tube
Inspection against the applicable tubing specification and purchase requirements
When pre-coated material is used, forming and welding may affect the coating around the tube seam and other processed areas. Поэтому, conformity of the original steel strip does not automatically demonstrate conformity of every finished tube characteristic.
5.2 What Should Be Written in a Tubing Purchase Order?
For a finished tube, buyers should identify the applicable tubing specification and separately clarify the coating requirements.
- Tube manufacturing method, such as electric-resistance welding.
- Outside diameter and wall thickness.
- Tube length and dimensional tolerances.
- Steel grade and chemical requirements.
- Coating type and coating mass requirements.
- Weld seam inspection and acceptance requirements.
- Additional bending, expanding, or leak-testing requirements where applicable.
For a broader selection of finished products and processing options, procurement managers can explore aluminized steel tubes and compare the required dimensions, характеристики покрытия, and intended service conditions.
6. Comparing ASTM, В, ОН, and Chinese Coating Specifications
International steel procurement frequently involves specifications from different national and regional standards systems. Although certain coating designations appear numerically similar, their chemistry, substrate classifications, and testing requirements may differ.
| Standard system | Common designation format | Main consideration |
|---|---|---|
| АСТМ | Тип 1 / Тип 2 and coating designations | Тип покрытия, mass, and substrate requirements |
| В 10346 | DX51D+АС, DX52D+АС, DX53D+AS | Steel grade and aluminum-silicon coating designation |
| ОН G3314 | SA1C, SA1D, SA1E | Japanese aluminized steel classification |
| ГБ/Т | Applicable substrate and coating designation | National material and coating requirements |
6.1 Is T1-40 Equivalent to AS120?
In terms of approximate combined coating mass, the two designations are close:
- Т1-40: approximately 122 g/m² combined coating mass.
- АС120: nominally 120 g/m² under the relevant EN designation.
Однако, similar coating mass does not establish full technical equivalence.
Three important factors must be checked before approving a substitution:
- Coating chemistry: The coating composition and applicable manufacturing requirements must be compared.
- Substrate properties: Commercial steel, drawing-quality steel, and other grades do not necessarily have direct equivalents across standards.
- Inspection requirements: Масса покрытия, механические свойства, bend performance, and sampling methods must be aligned.
For this reason, material substitutions should be approved through a technical comparison rather than a simple numerical conversion.
7. Inspection and Quality Acceptance Requirements
Correct material identification is only the first step. A complete quality-control process should confirm that the delivered material meets the agreed requirements and remains suitable for the intended manufacturing process.
| Inspection item | Inspection method | Acceptance consideration |
|---|---|---|
| Масса покрытия | Gravimetric testing or an applicable approved method | Specified coating designation and test limits |
| Coating adhesion | Applicable bending or forming tests | No unacceptable coating separation |
| Base metal properties | Tensile testing and applicable material analysis | Compliance with the ordered substrate grade |
| Dimensions | Толщина, ширина, длина, and flatness measurements | Applicable product tolerances |
| Состояние поверхности | Visual inspection | Agreed surface quality and treatment condition |
| Finished tube quality | Dimensional, сваривать, and additional application-specific testing | Applicable tubing specification and purchase agreement |
7.1 Why Coating Mass Reports Need Clear Units
A test report stating a coating mass of 61 g/m² is incomplete if it does not identify whether the result represents one side or both sides combined.
For reliable acceptance, the report should identify the test method, sample location, measurement basis, and actual measured result. The buyer should compare the result with the applicable standard edition rather than relying on an assumed conversion.
7.2 Why Coating Adhesion Matters During Fabrication
Aluminum-coated steel may undergo slitting, изгиб, профилирование валков, сварка, and other fabrication operations. These processes can introduce local deformation and mechanical stress.
Inspection should therefore consider the material’s intended processing route. A coating that performs well on an unprocessed flat sheet may behave differently around a formed edge or welded seam.
8. How to Prepare a Complete Purchase Specification
For international buyers, an effective purchase specification should remove ambiguity before production begins. Simply writing a material designation without dimensions, coating details, or inspection requirements may leave important technical decisions unresolved.
The following checklist can be used when preparing an inquiry or purchase order:
Aluminum-Coated Steel Procurement Checklist
- Standard and edition: Specify the applicable standard number and revision year.
- Тип покрытия: Identify Type 1 или Введите 2.
- Coating designation: Specify the required designation and coating mass acceptance limits.
- Substrate grade: Select the grade according to strength and forming requirements.
- Dimensions: Provide thickness, ширина, coil weight, or cut length.
- Surface treatment: Identify whether oiling, passivation, or another treatment is required.
- Coating adhesion: Specify the applicable test and acceptance criteria.
- Mechanical properties: Define tensile requirements and sampling direction where applicable.
- Surface quality: Establish acceptable surface conditions and defect limits.
- Packaging: Specify moisture protection, edge protection, and coil support.
- Inspection documentation: Request a material test certificate and actual coating measurement results.
- Finished tube requirements: If ordering tubing, separately specify the applicable tube standard, качество сварки, размеры, and additional testing.
9. Теда Ганхуа: Aluminum-Coated Steel Tube Supply and Processing Support
For industrial buyers, selecting the correct coating specification is only one part of the procurement process. Consistent dimensions, substrate quality, coating inspection, and manufacturing coordination are equally important when sourcing materials for exhaust systems, отопительное оборудование, industrial components, and other demanding applications.
Теда Ганхуа is a China-based metal processing and export enterprise with export experience dating back to 2006. The company provides metal product sourcing and processing support for international procurement managers, distributors, and industrial manufacturers.
When evaluating aluminum-coated steel tube requirements, the Teda Ganghua team can assist with technical specification confirmation, включая:
- Outside diameter, толщина стены, and tube length requirements.
- Substrate grade and applicable material standards.
- Aluminum coating type and coating mass requirements.
- Manufacturing and processing requirements for different applications.
- Material inspection and supporting quality documentation.
- Customized supply requirements based on drawings and technical specifications.
For buyers who need materials for high-temperature equipment, выхлопные системы, or general industrial applications, confirming the coating type and finished-product requirements before production helps reduce specification misunderstandings and quality risks.
Contact Teda Ganghua with your required dimensions, сорт материала, обозначение покрытия, количество, and application details to discuss a suitable supply solution.
10. Часто задаваемые вопросы
Q1. Is ASTM A463 a standard for aluminum-coated steel tubes?
Нет. It covers aluminum-coated steel sheet supplied in coils and cut lengths. Finished electric-resistance-welded metallic-coated mechanical tubing is covered by a separate product specification. Buyers should identify both the original strip requirements and the finished tube requirements when applicable.
Q2. What does T1-40 mean in aluminum-coated steel?
T1-40 identifies a Type 1 aluminum-silicon coating with a nominal designation of 0.40 oz/ft² on a combined-both-sides basis. This is approximately 122 г/м². It is a coating mass designation, not a thickness measurement of 0.40 мм.
Q3. What is the difference between Type 1 и тип 2 aluminum coatings?
Тип 1 uses an aluminum-silicon alloy coating, в то время как Тип 2 uses commercially pure aluminum. Тип 1 generally offers better high-temperature coating stability because silicon helps control iron-aluminum intermetallic growth. Тип 2 is commonly considered for applications where corrosion protection at lower operating temperatures is the main requirement.
Q4. Is T1-40 equivalent to EN 10346 АС120?
They have similar nominal combined coating masses, approximately 122 g/m² and 120 г/м², respectively. Однако, their coating chemistry, substrate classifications, and inspection requirements are not automatically identical. Full technical equivalence requires a specification-by-specification comparison.
Q5. What information should buyers provide when ordering aluminum-coated steel tubing?
Покупатели должны предоставить применимый стандарт труб., внешний диаметр, толщина стены, длина, сорт субстрата, тип покрытия, coating mass, требования к сварке, состояние поверхности, требования к инспекции, и предполагаемое применение. Эти детали помогают производителям установить четкие критерии производства и приемки..