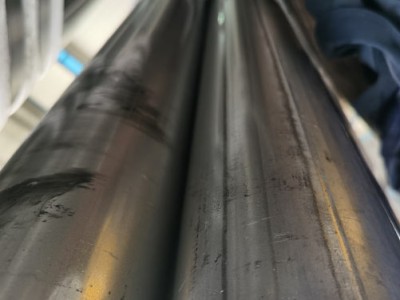
Bending and Forming Aluminized Steel Pipe Without Coating Damage
Bending and Forming Aluminized Steel Pipe: Best Practices to Avoid Coating Damage
Aluminized steel pipe forming requires precise control of bending force, tooling design, and processing conditions to protect the aluminum coating. During pipe bending, excessive deformation, sharp bending angles, or improper equipment settings may cause coating cracks, peeling, and reduced corrosion resistance.
This guide explains the key techniques for bending and forming aluminized steel pipe, including material preparation, bending radius selection, tooling requirements, and quality inspection methods to maintain coating integrity during manufacturing.
Why Coating Damage Happens During Pipe Bending
The aluminum-silicon coating on aluminized steel provides excellent oxidation resistance and high-temperature protection. However, the coating and steel substrate have different mechanical behaviors during deformation.
When the pipe is bent, the outer surface experiences tensile stress while the inner surface experiences compression. If the deformation exceeds the coating’s flexibility limit, micro-cracks may appear and gradually develop into coating separation.
Important Consideration: Successful forming requires balancing bending force and material flexibility. The goal is to achieve the required shape while keeping the protective aluminum layer continuous.
Main Factors Affecting Coating Performance During Forming
| Factor | Possible Problem | Recommended Control |
|---|---|---|
| Bending Radius | Coating cracking on outer surface | Use suitable radius according to pipe diameter and thickness |
| Tooling Condition | Surface scratches or coating damage | Use smooth and properly maintained tooling |
| Forming Speed | Uneven deformation | Maintain stable processing speed |
| Material Condition | Unexpected cracking | Confirm material properties before processing |
Selecting the Correct Bending Method
Different forming methods create different stress levels on the aluminum coating. Choosing the correct process helps reduce surface defects and improves product reliability.
Rotary Draw Bending
Rotary draw bending is widely used for precision pipe forming because it provides accurate control of bending radius and shape. It is suitable for applications requiring smooth curves and consistent dimensions.
- Provides excellent dimensional accuracy.
- Reduces deformation during controlled bending.
- Suitable for complex pipe shapes.
Roll Bending
Roll bending gradually forms the pipe through multiple passes. This method reduces concentrated stress and is suitable for larger diameter components.
Press Bending
Press bending is commonly used for simpler shapes. However, excessive pressure should be avoided because concentrated force may damage the coating surface.
How to Prevent Aluminum Coating Cracking
Maintaining coating performance during forming requires proper process control from material handling to final inspection.
- Select a suitable bending radius to reduce tensile stress.
- Avoid sharp tooling edges that scratch the coating.
- Control forming speed to prevent sudden deformation.
- Keep the pipe surface clean during processing.
- Inspect bent areas for cracks, peeling, or surface defects.
Bending Radius and Material Performance
The minimum bending radius depends on pipe diameter, wall thickness, coating condition, and application requirements. A larger radius generally reduces stress concentration and helps maintain coating continuity.
| Processing Parameter | Effect on Coating | Best Practice |
|---|---|---|
| Small Bending Radius | Higher risk of surface cracking | Use only when material flexibility allows |
| Large Bending Radius | Lower stress concentration | Preferred for coating protection |
| High Forming Speed | Increased deformation risk | Use stable and controlled speed |


Inspection After Pipe Forming
After bending, quality inspection is essential to confirm that the protective coating remains effective. Visual inspection and dimensional checks can identify problems before the pipe enters final assembly.
- Check for visible cracks and coating peeling.
- Measure bending accuracy and pipe roundness.
- Inspect surface scratches caused by tooling.
- Confirm that the formed pipe meets application requirements.
Industrial Supply Capability: Teda Ganghua provides aluminized steel tubes with reliable coating quality and customized processing support for automotive exhaust systems, heating equipment, and industrial applications. Our products can be supplied in different specifications to meet forming and fabrication requirements through our aluminized steel tubes solutions.
Common Mistakes During Forming
- Using unsuitable bending tools that scratch the surface.
- Applying excessive force in a single forming step.
- Ignoring material thickness and bending limitations.
- Failing to inspect coating condition after processing.
FAQ About Bending and Forming Aluminized Steel Pipe
1. Can aluminized steel pipe be bent without damaging the coating?
Yes. With suitable bending equipment, proper radius selection, and controlled forming parameters, coating damage can be minimized.
2. What causes coating cracks during pipe bending?
The main causes include excessive deformation, sharp bending radius, poor tooling condition, and improper forming speed.
3. Is heating required when forming aluminized steel pipe?
Most applications use cold forming methods. Heating requirements depend on pipe size, thickness, and the complexity of the shape.
4. How can manufacturers maintain coating protection after forming?
Using suitable forming methods, controlling stress, and performing surface inspection after bending help maintain coating performance.