Proceso de aluminización por inmersión en caliente: Cómo se fabrican los tubos de acero aluminizado
La aluminización por inmersión en caliente es una de las tecnologías de recubrimiento más confiables para la fabricación de tubos de acero aluminizados de alto rendimiento.. By immersing prepared steel into molten aluminum-silicon alloy, the process creates a metallurgically bonded coating that combines the strength of carbon steel with outstanding heat resistance, resistencia a la oxidación, y protección contra la corrosión.
Unlike paint or electroplated coatings that adhere mechanically, hot-dip aluminizing forms an intermetallic diffusion layer between the steel substrate and the aluminum coating. This metallurgical bond is the reason aluminized steel tubes are widely used in automotive exhaust systems, hornos industriales, intercambiadores de calor, conductos de climatización, and high-temperature ventilation equipment.
Why Hot-Dip Aluminizing Is Different
The coating is not simply deposited on the steel surface. During immersion, iron and aluminum atoms diffuse into each other, creating several alloy layers with different functions.
| Capa | Main Function |
|---|---|
| Outer Aluminum Layer | Provides corrosion resistance and heat reflection |
| Al-Si Alloy Layer | Improves coating stability and crack resistance |
| Fe-Al Diffusion Layer | Creates strong metallurgical bonding |
| Steel Substrate | Provides mechanical strength and toughness |
Complete Hot-Dip Aluminizing Process Flow
The manufacturing process consists of several tightly controlled stages. Each step directly affects coating adhesion, thickness uniformity, and final service life.
| Paso | Main Equipment | Objetivo |
|---|---|---|
| 1. Steel Strip Preparation | Coil Uncoiler | Prepare raw steel strip |
| 2. Desengrasar & Limpieza | Cleaning Line | Remove rolling oil and contaminants |
| 3. Encurtido | Acid Tank | Remove oxide scale and rust |
| 4. Fluxing | Flux Bath | Prevent oxidation before coating |
| 5. El secado & Preheating | Drying Furnace | Improve coating adhesion |
| 6. Aluminización en caliente | Molten Al-Si Bath | Form aluminum coating |
| 7. Control de cuchilla de aire | Air Knife System | Control coating thickness |
| 8. Enfriamiento | Cooling Section | Stabilize coating structure |
| 9. Tube Forming & Soldadura | Tube Mill | Convert strip into steel pipe |
| 10. Final Inspection | Inspection Line | Verify quality before shipment |
Paso 1 – Steel Strip Preparation
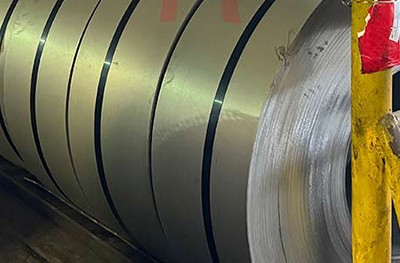
Production begins with high-quality carbon steel coils. Uniform thickness, flatness, and chemical composition are essential because the coating quality depends heavily on the substrate.
Common substrate grades include:
- ASTM A53
- ASTM A36
- ASTM A106
- Q235
- DIN St37


Paso 2 – Degreasing and Surface Cleaning
Rolling lubricants, grasa, polvo, and other contaminants are removed using alkaline cleaning systems. Any remaining contamination can cause coating defects such as pinholes or poor adhesion.
Paso 3 – Acid Pickling
The cleaned steel strip passes through controlled acid pickling tanks to remove mill scale and oxidation.
A clean metallic surface is necessary for proper metallurgical bonding during aluminizing.
Paso 4 – Fluxing
After pickling, the strip enters a flux bath that protects the steel surface from oxidation before immersion into molten aluminum.
Flux treatment improves wetting characteristics and helps produce a continuous coating.
Paso 5 – Drying and Preheating
The steel strip is dried and preheated before entering the aluminizing bath.
Typical objectives include:
- Eliminar la humedad
- Reduce thermal shock
- Improve coating consistency
Paso 6 – Immersion in the Molten Aluminum-Silicon Bath
This is the core stage of the process.
The steel strip is immersed into molten aluminum containing approximately 90% aluminum and 8–11% silicon.
| Typical Process Parameter | Valor típico |
|---|---|
| Temperatura del baño | 680–720°C |
| Contenido de aluminio | Aproximadamente 90% |
| Contenido de silicio | 8–11% |
| Coating Method | Continuous Hot-Dip Process |
Silicon plays an important role by controlling the growth of brittle iron-aluminum intermetallic compounds. Sin silicona, excessively thick alloy layers may become brittle.
Paso 7 – Air Knife Thickness Control
Immediately after leaving the molten bath, high-pressure air knives remove excess molten aluminum.
This operation controls:
- Coating thickness
- Surface smoothness
- Weight consistency
- Appearance quality
Paso 8 – Controlled Cooling
The coated strip is cooled under carefully controlled conditions to stabilize the coating microstructure.
Proper cooling minimizes thermal stress while maintaining coating adhesion.
Paso 9 – Tube Forming and Welding
Después del recubrimiento, the aluminized strip enters a tube mill where it is progressively formed into round tubing.
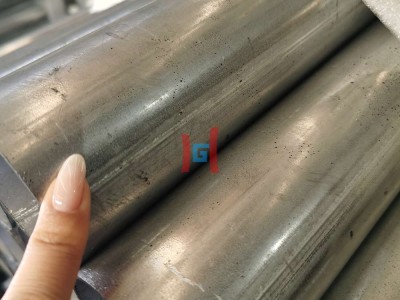
High-frequency welding joins the strip edges to produce continuous pipe suitable for industrial applications.
Paso 10 – Inspection and Quality Control
Every production batch is inspected before shipment.
Typical quality inspections include:
- Medición del espesor del recubrimiento
- Surface appearance inspection
- Bending test
- Adhesion evaluation
- Dimension verification
- Weld quality inspection
Critical Manufacturing Equipment Throughout the Process
| Equipo | Primary Function |
|---|---|
| Cleaning Line | Surface preparation |
| Pickling Tank | Oxide removal |
| Flux Station | Surface activation |
| Preheating Furnace | Temperature stabilization |
| Al-Si Bath | Coating formation |
| Air Knife System | Thickness control |
| Cooling Section | Microstructure stabilization |
| Tube Forming Mill | Pipe production |
Advantages of the Hot-Dip Aluminizing Process
- Excellent coating adhesion through metallurgical bonding.
- High heat resistance for temperatures approaching 700–800°C (Tipo 1 revestimientos).
- Outstanding oxidation resistance.
- Improved corrosion resistance compared with uncoated carbon steel.
- Excellent heat reflectivity for thermal management applications.
- Long service life in demanding industrial environments.
Typical Applications of Hot-Dip Aluminized Steel Pipes
- Sistemas de escape para automóviles
- Tubos para hornos industriales
- Intercambiadores de calor
- Boiler components
- Sistemas de conductos HVAC
- Equipos de secado agrícola
- Industrial ventilation pipelines
Teda Ganghua Hot-Dip Aluminized Steel Tube Solutions
Teda Ganghua supplies aluminized steel tubes manufactured for demanding industrial environments where heat resistance, protección contra la corrosión, and long service life are required. With professional processing capabilities, customized dimensions, corte de precisión, and strict quality inspection, Teda Ganghua supports customers across automotive, calefacción industrial, climatización, agricultural equipment, and heavy manufacturing industries.
Whether the application requires standard aluminized tubing or customized processing services, Teda Ganghua helps customers select suitable coating types, substrate grades, and dimensions for long-term operational performance.
Learn more about our
tubos de acero aluminizado
solutions.
Preguntas frecuentes
Why is silicon added to the aluminum bath?
Silicon controls the growth of brittle iron-aluminum intermetallic compounds, producing a stronger and more stable coating.
What is the typical temperature of the hot-dip aluminizing bath?
Industrial hot-dip aluminizing baths typically operate between 680°C and 720°C depending on the production process.
How is coating thickness controlled?
Air knife systems precisely remove excess molten aluminum immediately after immersion, producing a uniform coating thickness.
What industries use hot-dip aluminized steel pipes?
Major industries include automotive manufacturing, hornos industriales, intercambiadores de calor, sistemas de climatización, and high-temperature processing equipment.
Why is hot-dip aluminizing preferred over ordinary coatings?
Because the coating forms a metallurgical bond with the steel substrate, it offers significantly better adhesion, resistencia al calor, and long-term durability than mechanically bonded coatings.