
タイプ 1 対タイプ 2 アルミメッキ鋼コーティングの違い
タイプ 1 とタイプ 2 aluminized steel coatings are designed for different service environments, even though both use aluminum to protect a steel substrate. The fundamental difference lies in the addition of silicon to the aluminum coating and how this alloying element influences the formation of the iron-aluminum intermetallic layer during hot-dip coating. タイプ 1 uses an aluminum-silicon alloy to improve performance under elevated temperatures, 入力しながら 2 uses commercially pure aluminum to prioritize atmospheric corrosion protection. Understanding these metallurgical differences helps engineers and procurement managers select the appropriate coating for exhaust systems, 暖房器具, building components, および産業用アプリケーション.
1. Understanding the Chemical Difference Between the Two Coating Types
Both coating systems are produced through a hot-dip aluminizing process in which steel passes through a molten aluminum-based bath. During coating, metallurgical reactions occur at the interface between the steel substrate and the aluminum coating, forming an intermediate iron-aluminum alloy layer. しかし, the chemical composition of the coating bath significantly changes the development of this interface.
タイプ 1 コーティング: An aluminum-silicon alloy containing approximately 5–11% silicon by weight. Silicon helps control the growth of the iron-aluminum intermetallic layer and supports applications involving elevated temperatures.
タイプ 2 コーティング: Commercially pure aluminum without the intentional silicon addition used in the first coating system. It generally develops a different interfacial structure and is primarily selected for atmospheric corrosion resistance.
These compositions are recognized in ASTM A463/A463M, which specifies aluminum-coated steel sheet produced by the hot-dip process. The distinction is not simply a matter of adding or removing an alloying element. It changes the coating’s metallurgical structure, forming behavior, and suitability for different operating conditions.
| Comparison Factor | タイプ 1 | タイプ 2 |
|---|---|---|
| Main coating composition | Aluminum-silicon alloy | Commercially pure aluminum |
| シリコン含有量 | Approximately 5–11 wt.% | 意図的なシリコン添加なし |
| 金属間化合物層 | Growth is controlled by silicon addition | Generally develops a thicker alloyed interface |
| Primary performance priority | 高温耐酸化性 | 耐大気腐食性 |
| 代表的な用途 | 排気システム, 炉, 暖房器具 | Building panels, 屋根ふき, ventilation components |
| Forming characteristics | Generally better coating ductility | Thicker brittle intermetallic layer requires forming control |
2. Why Silicon Improves the High-Temperature Performance of Aluminum Coatings
The key metallurgical function of silicon is to regulate the reaction between molten aluminum and the steel substrate. During hot-dip aluminizing, iron from the steel reacts with aluminum to form intermetallic compounds. If this reaction proceeds excessively, the alloyed layer can become thick and brittle, increasing the risk of coating damage during subsequent forming and thermal exposure.
2.1 Controlling the Growth of Iron-Aluminum Intermetallic Compounds
In an aluminum-silicon coating bath, silicon influences the formation and growth of iron-aluminum intermetallic phases. It helps suppress excessive interfacial alloy-layer development during the coating process, producing a coating structure with a more favorable balance between the aluminum-rich outer layer and the underlying alloyed interface.
This distinction is important because an excessively thick intermetallic layer can reduce coating ductility. Under bending, スタンピング, or thermal cycling, brittle interfacial regions may develop cracks. By controlling the reaction during coating formation, silicon helps maintain more suitable coating characteristics for components that undergo fabrication before entering high-temperature service.
2.2 Maintaining an Effective Aluminum-Rich Protective Surface
Aluminum provides the principal oxidation protection in both coating systems. When exposed to oxygen at elevated temperatures, aluminum forms a stable aluminum oxide (アル2O3) surface film. This oxide layer acts as a barrier that slows further oxidation of the underlying coating and steel substrate.
The effectiveness of this protection depends on maintaining sufficient coating integrity. Excessive intermetallic growth, surface cracking, repeated thermal expansion, and coating depletion can gradually reduce the protective capability. The silicon-modified coating structure helps support the performance required in components exposed to repeated heating and cooling.
Important technical distinction: Silicon does not simply increase the melting point of aluminum or independently create heat resistance. Its primary role is to influence interfacial reactions and coating microstructure. High-temperature oxidation protection ultimately depends on the aluminum-rich surface, oxide-film stability, coating thickness, and actual operating conditions.
3. Why Pure Aluminum Coatings Offer Different Corrosion Protection
The second coating system follows a different metallurgical approach. Without the intentional silicon addition, the reaction between aluminum and iron during hot-dip coating is less restricted. This generally produces a thicker iron-aluminum intermetallic layer beneath the outer aluminum-rich coating.
3.1 A Different Interfacial Structure
The thicker alloyed interface is one of the important structural characteristics of pure aluminum-coated steel. Depending on the manufacturing process and coating conditions, different iron-aluminum intermetallic phases can develop. These phases are generally harder and more brittle than the aluminum-rich outer layer.
Although this structure can create challenges during severe forming operations, it is associated with the corrosion-oriented characteristics of this coating system. The outer aluminum layer provides a protective barrier, while the overall coating mass and interfacial structure contribute to long-term atmospheric exposure performance.
3.2 Aluminum Oxide and Atmospheric Corrosion Resistance
When aluminum is exposed to air, a thin oxide film forms naturally on its surface. This passive film limits further interaction between the metal and the surrounding environment. In atmospheric conditions, aluminum also provides barrier protection by separating the underlying steel from moisture and corrosive substances.
Pure aluminum-coated steel is therefore widely considered for building envelopes, 屋根ふき, 換気システム, and other components where exposure to rain, 湿度, and outdoor atmospheric conditions is more important than sustained high-temperature oxidation resistance.
しかし, corrosion performance cannot be determined by coating chemistry alone. 塗布量, 表面状態, cut edges, forming damage, drainage design, chloride exposure, and maintenance requirements all influence actual service life.
4. Comparing the Heat Resistance Mechanisms
The most important difference between the two coatings is how their metallurgical structures support performance under thermal exposure. Both contain aluminum, but they are not equally suitable for continuous heating, 熱サイクル, or oxidation-intensive environments.
タイプ 1: Designed Around Thermal Oxidation Protection
During high-temperature exposure, the aluminum-rich surface develops an oxide layer that reduces the rate of further oxidation. Silicon controls the development of the iron-aluminum interface during manufacturing, helping maintain a suitable coating structure for heat-exposed components.
Typical focus: Exhaust components, 熱シールド, 暖房器具, and industrial furnace parts.
タイプ 2: Designed Around Atmospheric Protection
The commercially pure aluminum coating provides a protective outer barrier against moisture and atmospheric corrosion. Its coating structure and commonly used coating weights make it suitable for applications where long-term environmental exposure is the primary consideration.
Typical focus: 屋根材, exterior panels, 換気ダクト, and building components.
It is important not to assign a universal maximum operating temperature to either coating based only on its type. Actual temperature capability depends on exposure duration, oxygen availability, coating mass, thermal cycling frequency, base steel composition, and mechanical loading. A component exposed to short-term heating may perform differently from one subjected to continuous operation at the same temperature.
5. Microstructure, Thermal Cycling, and Coating Failure
Thermal cycling introduces additional challenges because the aluminum coating, intermetallic interface, and steel substrate do not expand and contract at exactly the same rate. Repeated temperature changes generate stresses within the coating system, potentially causing cracks, localized separation, or progressive oxidation.
5.1 The Effect of Intermetallic Layer Thickness
The iron-aluminum intermetallic layer is necessary for metallurgical bonding, but excessive growth can become detrimental. A thick, brittle layer is less capable of accommodating deformation and local stress. During fabrication or thermal cycling, cracks may develop and provide pathways for oxygen to reach underlying regions.
The silicon addition in the first coating system helps limit excessive intermetallic growth during hot-dip processing. This is particularly relevant when the coated steel must be formed into exhaust pipes, thermal shields, or other components before installation.
5.2 Oxide Scale Stability During Repeated Heating
Aluminum oxide is responsible for much of the oxidation resistance of aluminized steel. Nevertheless, oxide protection is not permanent under all conditions. Repeated thermal shocks, mechanical abrasion, aggressive atmospheres, and coating depletion can weaken the protective surface.
For industrial equipment, engineers should evaluate the actual heating cycle rather than relying exclusively on a nominal temperature value. Continuous temperature, peak temperature, heating rate, cooling rate, and the presence of sulfur-containing or other aggressive gases should all be considered.
6. Typical Applications and Material Selection
Selecting the appropriate coating begins with identifying the dominant service condition. A component exposed to exhaust gases and repeated heating requires a different coating strategy from an exterior building panel exposed primarily to rain and humidity.
| 応用 | Main Service Condition | Preferred Coating | Selection Reason |
|---|---|---|---|
| 自動車の排気システム | Elevated temperature and oxidation | タイプ 1 | Designed for heat-exposed service |
| Industrial heating equipment | Repeated heating and cooling | タイプ 1 | Aluminum-based oxidation protection |
| 炉のコンポーネント | Thermal oxidation | タイプ 1 | Better alignment with heat-resistant applications |
| Roofing and cladding | Rain, 湿度, and atmospheric exposure | タイプ 2 | Corrosion-oriented coating design |
| 換気システム | Atmospheric corrosion and moderate temperatures | タイプ 2 | Suitable for environmental protection requirements |
| Outdoor building components | Long-term weather exposure | タイプ 2 | 耐大気腐食性 |
These recommendations describe typical applications rather than absolute restrictions. Some components experience both high temperatures and corrosive environments. そのような場合には, engineers must evaluate the dominant degradation mechanism and verify the coating against the actual operating conditions.
7. What Procurement Managers Should Check Before Ordering
For industrial buyers, specifying the coating type is only the first step. The purchase specification should also define the substrate, coating designation, 寸法公差, 表面要件, fabrication conditions, and inspection documentation.
Essential Technical Checks
1. Coating designation: Clearly identify the required coating type according to the applicable ASTM A463/A463M specification. Avoid using generic descriptions such as aluminum-coated steel without further clarification.
2. 塗布量: Specify the required coating weight and clarify whether the stated value represents the total coating mass on both sides or another measurement basis.
3. スチール基板: Confirm the base steel grade, 厚さ, mechanical properties, and applicable product requirements.
4. Operating temperature: Provide continuous and peak temperatures, 露出時間, and thermal cycling conditions.
5. Fabrication requirements: Identify bending radii, stamping depth, welding methods, and post-coating processing requirements.
6. Quality documentation: Request material test certificates, coating inspection records, dimensional inspection results, and relevant product conformity documents.
For tubular applications, additional requirements should include outside diameter, 壁の厚さ, 長さ, 寸法公差, weld seam quality, and the condition of the coating after tube forming and welding. Buyers should also clarify whether the coating is applied before or after tube fabrication because these manufacturing routes can produce different coating conditions at the weld seam and formed areas.
8. Aluminized Steel Tube Supply and Processing Support from Teda Ganghua
For manufacturers working with exhaust systems, 工業用加熱装置, ventilation assemblies, and other metal fabrication projects, selecting the correct coating must be coordinated with dimensional requirements and downstream processing.
Teda Ganghua provides metal material sourcing and processing support for international industrial buyers. With export experience dating back to 2006, the company supports procurement inquiries involving coated steel materials and customized metal products. Its technical coordination focuses on matching material specifications with application requirements, including substrate selection, 寸法, coating characteristics, and inspection documentation.
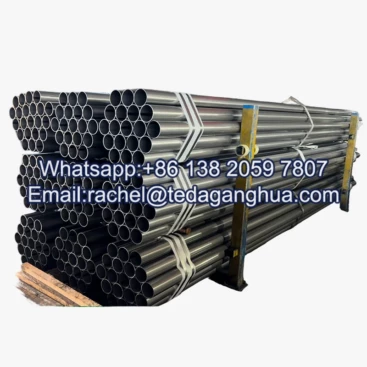
For projects requiring アルミメッキ鋼管, procurement managers can communicate their required outside diameter, 壁の厚さ, チューブの長さ, coating type, 動作温度, and fabrication conditions. These details help establish whether the selected material is suitable for the intended service environment.
Teda Ganghua also supports specification confirmation and material inspection coordination to help buyers reduce discrepancies between purchase requirements and delivered products. For demanding industrial applications, confirming the coating standard and manufacturing route before production is particularly important.
Submit Your Technical Requirements
When requesting a material quotation or technical confirmation, prepare the following information:
- Required coating type and applicable standard
- Steel grade and substrate thickness
- Tube outside diameter and wall thickness, if applicable
- Coating mass and surface requirements
- Continuous and maximum operating temperatures
- Required certificates and inspection standards
Providing these details enables a more accurate material assessment and helps establish a reliable supply specification for your project.
9. よくある質問
Q1. What is the main difference between Type 1 とタイプ 2 アルミメッキ鋼?
The primary difference is coating composition and intended performance. タイプ 1 contains approximately 5–11% silicon in an aluminum-based coating and is mainly designed for heat-resistant applications. タイプ 2 uses commercially pure aluminum and is primarily intended for atmospheric corrosion protection.
Q2. Why is silicon added to aluminum coatings?
Silicon helps control the growth of iron-aluminum intermetallic compounds during hot-dip coating. By limiting excessive interfacial alloy-layer development, it helps maintain a more suitable coating structure and improves fabrication characteristics for heat-exposed components.
Q3. Does Type 2 have better corrosion resistance than Type 1?
タイプ 2 is generally selected when atmospheric corrosion resistance is the primary requirement. Its pure aluminum coating and commonly used coating mass provide advantages in many outdoor environments. Actual corrosion performance still depends on coating thickness, exposure conditions, surface damage, and maintenance.
Q4. Can Type 2 aluminized steel be used in high-temperature applications?
It may tolerate certain moderate or intermittent temperature exposures, depending on the material specification and operating conditions. しかし, it is not the primary coating choice for sustained high-temperature oxidation service. エンジニアは材料を承認する前に完全な熱プロファイルを評価する必要があります.
Q5. アルミニウム被覆鋼板を対象とする ASTM 規格はどれですか?
ASTM A463/A463M は、溶融めっきプロセスを通じてアルミニウムでコーティングされた鋼板を対象としており、さまざまなコーティングの種類とコーティング質量の要件を特定しています。. 購入者は該当するエディションを指定する必要があります, coating type, 指定, 購入書類に記載されている基材要件.


